Home

Blog

  • PACM Epoxy Curing Agent: Light Colour at 50-80 mPa·s
    PACM Epoxy Curing Agent: Light Colour at 50-80 mPa·s
    Oct 23, 2026
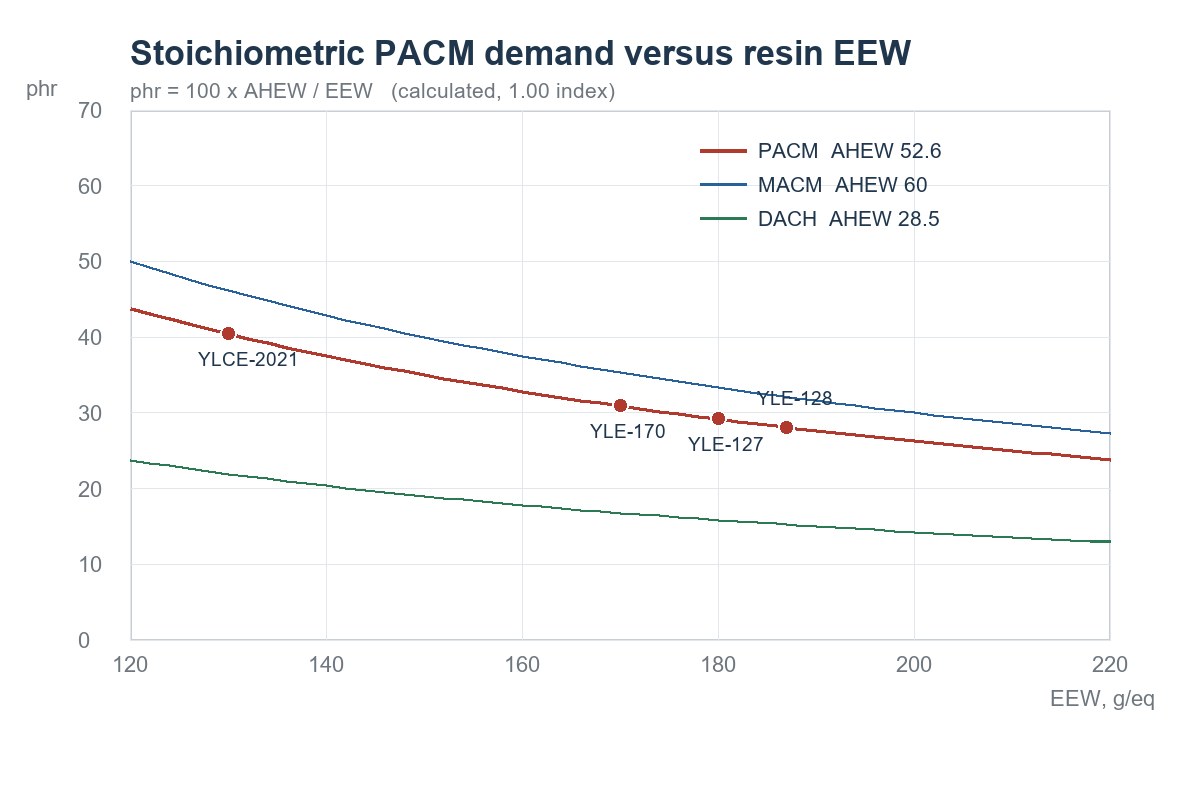
    PACM epoxy curing agent is a colourless alicyclic diamine, 4,4'-diaminodicyclohexyl methane (CAS 1761-71-3), sold at 50-80 mPa·s and APHA 30 or below. Four amine hydrogens on a 210.36 g/mol molecule give a calculated AHEW of 52.6 g/eq, which puts YLE-128 at 28.1 phr. Specification and dosage follow. Figure 1. Calculated demand for PACM (52.6 g/eq), MACM (60 g/eq) and DACH (28.5 g/eq) across 120-220 g/eq; marked points are the grades in Table 4. 1. Introduction: Why the Unsubstituted Ring Matters Alicyclic diamine hardeners suit coatings that must stay hard and stay light in colour but cannot take the short pot life of diethylenetriamine. PACM is the unsubstituted member of that family: two cyclohexane rings joined by a methylene bridge, each carrying one primary amine. Its published specification is five lines and one CAS number, with viscosity at 50-80 mPa·s at 25 °C. Melting point, flash point and density are not on the page, so they are left out here rather than filled from memory. Three sources feed the numbers: the PACM product page, three comparable alicyclic diamines from the same catalogue, and stoichiometry. 2. Materials and Methods: PACM Epoxy Curing Agent Specification One CAS number and four lines pin the identity down. 2.1 Product Identification and Published Limits Table 1 lists the identifiers that belong on a purchase order and on the COA review sheet. Table 1. Product identification of PACM; values marked calculated come from molecular structure, not from the product page. Item Information Trade designation PACM Chemical name 4,4'-Diaminodicyclohexyl methane CAS No. 1761-71-3 Molecular formula (calculated) C13H26N2 Molecular weight (calculated) 210.36 g/mol Amine hydrogen equivalent weight (calculated) 52.6 g/eq from four active hydrogens Appearance Colourless or slightly yellow transparent liquid, packed in drums Table 2 repeats the five published limits beside the test basis a laboratory would normally apply to each. Table 2. Published specification of PACM with the corresponding test method. Item Published limit Test basis Appearance Colourless liquid, no suspended matter visual, per current TDS Colour APHA 30 maximum ASTM D1544 Viscosity at 25 °C 50-80 mPa·s ASTM D445 Purity 99.0% minimum supplier method Water 0.20% maximum ASTM E203 2.2 Test Methods and Data Sources Resin epoxy equivalent weight is determined by titration according to ASTM D1652, with ISO 3001 as the alternative route. Colour is read according to ASTM D1544 against the Gardner scale, viscosity according to ASTM D445 at 25 °C. Water moves first after a drum is opened, so it is measured by Karl Fischer titration according to ASTM E203 on duplicate portions, reported as the mean of n = 3. Amine hydrogen equivalent weight is not printed on the product page. It follows from molecular weight divided by active hydrogens: 210.36 ÷ 4 = 52.59 g/eq. That arithmetic reproduces two published values on the same catalogue, 60 g/eq for MACM and 28.5 g/eq for DACH, to within 1%, which is why 52.6 g/eq is used in every dosage table here. 3. Results and Discussion: Ring Geometry and Cure Response Ring geometry, not molecular weight, separates PACM from the linear aliphatic amines. 3.1 Why the Cyclohexane Ring Changes Hardness and Colour Both amines sit on a cyclohexane ring, making them primary amines on secondary carbons. Steric hindrance there slows the addition to an epoxide, so a PACM mix stays workable longer than a DETA mix of the same equivalent weight. Crosslink density moves the other way. At 52.6 g/eq with four hydrogens, PACM creates more network junctions per 100 g of resin than a 60 g/eq hardener, and the rigid ring lifts hardness and heat deflection without aromatic structure. Colour holds because no aromatic chromophore is present to yellow under UV, although the surface stays a primary amine that reacts with carbon dioxide. 3.2 Comparison with Alternative Diamine Hardeners Table 3 sets the PACM epoxy curing agent beside three alicyclic diamines from the same catalogue, on the lines that decide a formulation. Table 3. Published properties of four alicyclic diamine hardeners; calculated AHEW values follow the method in section 2.2. Property PACM MACM DACH 1,3-BAC CAS No. 1761-71-3 6864-37-5 694-83-7 2579-20-6 Ring substitution none two methyl none aminomethyl arms Colour, APHA 30 max 30 max 30 max not published Viscosity, 25 °C 50-80 mPa·s 80-120 mPa·s not published not published Water 0.20% max not published 0.3% max 0.3% max AHEW 52.6 g/eq 60 g/eq 28.5 g/eq 35.6 g/eq Dosage tracks the equivalent weight almost linearly. On a 187 g/eq bisphenol A resin, DACH needs 15.2 phr, 1,3-BAC 19.0 phr, PACM 28.1 phr and MACM 32.1 phr at the same stoichiometry. Viscosity is where the grade earns its place: 50-80 mPa·s carries more filler and less solvent than MACM at 80-120 mPa·s, which decides whether a high-solids primer stays under a VOC ceiling. Speed is the trade-off: DACH reacts fast at 28.5 g/eq and suits thin films in a cold shop, but rules itself out of a 3 mm casting. 4. Formulation and Dosage Calculation Dosage comes from one equation: phr = 100 × AHEW ÷ EEW, with 52.6 g/eq for PACM and the EEW of the resin actually in the pot. Table 4 applies it to four resins at full and 0.90 stoichiometry. Table 4. Calculated PACM demand in phr for four Yolatech resins, at 1.00 and 0.90 stoichiometric index. Resin EEW, g/eq Dosage at 1.00 index, phr Dosage at 0.90 index, phr YLCE-2021 125-135 39.0-42.1 35.1-37.9 YLE-170 160-180 29.2-32.9 26.3-29.6 YLE-127 176-184 28.6-29.9 25.7-26.9 YLE-128 184-190 27.7-28.6 24.9-25.7 A 0.90 index leaves about a tenth of the epoxide unreacted. In practice most ambient-cure coatings run there, because a slight amine excess tolerates surface moisture and carbon dioxide better than an exact ratio. Below 0.85 the film stays soft and chemical resistance drops; above 1.05 the surplus amine plasticises the network and pushes colour up. Neither end recovers with longer curing, so verify the index before scaling up. The same equivalent weight serves polyurethane work: against an isocyanate equivalent of 42.02 g/eq, 100 g of NCO groups consume 125.2 g of PACM. 5. Processing Notes and Operating Window Four settings decide whether a PACM system behaves in the plant the way it did in the laboratory. Mix by weight, never by volume. Density differences between a filled resin and an amine shift volume ratios by several percent. Keep the shop between 18 and 30 °C. Below 10 °C the addition reaction slows sharply and a 24-hour cure stretches to three days; if the plant runs colder, extend induction and accept overnight tack. Hold relative humidity under 70%. Beyond that, carbamate forms faster than the film cures and the haze is permanent. Post-cure at 80 °C for 2 hours where heat deflection matters; no Tg is published, so confirm on your own laminate. Figure 2. Temperature bands for a PACM-cured ambient system; the 18-30 °C band holds both the published viscosity and a 24-hour cure. Batch size is the practical control on exotherm. Five kilograms in a thin tray is safe at 25 °C; the same five kilograms in a 20 cm drum will gel in the pot. 6. Applications Five roles appear on the product page. Typically coatings is trialled first. Table 5. Application roles of PACM and the property that carries each one. Segment Function of PACM Typical level What decides success Protective coatings curing agent 27-29 phr blush resistance, hardness Adhesives curing agent 28-31 phr colour, bond-line rigidity Composites curing agent 28-41 phr wet-out viscosity, pot life Saturated polyurethane chain extender 125 g per 100 g NCO urea segment regularity Polyamide hardeners amine intermediate set by the adduct amine value of the adduct Figure 3. The five roles listed on the product page, with the property that governs each. Filament winding is the composite case worth checking first, because 50-80 mPa·s wets out roving without solvent yet stays in the bath. For polyamide intermediates the grade is a building block, not a hardener, so the amine value of the finished adduct sets the dosage. 7. Limitations and Material Verification Three limits appear in the first month of use, and none is solved by adding more hardener. 7.1 Known Limitations and Unsuitable Cases No ring methyl groups means the unmethylated alicyclic diamines are the ones that thicken or crystallise in an unheated store. The page publishes no melting point, so the pour point has to come from the COA of the lot before a winter shipment. Cold curing is not its strength. At 10 °C a film still cures, but the surface stays tacky far longer than a DACH or DETA film, and dust becomes the limiting factor. Sections above roughly 50 mm need a slower hardener or a staged ramp; this one alone will crack from exotherm. Food contact, potable water and medical use fall outside the published data, with no migration testing listed. 7.2 Incoming Inspection, Packaging, Storage and Safety A receiving check needs four numbers: APHA colour, viscosity at 25 °C, water by Karl Fischer and purity by the supplier method. Anything outside Table 2 goes back before the drum reaches production. Purity at 99.0% leaves up to 1% of other amines and water, enough to shift colour and pot life between lots. Material ships in drums and keeps at least 12 months from manufacture in the original packing at ambient. Keep the cap closed, away from flame and sunlight, and blanket part-used drums with dry nitrogen. Check with the supplier before blending lots of different dates. The liquid is alkaline and attacks copper alloys, so gloves, goggles and local exhaust are the minimum; the MSDS governs. RoHS and REACH declarations are issued per shipment on request, and nothing here certifies the grade. 8. Frequently Asked Questions What is the amine hydrogen equivalent weight of PACM? It is 52.6 g/eq: 210.36 g/mol divided by four active hydrogens. The page does not print it; the result matches the published 60 g/eq of MACM and 28.5 g/eq of DACH. How much PACM does YLE-128 resin need? YLE-128 at 184-190 g/eq takes 27.7-28.6 phr at full stoichiometry, or 24.9-25.7 phr at a 0.90 index. The exact figure depends on the lot EEW, so the COA value belongs in the formula. Is PACM the same as MACM? No. PACM is unsubstituted at CAS 1761-71-3, AHEW 52.6 g/eq and 50-80 mPa·s; MACM carries two ring methyl groups at CAS 6864-37-5, AHEW 60 g/eq and 80-120 mPa·s. They are not interchangeable by weight. Why does a PACM film blush in humid weather? Primary amines react with carbon dioxide and water to form carbamates at the surface. The reaction runs fastest below 15 °C and above 70% relative humidity, and the haze cannot be washed off with solvent. Can PACM serve as a polyurethane chain extender? Yes. It reacts with isocyanate to build a urea segment, and 100 g of NCO groups take 125.2 g of PACM. Reactivity is high, so prepolymer processes suit it better than one-shot systems. What pot life should be expected at 25 °C? No gel time is published, and none can be calculated from AHEW. Run a 100 g cup test at shop temperature; treat any quoted figure, ours included, as a starting point. 9. Conclusions Light colour, 50-80 mPa·s and a calculated AHEW of 52.6 g/eq put dosage at 27.7-28.6 phr on YLE-128. The value sits in hardness and colour retention at high solids, not cure speed, so DACH stays faster and MACM more storage-tolerant. Two numbers decide most formulations: resin EEW and the index between 0.90 and 1.00. Both can be measured before the drum is opened. 10. References 1. Yolatech product page, PACM (CAS 1761-71-3), https://www.yolatech.com/44-diaminodicyclohexyl-methane-pacm-cas-1761-71-3 (accessed 2026-10-23). 2. Yolatech technical data sheet for PACM, specification and pack size (available on request). 3. Yolatech material safety data sheet for PACM, CAS 1761-71-3 (available on request). 4. ASTM D1652, epoxy content of epoxy resins (EEW). 5. ISO 3001, determination of epoxy equivalent. 6. ISO 9702, amine group nitrogen content of amine epoxide hardeners. 7. ASTM D445, kinematic viscosity. 8. ASTM D1544, Gardner color of transparent liquids. 9. ASTM E203, water content by Karl Fischer titration.
    Read More
  • HMDA Epoxy Curing Agent: 1,6-Hexanediamine phr and Purity
    HMDA Epoxy Curing Agent: 1,6-Hexanediamine phr and Purity
    Oct 22, 2026
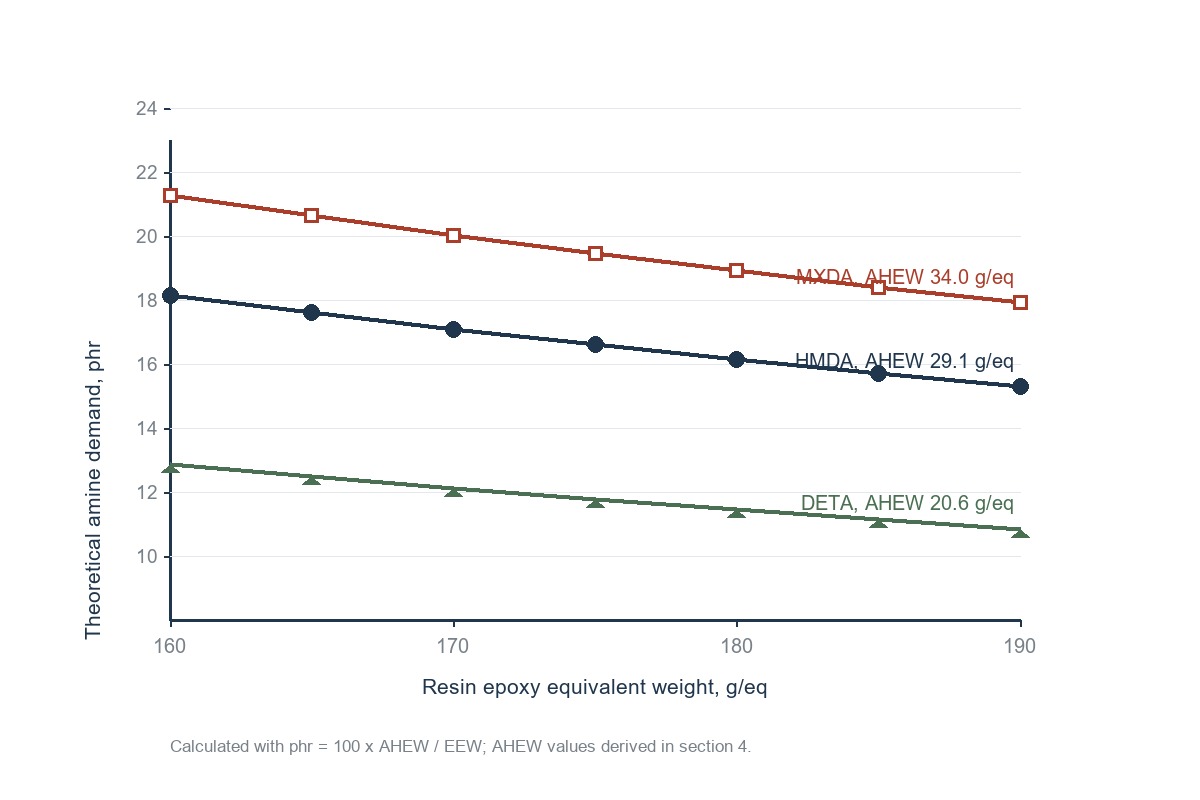
    HMDA epoxy curing agent 1,6-hexanediamine (CAS 124-09-4) is an aliphatic diamine hardener sold at 99.90% minimum purity with water below 0.05%. Its calculated amine hydrogen equivalent weight is 29.1 g/eq, and so the stoichiometric demand lands at 15.5 phr in a bisphenol A epoxy resin of 187.0 g/eq. Figure 1. Calculated stoichiometric demand against resin epoxy equivalent weight for HMDA (29.1 g/eq), MXDA (34.0 g/eq) and DETA (20.6 g/eq); curves follow phr = 100 x AHEW / EEW as derived in section 4. 1. Introduction: Where a Short-Chain Diamine Fits Straight-chain aliphatic diamines sit at the fast, high-crosslink-density end of the amine hardener range. 1,6-Hexanediamine is the shortest member that still keeps a flexible C6 spacer between its two primary amine groups, and four active hydrogens per molecule build a tight network at low loading, which is what high-solids coatings and rigid adhesive formulations ask for. The same shortness creates the two practical problems quantified below. A literature melting point of about 41-42 °C, absent from the product page, means drums can wax in a cool warehouse. The strong ammonia odour, stated openly on the product page, rules out indoor work without forced ventilation. Selection depends on whether the formulation accepts those constraints in exchange for reactivity. 2. Materials and Methods: Published Specification of 1,6-Hexanediamine 2.1 Product Identification and Published Specification The grade is sold under the trade name HMDA, chemical name 1,6-hexanediamine, CAS 124-09-4. Four specification items are published on the product page: appearance, purity, water content and the PRI value. Everything else in this report is calculated from structure or marked as literature data, never presented as a published figure. Table 1. Product identification of HMDA, with calculated and literature descriptors marked as such. Item Information Trade name HMDA Chemical name 1,6-Hexanediamine (hexamethylenediamine) CAS No. 124-09-4 Molecular formula C6H16N2 (literature) Active hydrogens per molecule 4, from two primary amine groups (calculated) Amine hydrogen equivalent weight 29.1 g/eq (calculated, 116.2 / 4) Product page yolatech.com/16-hexanediamine-hmda-cas-124-09-4 Table 2. Published specification items on the product page. Property Published value Appearance Colorless to pale yellow liquid Purity, % Min. 99.90 Water, % Max. 0.05 PRI value, mmol/t Max. 100 The liquid appearance on the specification sheet deserves one comment. A diamine that solidifies at about 41-42 °C stays liquid only in warm storage, so check the drum temperature before assuming the contents are pourable. 2.2 Test Methods and Data Sources Three data classes are kept apart. Published values come from the product page and its certificate documents. Calculated values, such as the 29.1 g/eq equivalent weight, follow from the molecular weight of 116.2 g/mol and four active hydrogens, and any reader can recompute them. Literature values, such as the melting point, are labelled as such and should be confirmed against the TDS and MSDS supplied with each lot. Where a formulation example is needed, the resin baseline is the bisphenol A liquid grade YLE-128 with an epoxy equivalent weight of 184-190 g/eq; all arithmetic is performed at the mid-point of 187 g/eq, and every demand figure in section 4 follows the same division. Purity enters as shipped, since the 99.90% floor leaves at most 0.1% for correction, less than normal plant weighing error. 3. Results and Discussion: HMDA Epoxy Curing Agent Against Alternative Polyamines 3.1 Structure-Reactivity Behaviour Two primary amines on a straight C6 chain give four hydrogens of nearly equal reactivity, so gelation arrives early and the exotherm is front-loaded. No steric shielding and no ether oxygen slow the addition, so this diamine reaches handle strength faster than ether-extended adducts at equal loading. The C6 spacer moderates the brittleness short diamines usually cause. Six carbons between the nitrogen nodes let the network deform before it cracks, a small but real gain over ethylene diamine type structures. The gain is relative: against polyetheramines or adducts the film stays harder and less forgiving. Humidity sensitivity is the weak point. The product page states that the material absorbs water and carbon dioxide from air. Carbamate on exposed amine surfaces shows up as blushing and poor intercoat adhesion, so open time in the mixer matters. 3.2 Selection Comparison Table 3 compares the diamine with the polyamine alternatives stocked on the same site, all AHEW values determined by the same molecular-weight division for a fair basis. The choice depends on which constraint binds first: loading accuracy, odour, blush, or flexibility. Table 3. Selection comparison of HMDA with alternative amine hardeners; equivalent weights and phr values are calculated against YLE-128 at 187 g/eq. Attribute HMDA (this grade) Alternative polyamines AHEW, g/eq (calculated) 29.1 DETA 20.6; MXDA 34.0; DMAPA 44.1; MACM 52.6 Stoichiometric phr in YLE-128 15.5 DETA 11.0; MXDA 18.2; DMAPA 23.6; MACM 28.1 Purity floor, % 99.90 (published) DETA high-purity grade; others per their pages Form at 25 °C Solid below about 41-42 °C (literature); liquid when warm MXDA liquid; MACM low-melt solid Odour Very strong ammonia odour (published) Lower for MACM; MXDA sharper but less volatile Blush tendency High in humid air; absorbs CO2 and water (published) MACM lower; DETA also blush-prone Network character Dense and rigid, C6 spacer adds slight flex MXDA aromatic ring raises Tg; DMAPA tertiary N slows cure Read the table by constraint, not by column. If loading accuracy at high purity binds, the 99.90% floor and the 15.5 phr figure make the diamine easy to dose and audit. If blushing or odour binds, pick a cycloaliphatic hardener and accept the higher phr. 4. Formulation and Dosage Calculation The stoichiometric rule is one line: phr = 100 x AHEW / EEW. With AHEW at 29.1 g/eq and the YLE-128 mid-point of 187 g/eq, demand is 100 x 29.1 / 187 = 15.5 phr. Every figure below follows from that division, with no hidden constant. Table 4. Calculated stoichiometric demand of HMDA across three resin grades, with DETA shown for cross-checking. Resin grade EEW, g/eq HMDA phr (calculated) HMDA kg per 100 kg resin DETA phr (calculated) YLE-127 180 16.1 16.1 11.4 YLE-128 187 15.5 15.5 11.0 YLE-170 (BPF) 170 17.1 17.1 12.1 Two corrections sit on top. First, if the lot certificate reports an EEW of 191 g/eq, demand drops to 15.2 phr, so dose from the certificate rather than the datasheet mid-point. Second, under-dosing shows as a tacky surface at room temperature; half a phr of deviation is already visible, which makes this hardener less tolerant of sloppy weighing than higher-AHEW alternatives. 5. Processing Notes and Operating Window Mixing behaviour is unforgiving but predictable. The material wets epoxy resin quickly, the exotherm peaks early in a mass batch, and pot life at bench scale is short once the amine is in. Plan the pour before mixing, not after. Workable practice, distilled from the published properties and the literature melting point: - Warm waxed or solidified drums to 45-50 °C until fully liquid, then homogenise before weighing; unmelted lumps dose badly. - Weigh the amine into the resin within minutes of opening the container. Air exposure builds carbamate skin that later reads as fish eyes in the film. - Keep mixed mass thin during induction when the batch exceeds a few litres; the four-hydrogen structure releases heat fast and a thick pile can discolour. - Ventilate the metering area. The published odour description is not a formality; operators judge leaks by smell long before instruments do. - If a batch must wait, seal the part container with a nitrogen blanket or desiccant, because the water ceiling of 0.05% is easy to exceed through uptake from humid air. Figure 2. Storage temperature scenarios against the literature melting point of about 41-42 °C; bars below the green line mark conditions where drum contents wax or solidify. 6. Applications Fit is best where reactivity and network density pay for themselves and appearance demands are modest. The four segments below all appear as application pages on this site; the table records why the diamine fits or does not. Table 5. Application fit of HMDA by segment. Segment Fit Reasoning Heavy-duty coatings Good with management Dense network resists chemicals; blush control needed in humid shops Structural adhesives Good Fast strength build at 15.5 phr in YLE-128; C6 spacer keeps some flex Composites Conditional Short pot life suits casting and lamination, not long layup schedules Clear decorative coats Poor Odour and carbamate blushing disqualify it where appearance leads Figure 3. Calculated stoichiometric demand of HMDA versus DETA across the three standard resin grades, at the mid-point EEW of each published range. 7. Limitations and Material Verification 7.1 Known Limitations and Unsuitable Uses Say it plainly: this hardener is the wrong choice for water-clear, low-blush finishes, for unventilated indoor work, and for formulations that must sit in an open container for hours. Odour and carbon dioxide uptake rule those uses out regardless of price. Viscosity, epoxy equivalent weight of the amine adduct, and cure kinetics are not published on the product page, so any pot-life or film-property claim beyond the stoichiometry above would be speculation. When those properties matter to a design, request the current TDS and confirm by trial batch; the calculation method in section 4 transfers, but the measured numbers must come from the lot. 7.2 Incoming Inspection, Packaging and Storage A duplicate titration on arrival is cheap insurance. Check purity and water against the certificate; the PRI ceiling of 100 mmol/t flags oxidised amine and is worth a spot check on every new lot. Store drums sealed, off cold floors, above the waxing window in Figure 2. If a drum has solidified, melt once at 45-50 °C and use it soon; repeated melt-solidify cycles waste colour stability and can raise the PRI reading. Packaging and shelf life follow the product page documents. 8. Frequently Asked Questions How much HMDA is needed per 100 parts of bisphenol A epoxy resin? 15.5 phr at a resin EEW of 187 g/eq, calculated as 100 x 29.1 / 187. Dose from the lot certificate EEW when one exists, because a 191 g/eq lot needs 15.2 phr instead. Why has my drum of 1,6-hexanediamine turned solid? The literature melting point is about 41-42 °C, so any storage below that lets the contents crystallise. Warm the sealed drum to 45-50 °C, homogenise, and weigh soon after. Does HMDA cure epoxy faster than DETA? Not faster per equivalent; DETA has the lower AHEW of 20.6 g/eq and gels quickly too. The difference is network density and loading, with HMDA at 15.5 phr against 11.0 phr in the same resin. Can 1,6-hexanediamine be used for clear coatings? Rarely a good idea. Carbon dioxide uptake blushes the film and the ammonia odour needs extraction. Cycloaliphatic hardeners such as MACM serve clear work better. What does the PRI value of 100 mmol/t mean? It is the published ceiling for an oxidation-related index on the specification sheet. A rising PRI reading across lots signals amine oxidation, so track it during incoming inspection. Is the 29.1 g/eq equivalent weight measured or calculated? Calculated, from the molecular weight of 116.2 g/mol and four active hydrogens. It is not a published specification item, and any measured amine value from the certificate takes precedence for dosing. 9. Conclusions As an HMDA epoxy curing agent, 1,6-hexanediamine earns its place where a dense, fast-building network at a modest 15.5 phr matters more than cosmetics. The 99.90% purity floor and 0.05% water ceiling make dosing auditable, and the arithmetic behind every figure in this report is one division a formulator can repeat. Melting behaviour and odour are the two constraints; both are manageable with warmed drums and ventilation, and both argue for cycloaliphatic or adduct hardeners when appearance leads the specification. 10. References 1. Yolatech product page: HMDA, 1,6-Hexanediamine, CAS 124-09-4, https://www.yolatech.com/16-hexanediamine-hmda-cas-124-09-4 2. HMDA technical data sheet, material safety data sheet and certificate of analysis, supplied with each commercial lot. 3. ASTM D1652, standard test practice for epoxy content of epoxy resins, used as the reference basis for resin EEW values. 4. ISO 3001, plastics, epoxy compounds, determination of epoxy equivalent weight. 5. ASTM E203, standard test method for water using volumetric Karl Fischer titration, referenced for the water ceiling.
    Read More
  • Liquid Phenolic Epoxy Resin YLEP-631: Seven Field Failures
    Liquid Phenolic Epoxy Resin YLEP-631: Seven Field Failures
    Oct 20, 2026
    Liquid phenolic epoxy resin YLEP-631 is a PNE-type novolac grade with 2.7 epoxy groups per molecule. Its published window is an EEW of 168-180 g/eq, a viscosity of 1100-1700 mPa·s at 52 °C and hydrolyzable chlorine below 500 ppm. Seven recurring failure patterns cover most field complaints about it. Figure 1. YLEP-631 pours warm and ships in steel drums; the color sits inside the Gardner limit of 3. 1. Introduction Heat service above 150 °C is the usual reason a formulator leaves a bisphenol A liquid for a novolac epoxy; the same move narrows the process window. YLEP-631 comes from a phenol-formaldehyde novolac glycidylated with epichlorohydrin; the oligomer mixture averages 2.7 epoxide rings per molecule against a fixed two for bisphenol A diglycidyl ether. Diagnosis first. Dosage second. 2. Materials and Methods: Identity and Test Basis for Liquid Phenolic Epoxy Resin YLEP-631 The product page publishes five specification items and a functionality statement; Table 1 sets identity beside them. 2.1 Product Identification and Published Specification Three gaps matter for procurement: no CAS number, density or flash point is published, so transport classification leans on the TDS and MSDS. Table 1. Identity and published specification of YLEP-631. Item Information CAS No. Not published; confirm on the current TDS / MSDS / COA Appearance Colorless to yellowish liquid Color, Gardner 3 maximum EEW, g/eq 168-180 Viscosity 1100-1700 mPa·s at 52 °C Hydrolyzable chlorine, ppm 500 maximum Epoxy functionality 2.7 groups per molecule (as published) Shelf life At least 12 months from manufacture in the original drum 2.2 Test Methods and Data Sources Values in Table 1 are reproduced as published, not re-measured; the lot COA overrides the catalogue window. Epoxy equivalent weight is determined by titration; ASTM D1652 and ISO 3001 describe the two routes in common use. Viscosity is quoted at 52 °C because the grade thickens sharply as it cools; a 25 °C reading is not comparable without a measured curve. Color follows ASTM D1544; hydrolyzable chlorine is a single ceiling, which suits buyers screening lots for ionic contamination. Incoming checks are usually performed in duplicate at two positions in the drum, with a third determination (n = 3) when the pair disagrees. 3. Results and Discussion: Where a 2.7-Functionality Resin Fails Two numbers set the operating window for YLEP-631: 2.7 epoxy groups per molecule and a viscosity specified at 52 °C. 3.1 Structure and the Reactivity Penalty Per kilogram, an EEW of 168-180 g/eq delivers 5.56-5.95 epoxy equivalents; a 184-190 g/eq bisphenol A liquid delivers 5.26-5.43. The gap is 5 to 10 percent. The novolac earns its price elsewhere: 2.7 reactive ends per molecule build network nodes faster than a difunctional resin can, lifting heat deflection and hot wet strength. The same 2.7 ends cause most field failures: more heat per unit mass during cure, less elongation, a shorter margin between workable viscosity and gel. Functionality buys heat resistance with process time. Moisture adds a second penalty: water picked up in a humid storeroom consumes epoxide and feeds the amine blush that spoils thin coatings; drums opened through a coastal summer gel early. 3.2 Field Failure Modes: Symptom, Root Cause, Countermeasure Seven patterns cover most failures reported for systems built on this grade, and each maps to a published number in Table 1. Table 2. Failure modes reported for liquid phenolic epoxy resin YLEP-631 systems. Observed symptom Likely root cause Countermeasure Viscosity creep or gel in a partly used drum Repeated opening in humid air; moisture starts headspace reaction Reseal at once, oldest stock first, re-check at 52 °C Runaway exotherm or char in thick castings 2.7 epoxides per molecule release more heat per unit mass Cast in layers, chill the mould, use a slower amine Cracks or brittle fracture after demoulding High crosslink density, low elongation Blend 20-30 phr of a difunctional liquid, ramp the cure Dry spots on fibre in laminates Bath cooled below the 52 °C reference Hold the bath at 55-60 °C and log it Ionic leakage or copper corrosion Chlorine ceiling is 500 ppm, not zero Screen lot COA; extraction-test the laminate Amine blush or oily film on coatings Moisture condensing on a cold substrate Keep substrate 3 °C above dew point, thin coats Batch color drift in clear parts Gardner 3 maximum allows a wide visual window Agree an internal limit tighter than 3 per lot Two are thermal, two are moisture or stoichiometry errors, the rest storage or specification gaps. Each costs more to fix than the resin. 3.3 Comparison with Alternative Systems Table 3 places YLEP-631 beside four alternatives, using published values only. Table 3. Property comparison of YLEP-631 with alternative epoxy systems (published values). Property YLEP-631 YLEP-638 YLE-128 (DGEBA) YLE-170 (BPF) YLSE-721 EEW, g/eq 168-180 170-190 184-190 160-180 110-125 Form at 25 °C Liquid Semi-solid Liquid Liquid Liquid Viscosity 1100-1700 mPa·s at 52 °C Not published; softening point 36-40 °C 11000-15000 mPa·s at 25 °C 2000-5000 mPa·s at 25 °C 6000-11000 mPa·s at 25 °C Epoxy groups per molecule 2.7 Above 2 2 2 4 YLE-128 bisphenol A epoxy resin stays the reference for room-temperature work: no heating, familiar dosage, two epoxides, a lower heat ceiling. The semi-solid sibling YLEP-638 novolac grade differs in one number: a 36-40 °C softening point instead of a pourable viscosity. YLE-170 bisphenol F resin runs at 2000-5000 mPa·s without warming and shares the 160-180 g/eq bracket but builds a less dense network. YLSE-721 tetrafunctional resin, a glycidylamine at 110-125 g/eq, is the harder-edged route: four epoxides, higher viscosity even at 25 °C, a Gardner allowance of 10. Color is a selection criterion, not a detail, for visible parts. 4. Formulation and Dosage Calculation Stoichiometric hardener demand follows one line, phr being parts per hundred of resin by weight. phr = 100 × AHEW ÷ EEW Table 4 works the equation across the published EEW window. Table 4. Stoichiometric hardener dosage for YLEP-631 across the published EEW window. Hardener Equivalent weight, g/eq phr at EEW 168 phr at EEW 174 phr at EEW 180 DETA (CAS 111-40-0), theoretical AHEW 20.6 12.3 11.8 11.4 MACM (CAS 6864-37-5), published AHEW 60 35.7 34.5 33.3 YLH-9101 (modified amine), published AHEW 92 54.8 52.9 51.1 MHHPA (CAS 25550-51-0), anhydride at ratio 0.85 143.0 85.1 82.2 79.4 Worked example: 2 kg at 174 g/eq takes 100 × 92 ÷ 174 = 52.9 phr of YLH-9101 modified amine, or 1058 g weighed separately. Blends move the target: seventy parts at 174 g/eq with thirty at 170 g/eq give a blend EEW of 172.8 g/eq, and a DETA demand of 11.9 phr. Treat every figure as a starting point: delivered EEW drifts inside its window, and a 10 g error is tolerable in 2 kg but is five percent in a 200 g lab mix. Post-cure belongs in the decision: heat resistance appears only after an elevated-temperature schedule; the current TDS governs the steps. 5. Processing Notes and Operating Window Warming the drum is the first operation, and where most batches go wrong. • Heat indirectly with a water bath or drum heater at 50-60 °C; open flame is out, per the product page. • A 200 L drum needs hours on the heater before the bulk reaches temperature. • Log viscosity at 52 °C against 1100-1700 mPa·s before charging the bath or the mixer. • Weigh resin and hardener by mass, never by volume, and degas 10-15 minutes under vacuum for sections above about 25 mm. • Ramp the cure: hold near 80 °C before climbing to 150-180 °C so the exotherm does not stack. Figure 2. A heater jacket warms the drum for decanting; indirect heat keeps the wall below the reaction point. 6. Applications Six routes appear on the product page, and each spends a different part of the specification. Electronic laminates use the dense network and the 500 ppm chlorine ceiling, watching ionic extraction on fine-line boards. Heat-resistant adhesives take hot strength from the tighter mesh but fail as brittle joints under impact. High-temperature coatings gain chemical resistance after post-cure and lose finish to amine blush on cold substrates. Composites wet out fibre at 1100-1700 mPa·s, but only while the bath holds 55-60 °C. Potting and casting risk exotherm cracking in thick sections; civil engineering grouts and epoxy vinyl inks take chemical resistance from the same network. None runs neat at room temperature; each starts from a warmed bath, a heated substrate or a blend. Figure 3. Wet lay-up shows the 52 °C viscosity first: fabric must be wet out while the bath holds temperature. 7. Limitations and Material Verification 7.1 Known Limitations and Unsuitable Cases This is not the resin for room-temperature hand lay-up, for impact-critical parts, or for flame retardance without additives. The molecule carries neither phosphorus nor bromine; a halogen-free flame-retardant laminate needs a co-resin such as YLDP-320 phenolic flame-retardant resin at 3.0% phosphorus. Viscosity exists only at 52 °C. If your process runs at 25 °C, ask for a measured curve instead of extrapolating. Clear parts need a color agreement tighter than Gardner 3; two compliant lots can look visibly different side by side. 7.2 Incoming Inspection, Packaging, Storage and Safety Incoming inspection should verify EEW by titration against the lot COA, plus color and hydrolyzable chlorine. Reject a lot outside 168-180 g/eq; every dosage moves with it. Storage is standard: well-ventilated, away from flames and direct sunlight, cap closed after use, oldest stock first. Shelf life is at least 12 months in the original drum. Safety information lives in the MSDS. Novolac epoxies are skin sensitisers; gloves and eye protection belong in the written procedure. 8. Frequently Asked Questions Why does a liquid grade need warming before use? YLEP-631 is liquid at 52 °C with 1100-1700 mPa·s, but the novolac backbone thickens sharply as temperature falls. Warming to 50-60 °C restores a workable viscosity. How is the hardener ratio calculated for a 168-180 g/eq novolac? phr = 100 × AHEW ÷ EEW. With MACM cycloaliphatic diamine at AHEW 60 g/eq, 100 g of resin at 174 g/eq takes 34.5 g of hardener. Use the lot COA value, not the catalogue midpoint. What causes cracking in thick YLEP-631 castings? Crosslink density: 2.7 epoxides per molecule build a rigid, low-elongation network, and a thick section adds thermal stress from its own exotherm. Cast in layers, ramp the cure, and consider 20-30 phr of a difunctional liquid. Is 500 ppm hydrolyzable chlorine low enough for electronic laminates? A ceiling, not a guarantee: a lot at 480 ppm passes specification yet may still run high for a fine-line board. Screen each lot COA and extraction-test the laminate when ionic cleanliness is critical. Can YLEP-631 be blended with a bisphenol A resin? Yes, and in practice it usually is. Blending cuts viscosity and cost while the novolac fraction keeps the heat resistance. Recalculate the blend EEW from 100 ÷ (sum of parts ÷ EEW of each) before fixing the hardener weight. Does YLEP-631 provide flame retardance? No. The molecule contains neither bromine nor phosphorus; flame retardance must come from a hardener, a co-resin or an additive, with any RoHS or UL 94 claim verified against current certificates. 9. Conclusions Liquid phenolic epoxy resin YLEP-631 is specified at 168-180 g/eq, 1100-1700 mPa·s at 52 °C, Gardner 3 maximum and 500 ppm hydrolyzable chlorine, with 2.7 epoxy groups per molecule. Its failure history is a history of that functionality: exotherm and brittleness in cure, viscosity and moisture in storage, ionic chlorine in electronics. Used warm, dosed from the lot COA and post-cured on schedule, the grade delivers the heat resistance it is priced for. 10. References 1. Product page, PNE type phenolic epoxy resin YLEP-631, Yolatech: https://www.yolatech.com/pne-type-phenolic-epoxy-resin-ylep-631 (accessed 2026-10-20). 2. Product page, PNE type phenolic epoxy resin YLEP-638, Yolatech: https://www.yolatech.com/pne-type-phenolic-epoxy-resin-ylep-638 (accessed 2026-10-20). 3. Product pages, bisphenol A epoxy resin YLE-127/YLE-128 and bisphenol F epoxy resin YLE-170, Yolatech: https://www.yolatech.com/bisphenol-a-epoxy-resin / https://www.yolatech.com/bisphenol-f-epoxy-resin 4. Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for YLEP-631, Yolatech (available on request). 5. ASTM D1652 (epoxy content, EEW) with ISO 3001 (epoxy equivalent), together with ASTM D1544 (Gardner color), ASTM D445 (kinematic viscosity) and ASTM E203 (Karl Fischer water).
    Read More
  • Methyl Hexahydrophthalic Anhydride: Liquid Casting Hardener
    Methyl Hexahydrophthalic Anhydride: Liquid Casting Hardener
    Oct 19, 2026
    3,4-Methyl hexahydrophthalic anhydride (MHHPA, CAS 25550-51-0) is a colorless liquid anhydride hardener of 50-80 cps at 25 °C. Assay is 98% minimum, the freezing point sits at or below -15 °C. Dosed at 110 phr in a 130 g/eq alicyclic epoxy, MHHPA yields about 123 mPa·s varnish for coil impregnation. Figure 1. The published appearance of 3,4-methyl hexahydrophthalic anhydride is a colourless liquid, so the hardener is pumped and metered without a melting step. 1. Introduction Dry-type transformer coils, cast insulators and potted semiconductors ask the same thing of a resin: flow into a tight winding, then hold electrical strength at temperature. Anhydride-cured epoxy answers with a slow, low-exotherm cure and an ester network that stays stable when hot. The liquid member of that family, MHHPA runs at 50-80 cps with a freezing point at or below -15 °C. An unheated drum stays pourable through most of a northern winter. The cost sits in the oven. An anhydride does not gel at 25 °C in a useful time; it needs a warm tank and a staged cure. Data come from the MHHPA product page and the resin pages compared here. 2. Materials and Methods: Identity and Specification of Methyl Hexahydrophthalic Anhydride Table 1 reproduces every specification line the page carries for 3,4-methyl hexahydrophthalic anhydride; nothing outside it is treated as a specification. 2.1 Product Identification and Specification Table 1. Identity and published specification of 3,4-methyl hexahydrophthalic anhydride (MHHPA). Item Published value Product name 3,4-Methyl hexahydrophthalic anhydride (MHHPA) CAS No. 25550-51-0 Appearance Colorless liquid Color, Pt-Co Max. 50 Content, % Min. 98 Viscosity, cps at 25 °C 50-80 Freezing point, °C Max. -15 Iodine value, g I2/100 g Max. 1.0 Packaging and shelf life Drums and IBC tanks; 12 months in original packing Storage 5-30 °C, dry, away from oxidants and acids 2.2 Test Methods and Data Sources Three data classes appear here, and a buyer should keep them apart. Page values are the ten lines in Table 1. Calculated values are the anhydride equivalent weight of 168.19 g/eq, from C9H12O3 with one anhydride group, plus every mix viscosity in Table 3. Empirical values, such as the 0.85 factor and accelerator levels, are starting points. Water is determined by Karl Fischer titration according to ASTM E203, and resin epoxy equivalents follow ASTM D1652 or ISO 3001. Flash point is not published; take it from the MSDS, determined according to ASTM D93 or ISO 3679. Every calculated number can be reworked from the equations in section 4. 3. Results and Discussion: Ring-Opening Chemistry and Viscosity MHHPA cures epoxy through an anhydride ring rather than an amine hydrogen, and that difference accounts for the viscosity, pot life and heat resistance compared in Table 2. 3.1 How the Anhydride Ring Opens on an Epoxy Backbone Cure starts from a hydroxyl, not from the hardener. A residual hydroxyl on the epoxy, or a glycol added on purpose, opens the ring into a monoester carrying a free carboxyl. That carboxyl opens an epoxy group into a diester and regenerates a hydroxyl, which opens the next anhydride. The sequence repeats into a polyester network. Two follow. There is no fast amine-epoxy exotherm, so a thick casting does not run away in the mould. And no free amine is left to blush, so clear castings stay clear. In practice an accelerator is still needed: tertiary amines or imidazoles at 0.5-2 phr cut gel time from hours to minutes at 120 °C. That band is an empirical starting point. Overdosing it is the classic mistake. The mix gels in the pot, and the casting yellows. 3.2 Comparison with Amine Hardeners for the Same Alicyclic Resin Against the two amine hardeners used with the same YLCE-2021 alicyclic epoxy, MHHPA asks for more mass but returns a thinner mix. Table 2. MHHPA against two modified cycloaliphatic amine hardeners on YLCE-2021, a 130 g/eq alicyclic epoxy. Property MHHPA YLH-9101 YLH-3002 Hardener type Anhydride Modified amine Modified amine Appearance Colorless liquid Clear pale yellow Transparent viscous Colour limit Pt-Co max. 50 Gardner max. 2 Gardner max. 1 Viscosity at 25 °C 50-80 cps 250-450 cps 5000-12000 cps Mixing basis AEW 168.19 g/eq AHEW 92 g/eq AHEW 182 g/eq phr on YLCE-2021 110 at k = 0.85 70.8 140.0 Mix viscosity, calculated 123 mPa·s 287 mPa·s 1956 mPa·s Gel at 25 °C Not practical Workable Workable Cure heat required Staged oven cycle Ambient possible Ambient possible The mass penalty is real: 110 kg of MHHPA per 100 kg of YLCE-2021 against 70.8 kg of YLH-9101 amine hardener. The viscosity gain is larger: a 123 mPa·s mix fills a winding that a 287 mPa·s mix only wets slowly. YLH-3002 shows the other end: 182 g/eq, 140 kg per 100 kg of the same resin, and a mix near 1956 mPa·s. That is a casting paste, not an impregnation varnish. Colour cannot be read across columns. Pt-Co and Gardner are different scales, and a Gardner 1 is not a Pt-Co 1. If a sheet mixes them, check which scale the limit belongs to. 4. Formulation and Dosage Calculation for Methyl Hexahydrophthalic Anhydride One equation sets the dose, and the only judgement inside it is the 0.85 factor that most casting shops apply to an anhydride-epoxy pair. phr = 100 × AEW ÷ EEW × k, where AEW is the anhydride equivalent weight, EEW the epoxy equivalent weight of the resin, and k the stoichiometric factor. At k = 1.00 the groups balance. At k = 0.85 the mix runs slightly epoxy-rich, which offsets etherification at high temperature and anhydride lost to hydrolysis in an open bath. Table 3. MHHPA requirement for four Yolatech epoxy grades, at full stoichiometry and at the 0.85 working factor. Epoxy grade EEW used Stoichiometric phr phr at k = 0.85 Mix viscosity, calculated YLCE-2021 130 g/eq 129.4 110.0 123 mPa·s YLSE-0600 105 g/eq 160.2 136.2 695 mPa·s YLE-170 170 g/eq 98.9 84.1 567 mPa·s YLE-128 187 g/eq 89.9 76.4 1309 mPa·s Worked example: 100 kg of YLCE-2021 at 130 g/eq carries 769.2 epoxy equivalents, and 110 kg of MHHPA at 168.19 g/eq carries 654.0 anhydride equivalents. The ratio is 0.850; the batch is 210 kg at 52.4% hardener. Mix viscosity comes from a log-mixing rule, log η = Σ w log η, with 65 cps for MHHPA and the midpoint of each resin window. It predicts rather than measures, so confirm on a viscometer at 25 °C. The rule explains the YLE-128 bisphenol A resin row. At 13000 cps it stays near 1309 mPa·s even at 76.4 phr, so that pair belongs in casting, not impregnation. Accelerator goes in last and shifts gel time more than the MHHPA dose does; check with the supplier before fixing a level. 5. Processing Notes and Operating Window Four conditions decide whether a casting comes out clear: moisture, mix temperature, degassing and the oven ramp. • Keep the drum closed between withdrawals; an anhydride takes up water, turns into the diacid and hazes. • Warm resin and hardener to 50-60 °C before mixing, so the blend degasses. • Add MHHPA first, stir without air entrapment, then accelerator. • Degas under vacuum at mix temperature; low viscosity releases air fast and lets fillers settle fast. • Impregnate at 60-80 °C until bubbling stops. Cold varnish on a cold coil is the usual cause of voids. • Gel at 100-120 °C, post-cure at 140-160 °C, and ramp slowly above 20 mm. Figure 2. Coil impregnation is where the 50-80 cps band matters most, because the varnish has to displace air from the winding before gel. 6. Applications of Methyl Hexahydrophthalic Anhydride The published application list is narrow and electrical: coil impregnation, component casting, and sealing of semiconductors such as insulators, capacitors, LED and digital tubes. Table 4. Published application routes for MHHPA and the line check that matters for each. Process route Published fit Line check Coil impregnation Thin varnish wets fine wire Bath viscosity and water Insulator casting Fills thin walls before gel Mould temperature spread Capacitor and LED potting Clear, colour-stable casting Pt-Co of each incoming lot Semiconductor sealing No amine residue to blush Cure completeness by DSC Coating resin intermediate Anhydride for polyester routes Acid value and water Figure 3. Cast insulators and potted components are the visible end use; the Pt-Co limit on the hardener keeps the cast body water-clear. 7. Limitations and Material Verification MHHPA is the wrong hardener for anything that must cure below 100 °C, and its storage window is narrower than the resin it cures. 7.1 Where MHHPA Is the Wrong Choice Ambient-cure flooring, hand lay-up and field repair are out. The chemistry needs an oven, and no accelerator turns it into a 25 °C system with usable pot life. Cold storage is the second trap. Below -15 °C the liquid freezes; remelt at 60 °C or lower with the lid on, because an open drum pulls in water faster than the crystals melt. Low viscosity cuts both ways. Fillers settle overnight, and thin varnish finds every gap in a worn mould. Shelf life is 12 months against 24 for YLCE-2021, so rotate stock; if a drum sat a year, verify water first. 7.2 Incoming Inspection, Packaging, Storage and Safety Each lot should be checked against the COA on four lines: content at 98% minimum, Pt-Co at 50 maximum, viscosity at 50-80 cps at 25 °C, and iodine value at 1.0 maximum. Water has no published limit. Set one from the first COA and run viscosity in duplicate at 25 °C; a single reading on a cold sample misleads. Anhydrides are skin and respiratory sensitisers. Gloves, goggles and ventilation are the minimum, the SDS governs, and spills go to absorbent rather than to a drain. 8. Frequently Asked Questions What dosage of MHHPA should be used with a 130 g/eq alicyclic epoxy? Full stoichiometry gives 129.4 phr; the 0.85 factor gives 110 phr, or 110 kg per 100 kg of YLCE-2021. Recalculate for other resins with phr = 100 × 168.19 ÷ EEW × 0.85. Why does a liquid hardener still need an oven? Because the ring-opening cure is slow at room temperature. A liquid hardener solves metering only; the hydroxyl attack that starts the chain needs heat. Can MHHPA replace a cycloaliphatic amine hardener one for one? No. The dose moves from 70.8 to 110 phr on the same resin, the cure needs heat, and pot life stretches from hours to days. Reformulate the accelerator and the schedule. What does the iodine value limit of 1.0 actually control? It measures residual unsaturation in the ring. A low value means the 3,4-methyl hexahydrophthalic anhydride is fully hydrogenated, so no aromatic chromophore is left to yellow the casting. How should MHHPA be stored, and what happens if it freezes? Drums and IBC tanks at 5-30 °C, dry and sealed, for 12 months. If it freezes, remelt at 60 °C or below with the lid on and mix before use; water pickup during remelt is the real risk. Is MHHPA suitable for room-temperature flooring or hand lay-up? No. Those processes need an ambient-cure amine. MHHPA belongs in heated impregnation, casting and potting lines. 9. Conclusions MHHPA is a colorless liquid anhydride with 50-80 cps at 25 °C, 98% minimum assay, a freezing point at or below -15 °C and an iodine value capped at 1.0. Its 168.19 g/eq sets 110 phr on a 130 g/eq alicyclic epoxy at the 0.85 factor, and the mix lands near 123 mPa·s. That suits heated impregnation, insulator casting and potting. It does not suit room-temperature cure, and it does not rescue a 13000 cps bisphenol A resin. 10. References 1. Yolatech product page: https://www.yolatech.com/34-methyl-hexahydrophthalic-anhydride-cas-no-25550-51-0-mhhpa (accessed 2026-10-19). 2. Yolatech product page for YLCE-2021 alicyclic epoxy: https://www.yolatech.com/34-epoxycyclohexylmethyl-ylce-2021-cas-2386-87-0 (accessed 2026-10-19). 3. Yolatech product page for YLH-9101: https://www.yolatech.com/curing-agnet-ylh-9101 (accessed 2026-10-19). 4. Yolatech product page for YLH-3002: https://www.yolatech.com/curing-agnet-ylh-3002 (accessed 2026-10-19). 5. Yolatech Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for MHHPA 25550-51-0 (available on request). 6. ASTM D1652, epoxy content of epoxy resins. 7. ISO 3001, determination of epoxy equivalent. 8. ASTM E203, water content by Karl Fischer titration. 9. ISO 3679, flash point, rapid equilibrium closed cup.
    Read More
  • DOPO-NQ Modified Phenolic Epoxy Resin: Blend Ratio Guide
    DOPO-NQ Modified Phenolic Epoxy Resin: Blend Ratio Guide
    Oct 16, 2026
    DOPO-NQ modified phenolic epoxy resin is a halogen-free, phosphorus-bearing flame-retardant epoxy resin supplied as the solid grades YLDP-3300 and YLDP-3375. The two grades cover 280-320 and 350-400 g/eq at softening points of 40-50 and 55-65 °C, and the blend mathematics is set out below in detail. Figure 1. The DOPO-NQ grades are solid resins; the flake form shown is illustrative, since no appearance entry is published on the product page. 1. Introduction Electronics laminates are moving away from bromine, and the chemistry that replaces it has to be reactive rather than additive. DOPO-based epoxy resins are the main reactive-phosphorus route, and the DOPO-NQ product page calls the family one of the most probable alternatives to halogen-containing flame retardants. Three derivatives share the family: DOPO-HQ modified, DOPO-NQ modified and plain DOPO modified grades. The NQ and HQ suffixes denote the naphthoquinone- and hydroquinone-derived DOPO adducts; that is nomenclature, not a published specification, so the TDS is the final word. Both DOPO-NQ grades are solids, softening at 40-50 °C for YLDP-3300 and 55-65 °C for YLDP-3375. That fact shapes everything downstream: how the resin is melted, what varnish solids a line reaches, and how the blend is dosed. This report works through that math, on public page values plus marked calculations. 2. Materials and Methods: Identification of the DOPO-NQ Modified Phenolic Epoxy Resin Grades Table 1 collects every specification item the product page publishes for the two grades. 2.1 Product Identification and Specification Table 1. Identity and published specification of the DOPO-NQ modified phenolic epoxy resin grades. Item YLDP-3300 YLDP-3375 Epoxy equivalent weight 280-320 g/eq 350-400 g/eq Softening point (published as Viscosity, SP/°C) 40-50 °C 55-65 °C Hydrolyzable chlorine 1000 ppm 1000 ppm Appearance, phosphorus content, CAS No. Not published Not published Packaging Drum package Drum package Shelf life 12 months minimum 12 months minimum Both grades share the drum packing, the storage wording and the 12 month minimum shelf life. The chlorine figure is listed without a maximum or typical label. 2.2 Test Methods and Data Sources The EEW windows are oxirane titration results; ASTM D1652 and ISO 3001 are the standard routes behind such figures, and the COA of the delivered lot overrides the catalogue range. The softening points sit under a column headed Viscosity, SP/°C (see 7.1). Hydrolyzable chlorine is listed without a method name. Water content, where a blend needs it, is determined by Karl Fischer titration under ASTM E203. Incoming checks are normally run in duplicate, or as n = 3 determinations when a lot feeds a qualification. 3. Results and Discussion: Solid Form, Softening Point and the Reactivity Budget The published numbers define a solid, mid-EEW, reactive-phosphorus resin family, and every processing decision follows from those three facts. 3.1 What the DOPO-NQ Backbone Does The DOPO unit is a bicyclic phosphaphenanthrene oxide whose P-H bond adds across double bonds and carbonyl groups; naphthoquinone is one standard partner. Bonded this way, the phosphorus sits inside the epoxy backbone instead of migrating like an additive. Within the pair, the higher EEW grade also carries the higher softening point: 350-400 g/eq with 55-65 °C against 280-320 g/eq with 40-50 °C. The consistent direction points to different molecular weights. 3.2 Comparison with Alternative Flame-Retardant Epoxy Systems Table 2 puts the two DOPO-NQ grades beside a DOPO-HQ solid grade, a DOPO-modified solution grade and a brominated resin. Table 2. Property comparison of the DOPO-NQ grades with DOPO-HQ, DOPO-modified solution and brominated alternatives (published values). Property YLDP-3300 / YLDP-3375 YLDP-320 (DOPO-HQ) YLDP-315-M75 (solution) YLEB-300-K75 (brominated) Form at 25 °C Solid, SP 40-50 / 55-65 °C Solid, SP 70-85 °C Solution, 1000-3000 mPa·s at 25 °C Solution, 200-1500 mPa·s Epoxy equivalent weight 280-320 / 350-400 g/eq 300-340 g/eq 295-335 g/eq 280-320 g/eq Hydrolyzable chlorine 1000 ppm 500 ppm maximum Not published Not published Non-volatile content Not published 99.0% minimum 75±1% 75±1% Flame-retardant element Reactive phosphorus Reactive phosphorus (3.0%) Reactive phosphorus Reactive bromine Against the DOPO-HQ grade YLDP-320, the NQ grades are softer solids that melt about 30 °C earlier, at the cost of a chlorine figure twice as high. Against the brominated brominated epoxy resin YLEB-300-K75, the swap is chemical rather than thermal: bromine leaves and bonded phosphorus enters. Whether that pays depends on the rating target and the customer's certification documents. The trade-off is real. 4. Formulation and Dosage Calculation for DOPO-NQ Modified Phenolic Epoxy Resin Laminates rarely run the DOPO resin alone. The usual start is a blend with a liquid bisphenol A epoxy resin YLE-128, published at 184-190 g/eq, and dicyandiamide as the hardener. Blend EEW = (100 + d) ÷ (100 ÷ EEW of the base resin + d ÷ EEW of the DOPO-NQ grade), with d in phr. Hardener demand follows phr = 100 × AHEW ÷ blend EEW. Dicyandiamide has a theoretical AHEW of 21.0 g/eq, calculated from 84.08 g/mol and four active hydrogens. Table 3 works the example with YLDP-3300 at 300 g/eq in a base resin at 187 g/eq. The chlorine column counts only the DOPO-NQ component at 1000 ppm. Table 3. Blend EEW, dicyandiamide demand and resin mass per equivalent for YLDP-3300 loadings in a base resin at 187 g/eq (calculated). YLDP-3300 loading, phr Blend EEW, g/eq DICY demand, phr Resin mass per equivalent, kg/eq Chlorine contribution of the component, ppm 0 187.0 11.2 0.187 0 20 199.5 10.5 0.200 167 40 209.6 10.0 0.210 286 60 217.8 9.6 0.218 375 100 230.4 9.1 0.230 500 The blend EEW rises with every added part, so hardener demand falls from 11.2 to 9.1 phr; that is the opposite direction to a low-EEW reactive diluent, and it is easy to get backwards when copying a diluent recipe. The mass column is the cost reading: each kilogram of YLDP-3300 buys fewer epoxy equivalents than a kilogram of base resin. Whether that pays depends on what the phosphorus buys back in the laminate. The chlorine column is the reliability reading: a 40 phr loading contributes about 286 ppm before base resin, hardener and catalyst add theirs. For high-reliability boards the figure belongs in the incoming specification, and a tight budget favors the DOPO-HQ grade at 500 ppm maximum. Dosage is a trade-off, not a constant. 5. Processing Notes and Operating Window The operating window is set by the softening points, and the grades differ by 15 °C. Melting: YLDP-3300 softens at 40-50 °C, so a jacketed vessel is usually enough; YLDP-3375 needs 55-65 °C and a longer melt. Avoid holding the resin far above its softening point, because color and EEW can drift. Dissolving: add solvent in portions and check viscosity after each. The sibling solution grades run at 70-75% solids, a workable anchor, but the reachable solids here is not published; confirm on the TDS. Humidity: the page says to close the cap tightly after each use. A drum left open in a humid shop picks up water, which shifts the stoichiometry and shows up later as blush or soft cure. Filtration: melt, homogenize and filter before impregnation; a solid grade can carry packaging traces. Cure: dicyandiamide systems typically cure in a press at elevated temperature. The schedule depends on the accelerator package, so run a gel-time check before locking a batch size. Figure 2. Solid resin is charged into a heated vessel and dissolved before the hardener stage. 6. Applications of the DOPO-NQ Modified Phenolic Epoxy Resin Grades The product page lists three applications, all laminate-side. Table 4 links each to what the resin contributes and what to verify. Table 4. Applications listed on the product page and the verification point for each. Application Role of the resin Verification point Halogen-free flame-retardant printed circuit substrates Bonded phosphorus replaces bromine in the laminate Flame rating on the customer's own laminate panels Electronic copper-clad laminates Solid grade melted into varnish for impregnation Varnish solids and viscosity measured at line temperature Electrical laminates Heat resistance and low water absorption from the aromatic backbone Water uptake and flex properties after cure All three run through the same impregnation logic: melt or dissolve, mix with hardener, wet the fabric, press. Inside the pair, the choice is a softening-point decision. Figure 3. Copper-clad laminate panels, the second application listed on the product page. 7. Limitations and Material Verification 7.1 Known Limitations and Unsuitable Cases Appearance, phosphorus content, CAS number, chemical name and molecular weight are all absent from the page, so documents that require a CAS entry cannot be filled from it. The TDS, MSDS and COA govern. The parameter table labels the third column Viscosity (SP/°C) while the unit is °C and the values rise with grade. Read as published, those are softening points, not viscosities; confirm on the TDS before copying the row into a drawing. Not the right grade when the process needs a room-temperature liquid, when a published CAS number is required, or when the chlorine budget sits below 1000 ppm and the DOPO-HQ grade fits instead. Swapping between the two grades, or between NQ and HQ chemistry, changes both stoichiometry and melt step; requalification is the honest path. 7.2 Incoming Inspection, Packaging, Storage and Safety A workable incoming panel is EEW by oxirane titration, softening point, hydrolyzable chlorine titration and water by Karl Fischer titration, run in duplicate or as n = 3. The page states drum package and at least 12 months from manufacture in the original packing at ambient temperature, stored well-ventilated away from flames and direct sunlight. Safety handling follows the Material Safety Data Sheet. Statements about REACH, RoHS or UL 94 belong to the certificate that ships with the lot; a catalogue page is not a certificate. 8. Frequently Asked Questions What is DOPO-NQ modified phenolic epoxy resin? It is the naphthoquinone-derived branch of the family: solid grades YLDP-3300 and YLDP-3375, EEW 280-320 and 350-400 g/eq, softening points 40-50 and 55-65 °C. Why does the table show a temperature, not a viscosity? The column is published as Viscosity (SP/°C), yet the values carry the unit °C and scale with grade, which is softening-point behavior; the TDS wording governs. What happens to the hardener dosage when YLDP-3300 is blended into a bisphenol A resin? The blend EEW rises rather than falls. At 40 phr in a resin at 187 g/eq the blend EEW reaches about 210 g/eq and the dicyandiamide demand drops from 11.2 to 10.0 phr. How much hydrolyzable chlorine does the DOPO-NQ component add to a blend? The grades are listed at 1000 ppm. At 40 phr the component contribution works out to about 286 ppm, which is why the figure belongs in the incoming specification. Is a phosphorus content published for YLDP-3300 and YLDP-3375? No. Neither grade carries a phosphorus entry, unlike the DOPO-HQ grade at 3.0%, so loading has to be set from the COA of the delivered lot. What should incoming inspection of a DOPO-NQ lot cover? EEW by titration, softening point, hydrolyzable chlorine and water by Karl Fischer titration, in duplicate as a minimum. Drum package and a 12 month minimum shelf life are also specified. 9. Conclusions The published record is short but usable: EEW 280-320 and 350-400 g/eq, softening points 40-50 and 55-65 °C, hydrolyzable chlorine at 1000 ppm, drum package and a 12 month minimum shelf life. Blended into a bisphenol A base resin, the grades raise the blend EEW and cut the dicyandiamide demand from 11.2 toward 9.1 phr. The missing phosphorus value comes from the COA. Treat the pair as a softening-point choice, dose on the blend stoichiometry, and anchor the unpublished items to the current TDS, MSDS and COA. 10. References 1. DOPO-NQ modified phenolic epoxy resin, product page, Yolatech. https://www.yolatech.com/dopo-nq-modified-phenolic-epoxy-resin (accessed 2026-10-16). 2. DOPO-HQ modified phenolic epoxy resin YLDP-320, product page, Yolatech. https://www.yolatech.com/dopo-hq-modified-phenolic-epoxy-resin-yldp-320 3. DOPO modified phenolic epoxy resin, solution grades, product page, Yolatech. https://www.yolatech.com/dopo-modified-phenolic-epoxy-resin 4. Brominated epoxy resin grades YLEB-265 to YLEB-425S, product page, Yolatech. https://www.yolatech.com/brominated-epoxy-resin 5. Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for the two DOPO-NQ grades, Yolatech, available on request. 6. ASTM D1652 and ISO 3001, titration routes behind the published epoxy equivalent weights. 7. ASTM E203, Karl Fischer titration for water content on incoming lots.
    Read More
  • Bio-Based Epoxy Reactive Diluent: YLD-9016 Dosage Guide
    Bio-Based Epoxy Reactive Diluent: YLD-9016 Dosage Guide
    Oct 14, 2026
    Bio-based epoxy reactive diluent YLD-9016 is a difunctional cardanol diglycidyl ether specified at EEW 250-330 g/eq and 60-150 mPa·s at 25 °C. CAS 68390-54-5, non-volatile content 99.7% minimum, derived from cashew nut shell liquid. At 15 phr the diluent cuts a 13000 mPa·s resin to about 6300 mPa·s. Figure 1. Cardanol diglycidyl ether YLD-9016 is supplied as a light yellowish brown liquid with a Gardner color of 12 maximum and ships in 200 kg drums. 1. Introduction A high-solids epoxy formulation needs its viscosity cut by something that stays in the film. Solvent leaves as VOC; a reactive diluent cures into the network instead. That is the argument for glycidyl ethers. The cardanol line already covers three answers: cardanol glycidyl ethers YLD-9006 monofunctional at 30-50 mPa·s, and standard cardanol diglycidyl ether YLD-9014 with its variant YLD-9014A difunctional but at 1000-3000 mPa·s. Resin-class flow, not diluent-class flow. YLD-9016 publishes 60-150 mPa·s with two epoxy groups per molecule. It is the only grade in the family that pairs diluent-class viscosity with difunctional reactivity, on a cashew-derived backbone. Viscosity is only half the argument. Specification values below come from the public Yolatech product pages, derived constants are marked calculated, and dosage figures are worked examples. 2. Materials and Methods: Identification of Bio-Based Epoxy Reactive Diluent YLD-9016 Table 1 collects the identity and specification data published for YLD-9016. 2.1 Product Identification and Specification Table 1. Identity and published specification of bio-based epoxy reactive diluent YLD-9016. Item Information Product name Cardanol Diglycidyl Ether YLD-9016 Chemical family Cashew oil modified difunctional glycidyl ether CAS No. 68390-54-5 Appearance Light yellowish brown liquid Color, G Max. 12 EEW, g/eq 250-330 Viscosity (25 °C), mPa·s 60-150 Non-volatile, % Min. 99.7 Epoxy functionality 2 (bifunctional, as published) Raw material base Cashew nut shell liquid, plant-derived Packaging 200 kg drum Shelf life 12 months in original packing 2.2 Test Methods and Data Sources Table 1 reproduces the published figures without alteration. The report adds no laboratory data of its own. Epoxy equivalent weight is determined by titration under ASTM D1652 or ISO 3001, and the figure on the current TDS governs. Color is determined by ASTM D1544, and viscosity is measured at 25 °C under the method stated in the current TDS. Incoming checks on a glycidyl ether lot are typically run in duplicate, or as n = 3 determinations from separate positions in the drum. 3. Results and Discussion: Viscosity, Functionality and Dilution Behaviour Two published numbers separate YLD-9016 from the cardanol line: 60-150 mPa·s at 25 °C and 99.7% minimum non-volatile. 3.1 Structure and Reactivity of the Cardanol Backbone Cardanol is a meta-substituted phenol carrying a C15 unsaturated alkyl chain, obtained from cashew nut shell liquid. Capping that core with two glycidyl groups gives a rigid aromatic ring, a long hydrophobic tail and two reactive epoxide ends. Each part does one job. The epoxide ends consume amine and enter the network. The alkyl chain buys flexibility and water repellency. The aromatic ring lets a film harden at room and low temperatures. Nothing evaporates. A non-volatile content of 99.7% minimum means essentially the whole dose becomes part of the film. 3.2 Comparison with Alternative Systems Table 2 places YLD-9016 beside the petrochemical ethers it replaces and the sibling cardanol grades. Table 2. Property comparison of bio-based epoxy reactive diluent YLD-9016 with alternative reactive diluents (published values). Property YLD-9016 YLD-9014 AGE YLD-7003 BGE YLD-9004A HDDGE YLD-6008 Epoxy functionality 2 2 1 1 2 EEW, g/eq 250-330 290-350 294-313 147-157 142-155 Viscosity (25 °C), mPa·s 60-150 1000-3000 4-10 Max. 2 10-25 Raw material base Cashew, bio-based Cashew, bio-based Petrochemical Petrochemical Petrochemical Hardener demand vs 187 g/eq DGEBA Lowers Lowers Lowers Raises Raises   On raw thinning power the petrochemical ethers win: butyl glycidyl ether BGE YLD-9004 at 2 mPa·s maximum and 1,6-hexanediol diglycidyl ether YLD-6008 at 10-25 mPa·s, against 60-150 mPa·s. What they give back is hardener demand. At EEW 147-157 and 142-155 g/eq they pull a blend below the 184-190 g/eq of a standard bisphenol A resin, so every added part costs amine. YLD-9016 and alkyl (C12-C14) glycidyl ether YLD-7003 sit above 250 g/eq and push it down. Color limits are not comparable across the columns: the cardanol grades are limited in Gardner, the petrochemical ethers in APHA. Where a difunctional petrochemical ether is the incumbent, the product page names 1,4-butanediol diglycidyl ether YLD-6018L as a comparator, published at 98% minimum purity and no EEW window. 4. Formulation and Dosage Calculation Blend EEW and hardener demand follow two equations, with phr read as parts per hundred parts of resin by weight. Blend EEW = (100 + d) ÷ (100 ÷ EEW + d ÷ EEW9016), where d is the diluent loading in phr phr = 100 × AHEW ÷ EEW Table 3. Dilution and hardener dosage worksheet for 100 parts of bisphenol A epoxy resin YLE-128 at 187 g/eq and 13000 mPa·s, blended with YLD-9016 at its 290 g/eq and 105 mPa·s midpoints (calculated). YLD-9016 loading, phr Blend EEW, g/eq DETA phr at AHEW 20.6 MACM phr at AHEW 60 Viscosity estimate, mPa·s 0 187 11.0 32.1 13000 10 193 10.7 31.1 8400 15 196 10.5 30.6 6300 20 199 10.4 30.2 5800 Viscosity is estimated by a log-rule blend, which tracks glycidyl ether systems well enough for screening. A 15 phr loading takes an 11000-15000 mPa·s bisphenol A epoxy resin YLE-128 down to about 6300 mPa·s, a 51% cut. For a 1,000 g resin charge, weigh 150 g of YLD-9016 and 306 g of MACM curing agent at its published AHEW of 60 g/eq. Treat 30.6 phr as a starting point, because the 250-330 g/eq window is 80 g/eq wide. Dilution efficiency, not price, is the honest basis. No list price is published, so express the trade-off as viscosity reduction per phr and settle it against your own drum quotation. On that basis 15 phr of BGE reaches about 3500 mPa·s and wins on thinning, but YLD-9016 wins on volatile-free composition and hardener demand. If a formulation has to stay stiff, cap the loading near 20 phr and verify hardness development on the actual system. 5. Processing Notes and Operating Window Field practice with YLD-9016 reduces to five points. Add the diluent to the resin first and homogenize before the hardener enters; adding it after the amine invites stoichiometry errors. If a drum comes off a winter pallet, let it reach room temperature before reading viscosity, because the 60-150 mPa·s window is temperature-specific. Recalculate hardener phr from the lot COA each time a new drum arrives. Keep drums sealed between draws; glycidyl ethers absorb moisture slowly in humid storage, and water shows up later as blush. Run a gel-time check before locking pot life; difunctional diluents gel differently from the monofunctional ethers they replace. Figure 2. Diluent is poured into the resin and homogenized before the hardener is dosed, keeping the mix stoichiometry under control. 6. Applications The page lists high-solids and solvent-free coatings, adhesives and composites, plus surface alkylation of silica and titanium dioxide. Table 4. Application fit for bio-based epoxy reactive diluent YLD-9016 and the resin grades commonly blended with it. Application Why YLD-9016 fits Resin companion High-solids coatings Reactive dilution at 99.7% minimum non-volatile content YLE-128 Solvent-free 2K systems Co-cures into the network instead of leaving as emission YLE-170 Adhesives Flexibility, impact resistance and water resistance YLE-128 Composites and FRP Impregnation aid at diluent-class viscosity YLE-170 Filler surface treatment Alkylates silica and titanium dioxide surfaces None The coating logic runs through epoxy resin coatings: wherever a solvent-borne recipe converts to high solids, a reactive diluent with a negligible volatile fraction is the direct swap, but the hardener ratio still needs recalculating. Adhesive work is covered in epoxy resin adhesives, impregnation in epoxy resin composites. Figure 3. Solvent-free epoxy floor coating applied by roller, the application where reactive dilution replaces solvent entirely. 7. Limitations and Material Verification 7.1 Known Limitations and Unsuitable Cases Four specification gaps deserve confirmation before YLD-9016 is written into a purchase specification. Hydrolyzable chlorine, water content, density, flash point and molecular formula are not published; the grade gives only a non-volatile floor of 99.7%. Confirm them on the current TDS, MSDS and COA. The 250-330 g/eq EEW window is 80 g/eq wide, wider than the 184-190 g/eq of YLE-128. Batch drift inside it moves hardener demand by about 3% at a fixed loading. This grade is not the right choice for a stiff, heat-deflection-critical casting, and it is not a flame retardant: no halogen or phosphorus content is published. The food-grade statement appears on the YLD-9006 page, not here. Do not carry the claim across without written confirmation. 7.2 Incoming Inspection, Packaging, Storage and Safety Incoming inspection should confirm EEW by titration against the lot COA, plus color and non-volatile content. Reject a lot outside 250-330 g/eq. Packaging is a 200 kg drum with a stated shelf life of 12 months from manufacture in the original packing, stored cool and dry out of direct sunlight. Handling detail is carried by the Material Safety Data Sheet. Glycidyl ethers are skin sensitisers, so gloves and eye protection belong in the procedure. RoHS, REACH or UL 94 status has to be confirmed by the buyer against current certificates. A general product description implies no certification. 8. Frequently Asked Questions What is bio-based epoxy reactive diluent YLD-9016 made from? YLD-9016 is a cardanol diglycidyl ether derived from cashew nut shell liquid, with two epoxy groups per molecule. The page positions it as a non-toxic, renewable alternative to petrochemical ethers such as AGE and BGE. How is YLD-9016 different from YLD-9014 and YLD-9014A? The difference is viscosity. YLD-9016 runs at 60-150 mPa·s while YLD-9014 and YLD-9014A both sit at 1000-3000 mPa·s; all three share CAS 68390-54-5. How much YLD-9016 should be blended into a bisphenol A epoxy resin? Start between 10 and 20 phr. A log-rule estimate for 15 phr in an 11000-15000 mPa·s bisphenol A resin lands near 6300 mPa·s, and the right level depends on the stiffness the part can give up. Does YLD-9016 change the hardener dosage? Yes, downward. Its own EEW sits above the 184-190 g/eq of a standard bisphenol A resin, so each added part raises the blend EEW; at 15 phr the calculated MACM demand drops from 32.1 to 30.6 phr. Can YLD-9016 replace butyl glycidyl ether in a solvent-free coating? On thinning alone, no. BGE at 2 mPa·s maximum cuts deeper per phr and usually wins that comparison, so the swap makes sense when volatile content, odor or hardener demand carries more weight than the last third of the viscosity cut. Does YLD-9016 soften the cured coating? It adds flexibility by design, which is a trade rather than a defect. The alkyl chain lowers modulus and heat deflection while raising impact and water resistance, and the effect depends on the loading. 9. Conclusions Bio-based epoxy reactive diluent YLD-9016 is published at EEW 250-330 g/eq, 60-150 mPa·s at 25 °C, Gardner color 12 maximum and 99.7% minimum non-volatile content, in 200 kg drums with a 12-month shelf life. Its position is narrow but useful: diluent-class viscosity on a difunctional, cashew-derived backbone, with lower hardener demand than the petrochemical ethers it replaces. Dose by stoichiometry from the lot COA, cap the loading near 20 phr, and keep the deep-thinning monofunctional ethers for jobs that need them. 10. References 1. Product page, Cardanol Diglycidyl Ether YLD-9016, Yolatech: https://www.yolatech.com/cardanol-diglycidyl-ether-yld-9016 2. Product page, Cardanol Diglycidyl Ether YLD-9014, Yolatech: https://www.yolatech.com/cardanol-diglycidyl-ether-yld-9014 3. Product page, Butyl glycidyl ether BGE YLD-9004, Yolatech: https://www.yolatech.com/butyl-glycidyl-etherbge-yld-9004 4. Product page, 1,6-Hexanediol diglycidyl ether YLD-6008, Yolatech: https://www.yolatech.com/16-hexanediol-diglycidyl-ether-yld-6008 5. Product page, liquid bisphenol A epoxy resin YLE-127 / YLE-128, Yolatech: https://www.yolatech.com/bisphenol-a-epoxy-resin 6. Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for Cardanol Diglycidyl Ether YLD-9016, Yolatech (available on request). 7. ASTM D1652 and ISO 3001, titration routes for epoxy content and epoxy equivalent weight. 8. ASTM D1544 for Gardner color, ASTM D445 for kinematic viscosity, ASTM E203 for water by Karl Fischer titration.
    Read More
  • Phenolic Novolac Epoxy Resin: YLEP-638 Selection Guide
    Phenolic Novolac Epoxy Resin: YLEP-638 Selection Guide
    Oct 13, 2026
    Phenolic novolac epoxy resin YLEP-638 is a multifunctional epoxy resin from phenol-formaldehyde novolac and epichlorohydrin. Its published specification lists an epoxy equivalent weight of 170-190 g/eq, Gardner color 3.0 maximum, a softening point of 36-40 °C and hydrolyzable chlorine below 500 ppm. Figure 1. YLEP-638 phenolic novolac epoxy resin is supplied in steel drums and is a semi-solid at room temperature; the printed label carries the lot number, manufacturing date and expiry date. 1. Introduction Continuous service above roughly 150 °C is where a difunctional bisphenol A epoxy resin stops being the obvious answer. Phenolic novolac epoxy resin trades easy flow for a denser cured network. Built on a phenol-formaldehyde novolac core condensed with epichlorohydrin, YLEP-638 carries more than two epoxide rings per molecule on average. Published data on the sibling grade YLEP-631 records an average of 2.7 epoxy groups per molecule, against two for bisphenol A diglycidyl ether. Specification values below are quoted from the public Yolatech product pages, derived constants are marked calculated, and every dosage figure is a worked example rather than a recipe. Selection comes first. Dosage comes second. 2. Materials and Methods: Identification of Phenolic Novolac Epoxy Resin YLEP-638 The YLEP-638 product page publishes five specification items and a five-line application list. Table 1 sets identity data beside those published values. 2.1 Product Identification and Specification Table 1 collects identity data from the product page and flags the derived rows. Table 1. Identity and published specification of phenolic novolac epoxy resin YLEP-638. Item Information Product name PNE type phenolic epoxy resin YLEP-638 Chemical family Phenolic novolac (PNE) multifunctional epoxy resin CAS No. Not published; confirm on the current TDS / MSDS / COA Appearance Colorless to yellowish liquid (as published) Color, Gardner 3.0 maximum EEW, g/eq 170-190 Softening point (SP), °C 36-40 Hydrolyzable chlorine, ppm 500 maximum Epoxy functionality Above 2 (YLEP-631 published at 2.7) Packaging Drum Shelf life At least 12 months in original packing 2.2 Test Methods and Data Sources Values in Table 1 are quoted as published. No independent laboratory work was performed for this report. Epoxy equivalent weight is determined by titration, and the figure in the current TDS governs. ASTM D1652 and ISO 3001 describe the two common routes. Color is determined by ASTM D1544. Viscosity of the liquid comparator grades is measured at 25 °C; the YLEP-631 figure is quoted at 52 °C because that grade is not free-flowing at ambient. Hydrolyzable chlorine is given as one ceiling instead of a range, which matters where ionic chloride drives copper corrosion. Water content is normally found by Karl Fischer titration. Incoming checks on a novolac epoxy lot are usually run in duplicate, or as n = 3 determinations from separate positions in the same drum. 3. Results and Discussion: Structure, Reactivity and Grade Selection Two structural facts drive most selection decisions around YLEP-638: the novolac backbone and the 170-190 g/eq epoxy equivalent weight. 3.1 Structure and Reactivity of the Novolac Backbone Phenol and formaldehyde condense under acid catalysis into a novolac oligomer carrying several phenolic hydroxyls. Epoxidation with epichlorohydrin converts those hydroxyls into glycidyl ether groups, so one molecule can end in more than two epoxide rings. Higher functionality raises crosslink density after cure. Heat deflection temperature, chemical resistance and hot wet strength climb with it. Elongation falls. An epoxy equivalent weight of 170-190 g/eq sits close to the 184-190 g/eq of a standard liquid bisphenol A grade, so hardener demand per 100 g of resin stays in the same bracket. Functionality is the difference maker, not EEW. 3.2 Comparison with Alternative Systems Table 2 places YLEP-638 beside four published grades that buyers weigh against it. Table 2. Property comparison of YLEP-638 with alternative epoxy systems (published values). Property YLEP-638 YLEP-631 YLE-128 (DGEBA) YLE-170 (BPF) YLDP-320 EEW, g/eq 170-190 168-180 184-190 160-180 300-340 Form at ambient Semi-solid Liquid Liquid Liquid Solid Softening point, °C 36-40 Not published Not published Not published 70-85 Viscosity Not published 1100-1700 mPa·s at 52 °C 11000-15000 mPa·s at 25 °C 2000-5000 mPa·s at 25 °C Not published Epoxy groups per molecule Above 2 2.7 2 2 Not published Bisphenol F resin YLE-170, at 160-180 g/eq and 2000-5000 mPa·s, is the low-viscosity liquid option and wets fibre better than a novolac melt. Its cured heat resistance sits a little lower. YLEP-631 is the same chemistry at 168-180 g/eq with a published 1100-1700 mPa·s viscosity at 52 °C, so it pours where PNE type phenolic epoxy resin YLEP-638 will not flow unassisted. YLDP-320 answers a different question: 300-340 g/eq, 3.0% phosphorus, supplied as a solid for halogen-free flame-retardant laminates. Same backbone, different job. 4. Formulation and Dosage Calculation For an amine-cured system the stoichiometric hardener loading follows one equation, with phr read as parts per hundred parts of resin by weight. phr = 100 × AHEW ÷ EEW Anhydride curing uses the same logic with an anhydride equivalent weight, and the practical ratio usually falls between 0.85 and 1.00 of the theoretical figure. Table 3. Stoichiometric hardener dosage for phenolic novolac epoxy resin YLEP-638, calculated from the published EEW window. Hardener Equivalent weight, g/eq phr at EEW 170 phr at EEW 180 phr at EEW 190 DETA (CAS 111-40-0), theoretical AHEW 20.6 12.1 11.4 10.8 MACM (CAS 6864-37-5), published AHEW 60 35.3 33.3 31.6 MHHPA (CAS 25550-51-0), anhydride weight at ratio 0.90 151.2 88.9 84.0 79.6 A 500 g batch of YLEP-638 measuring 180 g/eq needs 100 × 60 ÷ 180 = 33.3 phr of MACM curing agent, or about 167 g weighed into the mix. Treat 33.3 phr as a starting point. Delivered epoxy equivalent weight moves inside the 170-190 g/eq window, and the amine content of a hardener lot rarely lands on the published figure. 5. Processing Notes and Operating Window YLEP-638 does not pour at room temperature. Warming the drum to 60-80 °C brings it to a workable viscosity, and blending with a liquid grade or a reactive diluent does the same at lower temperature. Pre-warm resin and hardener separately. Check the MHHPA anhydride or amine against its own viscosity or melting point before either enters the mix. Mix in one direction and keep the vortex shallow. Air whipped into a high-viscosity novolac blend is hard to remove afterwards. Degas under vacuum if the part is thick. A 10 to 15 minute step covers sections up to about 25 mm. Gel time shortens sharply as batch weight grows, because the exotherm of a novolac system concentrates in the mass. Check pot life at your own mix weight instead of trusting a table value. 6. Applications Five end uses appear on the YLEP-638 product page: coating, potting and casting, adhesive, laminates, and composites. Table 4. Application fit for phenolic novolac epoxy resin YLEP-638 and the grades commonly blended with it. Application Why YLEP-638 fits Companion grade Laminates Dense network, 500 ppm maximum hydrolyzable chlorine YLDP-320 for flame retardance Coatings Chemical and thermal resistance at high service temperature YLE-170 to cut viscosity Adhesives Hot wet strength under sustained load YLE-128 for flexibility Composites Mechanical strength at temperature after post-cure YLE-170 for fibre wet-out Potting and casting Rigid encapsulation of thermally stressed parts YLE-128 to ease flow YLEP-638 rarely runs alone. It is blended with a lower-viscosity resin to reach a processable viscosity, and the blend ratio decides the cured balance between heat resistance and toughness. 7. Limitations and Material Verification 7.1 Known Limitations and Unsuitable Cases Three published details deserve confirmation before YLEP-638 is written into a specification. The specification table labels its 36-40 °C row as viscosity in degrees Celsius, which describes a softening point rather than a viscosity. Confirm the property on the current TDS. Appearance is published as a colorless to yellowish liquid, while the product description calls the same resin semi-solid. Both cannot hold for one drum at 25 °C. No CAS number or epoxy functionality value is published for YLEP-638. Hand lay-up at ambient is not a suitable process for this grade. Neither is a flexible, impact-critical part: the dense network that buys heat resistance costs elongation. Pick YLEP-631 when flow governs the process, and YLEP-638 when heat and chemical resistance govern the part. 7.2 Incoming Inspection, Packaging, Storage and Safety Incoming inspection should confirm epoxy equivalent weight by titration against the lot COA, plus color and hydrolyzable chlorine. Reject a lot whose EEW sits outside 170-190 g/eq, because the dosage table shifts with it. Storage follows the standard epoxy routine: a well-ventilated area, away from flames and direct sunlight, with the cap closed tightly after each use. The product page states at least 12 months from manufacture in the original packing at ambient temperature, and drum is the published package. Safety information sits in the Material Safety Data Sheet. Novolac epoxy resins are skin sensitisers, so gloves and eye protection belong in the handling procedure. Any RoHS, REACH or UL 94 statement must be verified by the customer against current certificates. No certification is implied by a general product description. 8. Frequently Asked Questions What is the epoxy equivalent weight of phenolic novolac epoxy resin YLEP-638? The published range is 170-190 g/eq. Epoxy equivalent weight is determined by titration under the method stated in the current TDS, and ASTM D1652 covers the standard route. Use the lot COA figure for dosage work. How much hardener does YLEP-638 need per 100 g of resin? With MACM curing agent at a published AHEW of 60 g/eq, 100 g of YLEP-638 at 180 g/eq takes 33.3 g. The same 100 g with diethylenetriamine DETA at a theoretical 20.6 g/eq takes 11.4 g. Can YLEP-638 replace a liquid bisphenol A epoxy resin one for one? Not at ambient temperature. YLE-128 is a 11000-15000 mPa·s liquid, while YLEP-638 is a semi-solid with a 36-40 °C softening point, so warming or blending is required. Expect shorter gel time and a stiffer cured part. Why is YLEP-638 supplied as a semi-solid rather than a liquid? The novolac backbone raises functionality, and higher functionality raises viscosity at a given epoxy equivalent weight. That is the trade-off the grade accepts in return for a denser cured network. What is the difference between YLEP-638 and YLEP-631? Both are PNE-type phenolic novolac epoxy resins capped at 500 ppm hydrolyzable chlorine. YLEP-631 is published at 168-180 g/eq with a 1100-1700 mPa·s viscosity at 52 °C; YLEP-638 is published at 170-190 g/eq with a 36-40 °C softening point. Is YLEP-638 suitable for halogen-free electronic laminates? It can serve as the base resin, but it carries neither phosphorus nor bromine, so flame retardance has to come from the hardener, from a co-resin such as YLDP-320 at 3.0% phosphorus, or from an additive. Hydrolyzable chlorine at 500 ppm maximum is the ionic figure that matters. 9. Conclusions YLEP-638 is a PNE-type phenolic novolac epoxy resin published at 170-190 g/eq, 3.0 maximum Gardner color, a 36-40 °C softening point and 500 ppm maximum hydrolyzable chlorine. It ships in drums with a stated 12-month shelf life. Its value lies in crosslink density rather than in flow. Warm it or blend it, then dose by stoichiometry from the measured epoxy equivalent weight of the lot. Choose the lower-viscosity YLEP-631 phenolic novolac grade when flow governs the process, and YLEP-638 when heat and chemical resistance govern the part. 10. References 1. Product page, PNE type phenolic epoxy resin YLEP-638, Yolatech: https://www.yolatech.com/pne-type-phenolic-epoxy-resin-ylep-638 2. Product page, PNE type phenolic epoxy resin YLEP-631, Yolatech: https://www.yolatech.com/pne-type-phenolic-epoxy-resin-ylep-631 3. Product page, bisphenol A epoxy resin grades YLE-127 and YLE-128, Yolatech: https://www.yolatech.com/bisphenol-a-epoxy-resin 4. Product page, bisphenol F epoxy resin grade YLE-170, Yolatech: https://www.yolatech.com/bisphenol-f-epoxy-resin 5. Product page, DOPO-HQ modified phenolic epoxy resin YLDP-320, Yolatech: https://www.yolatech.com/dopo-hq-modified-phenolic-epoxy-resin-yldp-320 6. Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for PNE type phenolic epoxy resin YLEP-638, Yolatech (available on request). 7. ASTM D1652, epoxy content of epoxy resins (EEW); ISO 3001, determination of epoxy equivalent. 8. ASTM D1544, Gardner color of transparent liquids; ASTM D445, kinematic viscosity; ASTM E203, water content by Karl Fischer titration.
    Read More
  • Glycidyl Methacrylate GMA: Epoxy Value and Dosage Guide
    Glycidyl Methacrylate GMA: Epoxy Value and Dosage Guide
    Oct 12, 2026
    Glycidyl methacrylate (GMA, CAS 106-91-2) is a difunctional monomer carrying one methacrylate double bond and one glycidyl ester epoxy group per molecule. Its published specification lists purity at 99% minimum, acid value at 0.05 mgKOH/g maximum and water at 0.10% maximum. It ships in closed drums. Figure 1. Glycidyl methacrylate as supplied: a colorless transparent liquid. Product Name: Glycidyl methacrylate Chemical Names: 2,3-Epoxypropyl methacrylate; methacrylic acid 2,3-epoxypropyl ester CAS No.: 106-91-2 Product Category: Functional chemical / reactive monomer 1. Introduction Glycidyl methacrylate (CAS 106-91-2) is unusual among monomers because it carries two independent reactive sites. The methacrylate double bond polymerises by a radical route, and the glycidyl ester ring opens later. That combination places a 142.15 g/mol molecule in powder coating binders, adhesion promoters and polyolefin compatibilisers. Two stages, then: polymerise, then crosslink. Specification values below are quoted from the public Yolatech product page. Constants the page does not publish are marked calculated, and dosage figures are worked examples. 2. Materials and Methods: Product Identification and Specification of Glycidyl Methacrylate The product page publishes four specification items. 2.1 Product Identification and Specification Table 1 merges the identity data with the published specification and adds the derived epoxide equivalent weight. Table 1. Identity and published specification of glycidyl methacrylate (CAS 106-91-2). Item Information Product name Glycidyl methacrylate Chemical names 2,3-Epoxypropyl methacrylate; methacrylic acid 2,3-epoxypropyl ester CAS No. 106-91-2 Molecular formula C7H10O3 (calculated) Molecular weight, g/mol 142.15 (calculated) Reactive groups Methacrylate double bond; glycidyl ester epoxide Appearance Colorless transparent liquid Solubility Insoluble in water; soluble in almost all organic solvents Purity, % 99 minimum Acid value, mgKOH/g 0.05 maximum Water, % 0.10 maximum Epoxide equivalent weight, g/eq 142.15 (calculated from structure) Shelf life, original packing 12 months minimum at ambient temperature Package Drum 2.2 Test Methods and Data Sources Three data classes are kept separate. Appearance, purity, acid value and water content are published values taken as supplied, while molecular formula, molecular weight and epoxide equivalent weight are calculated from the structure of CAS 106-91-2. Epoxide content is titrated according to ASTM D1652 or ISO 3001, and water content is measured according to ASTM E203. Viscosity and flash point are determined by ASTM D445 and ASTM D93. Lot values appear on the batch COA. 3. Results and Discussion: Reactivity of Glycidyl Methacrylate The two reactive sites behave independently, and that independence is the design premise. 3.1 Structure and Reactivity The methacrylate end copolymerises with methyl methacrylate, butyl acrylate or styrene. Methacrylate double bonds propagate more slowly than acrylates, but they also suppress the chain transfer that limits allylic monomers. The glycidyl ester ring survives that radical step, which is what makes the two-stage route possible. Epoxides do not open under ordinary radical conditions, so a binder can be synthesised, isolated, stored and crosslinked later. In practice the ring-opening step uses carboxylic acids, amines, anhydrides or thiols, catalysed by tertiary amines such as DMP-30 or imidazoles. Epoxide equivalent weight of the neat monomer is 142.15 g/eq, calculated from a molecular weight of 142.15 g/mol and one epoxide per molecule. In a copolymer the value scales inversely with the GMA mass fraction, and that arithmetic drives every dosage figure below. 3.2 Comparison with Alternative Mono-Epoxide Monomers Four monofunctional epoxides sit in the same catalogue, and only one of them can be polymerised into a radical backbone. Table 2 compares the published values. Table 2. Glycidyl methacrylate compared with three alternative mono-epoxide monomers (property / this product / alternatives). Property Glycidyl methacrylate (106-91-2) Allyl glycidyl ether YLD-9005 Glycidyl phenyl ether YLD-6001 Butyl glycidyl ether YLD-9004B Second reactive group Methacrylate double bond Allyl double bond None None Radical copolymerisation with acrylics Yes Limited by chain transfer No No Epoxide equivalent weight, g/eq 142.15 calculated 155-285 published Not published 188-205 published Viscosity at 25 °C, mPa·s Not published 1-7 2-8 3 maximum Water, % maximum 0.10 0.10 0.10 0.50 Typical role Reactive monomer for acrylic binders Chain-transfer agent Aromatic reactive diluent Aliphatic reactive diluent The comparison sets the selection rule. Where a reactive diluent has to lower the mixed viscosity of a liquid bisphenol A epoxy resin system, allyl glycidyl ether YLD-9005 and glycidyl phenyl ether YLD-6001 do the job at 1-8 mPa·s. Where the requirement is a polymerisable epoxy, glycidyl methacrylate is the only one of the four that qualifies. 4. Formulation and Dosage Calculation Dosage follows from two equivalent weights. Binder EEW = 142.15 ÷ w, where w is the GMA mass fraction in the copolymer, and crosslinker phr = 100 × AEW ÷ binder EEW, where AEW is the acid equivalent weight of the crosslinker. Dodecanedioic acid has a molecular weight of 230.30 g/mol and two carboxylic groups, so its acid equivalent weight is 115.15 g/eq and its acid value about 487 mgKOH/g. Table 3. Crosslinker dosage for a GMA-acrylic binder with dodecanedioic acid (AEW 115.15 g/eq), calculated. GMA in binder, wt% Binder EEW, g/eq Diacid, phr Comment 15 947.7 12.2 Low epoxide density, softer network 20 710.8 16.2 Highest binder glass transition, lowest flow 25 568.6 20.3 Common powder coating balance 30 473.8 24.3 Higher crosslink density, tighter cure window 35 406.1 28.4 Rarely used; binder softening point drops A 100 kg binder charge at 25 wt% GMA carries 25 kg of glycidyl methacrylate and has an epoxide equivalent weight of 568.6 g/eq. Stoichiometric crosslinking needs 20.3 kg of dodecanedioic acid. Treat the ratio as a starting point. The useful window is normally 0.85 to 1.00 of stoichiometry; a slight acid excess improves flow and adhesion, while excess epoxide favours chemical resistance. When adhesion matters more than solvent resistance, 0.95 to 1.00 is the usual choice. 5. Processing Notes and Operating Window Five process points decide whether a GMA formulation behaves predictably. • Inhibitor management. The monomer carries a phenolic inhibitor at the low hundred ppm level, stated on the current TDS. Radical polymerisation must overcome it, so initiator charge is set from a trial run, not theory. • Radical step window. Acrylic copolymerisation runs at 70-110 °C. If the temperature climbs above that range, or acid or base is present, the epoxide is consumed before the backbone is finished. • Ring-opening cure. Powder coating binders cure at 160-200 °C for 15-30 minutes. Amine or imidazole catalysis lowers the peak, but it also shortens melt pot life. • Moisture control. Water above specification hydrolyses the glycidyl ester. Open containers and damp fillers pull the acid value out of range. • Storage. Keep containers closed in a well-ventilated area away from flames and direct sunlight, and seal the cap immediately after use. Figure 2. Electrostatic powder application, the step that precedes the ring-opening cure. 6. Applications The monomer earns its place in five areas, and the loading differs by an order of magnitude between them. Table 4. Main applications of glycidyl methacrylate and typical loadings. Application Function of glycidyl methacrylate Typical loading Powder coating binders Epoxide reacts with a diacid during oven cure 20-30 wt% of binder Adhesion promoters and primers Bonds to substrate hydroxyls and to the binder 1-5 wt% on binder Polyolefin compatibilisers Grafted onto a polyolefin backbone to couple with polar fillers 3-8 phr in the compound Waterborne acrylic emulsions Crosslinking monomer for self-crosslinking lattices 1-4 wt% on monomer Polymer synthesis intermediate Building block for epoxy-functional polymers Formulation specific Powder coatings are the largest outlet, because a GMA-acrylic binder crosslinked with a diacid weathers outdoors without the halogenated or amine hardeners older systems used. Accelerator choice for that chemistry is covered in the note on curing additives for epoxy powder coatings. In adhesives the monomer works as a coupling agent rather than a bulk component; a few parts in a primer improve wet adhesion to steel and aluminium, a mechanism described for epoxy resin adhesives. The same polarity shift lets a grafted polyolefin bond glass fibre in fibre-reinforced composites. Figure 3. Glass fibre reinforced pellets, a typical end use for a grafted polyolefin compatibiliser. 7. Limitations and Material Verification 7.1 Known Limitations and Non-Applicable Uses The epoxide on glycidyl methacrylate is monofunctional, so the monomer cannot build a crosslinked epoxy network on its own. It is not a substitute for a liquid epoxy resin and not a curing agent. Where bulk viscosity reduction is the goal, a monofunctional glycidyl ether such as butyl glycidyl ether YLD-9004 is the route, because the methacrylate double bond contributes nothing to that chemistry. Homopolymerisation gives a linear epoxy-functional acrylic, not a network, and crosslinking needs a separate partner. Water is the second limitation: the glycidyl ester hydrolyses to a glycol with acid catalysis, so an ageing drum loses epoxide content, and a wet filler does the same inside a formulation. Handling is the third. The material is a skin and eye irritant and a skin sensitiser, and bulk radical polymerisation carries a runaway risk when initiator charge and cooling are mismatched. 7.2 Incoming Inspection, Packaging, Storage and Safety Four checks cover most incoming lots: appearance, purity, acid value and water content. Acid value is the fastest hydrolysis indicator and the cheapest test, so it stands in for a full epoxide titration on routine receipts. Run epoxide content according to ASTM D1652 on a new supplier or after long storage. Check with the supplier before assuming a drum is still in specification. Packaging is a drum, and shelf life is at least 12 months from the date of manufacture in the original packing at ambient temperatures. That clock holds only while the drum stays closed. RoHS, REACH and UL 94 statements are for the customer to verify against current documentation rather than infer from a product description. Batch compliance data and safety information appear in the MSDS, TDS and COA for glycidyl methacrylate. 8. Frequently Asked Questions Is glycidyl methacrylate a resin or a curing agent? Neither. Glycidyl methacrylate is a functional monomer with a molecular weight of 142.15 g/mol, copolymerised into a binder or grafted onto a polymer backbone. What is the epoxy equivalent weight of glycidyl methacrylate? The calculated value is 142.15 g/eq. A copolymer containing 25 wt% glycidyl methacrylate therefore has a binder epoxide equivalent weight of 568.6 g/eq. Why is the acid value limited to 0.05 mgKOH/g maximum? Acid value tracks hydrolysis. The glycidyl ester reacts with water to form a glycol and methacrylic acid, and the acid catalyses further hydrolysis, so a rising acid value signals moisture pickup. Does the epoxy group survive free-radical polymerisation? Yes, within the operating window. Epoxides do not open under radical conditions, so the ring survives copolymerisation at 70-110 °C. It is consumed only if water, acids or bases are present. How much dodecanedioic acid does a GMA-acrylic binder need? At 25 wt% glycidyl methacrylate the stoichiometric charge is 20.3 phr of dodecanedioic acid, assuming an acid equivalent weight of 115.15 g/eq. Commercial formulations usually run between 0.85 and 1.00 of that figure. Can glycidyl methacrylate replace a reactive diluent such as YLD-9004? Not for the purpose of reducing viscosity. Butyl glycidyl ether YLD-9004 is a dedicated reactive diluent with a published epoxide equivalent weight of 188-205 g/eq. 9. Conclusions Two reactive sites on one 142.15 g/mol molecule are the whole value proposition of glycidyl methacrylate (CAS 106-91-2). The published specification is short and focused on hydrolysis control: purity at 99% minimum, acid value at 0.05 mgKOH/g maximum and water at 0.10% maximum. The dosage follows from two equivalent weights. A binder at 25 wt% glycidyl methacrylate has an epoxide equivalent weight of 568.6 g/eq and takes 20.3 phr of dodecanedioic acid at stoichiometry. The material is a monomer and an adhesion promoter, not a resin or a hardener. 10. References 1. Yolatech product page: https://www.yolatech.com/glycidyl-methacrylate-cas-106-91-2 (accessed 2026-10-12). 2. Yolatech Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for glycidyl methacrylate CAS 106-91-2 (available on request). 3. ASTM D1652, epoxy content of epoxy resins (EEW). 4. ISO 3001, determination of epoxy equivalent. 5. ASTM E203, water content by Karl Fischer titration. 6. ASTM D445, kinematic viscosity. 7. ASTM D93, flash point, Pensky-Martens closed cup. 8. Yolatech product page: https://www.yolatech.com/allyl-glycidyl-ether-yld-9005 (accessed 2026-10-12). 9. Yolatech product page: https://www.yolatech.com/butyl-glycidyl-etherbge-yld-9004 (accessed 2026-10-12).
    Read More
  • DMTDA Chain Extender: Stoichiometric Dosage and Blend Ratios
    DMTDA Chain Extender: Stoichiometric Dosage and Blend Ratios
    Oct 10, 2026
    DMTDA, dimethyl thio-toluene diamine (CAS 106264-79-3), is a liquid aromatic diamine used as a polyurethane chain extender and epoxy curing agent. Its published specification lists diamines at 95% minimum, water at 0.10% maximum and amine value 515-535 mg KOH/g. Epoxy equivalent weight is 53.6 g/eq. Figure 1. DMTDA as supplied: a light yellow liquid in a glass sample bottle. Product Code: DMTDA Chemical Name: Dimethyl thio-toluene diamine CAS No.: 106264-79-3 Product Category: Aromatic diamine chain extender and epoxy curing agent 1. Introduction DMTDA (CAS 106264-79-3) is a room-temperature liquid aromatic diamine that removes the melt step solid curatives require. Cast polyurethane elastomers and polyurea coatings use aromatic diamines because the rigid ring lifts hardness, modulus and heat resistance above what a polyether amine reaches. The price is reactivity. The published specification is short: appearance, diamine content, toluenediamine (TDA) content, water and amine value. Everything else, from equivalent weight to blend ratio, has to be derived. All numbers come from the public product page. Constants it does not publish are marked calculated, and dosage figures are worked examples. 2. Materials and Methods: DMTDA Identification and Specification The product page publishes five specification items, and DMTDA ships as one liquid grade in drums. 2.1 Product Identification and Specification Table 1 collects the identification data used here, and Table 2 reproduces the published specification. Table 1. Identification data of DMTDA (CAS 106264-79-3). Item Information Product name DMTDA Chemical name Dimethyl thio-toluene diamine CAS No. 106264-79-3 Molecular formula C9H14N2S2 (calculated) Molecular mass 214.3 g/mol (calculated) Amine functionality two primary amines, four active hydrogens Table 2. Published specification of DMTDA, taken from the product page. Item Specification Appearance Light yellow viscous liquid Diamine content 95% minimum TDA content 1.00% maximum Water content 0.10% maximum Amine value 515-535 mg KOH/g 2.2 Test Methods and Data Sources Five items carry published values and the rest are calculated. Appearance is judged visually. Water is determined by Karl Fischer titration according to ASTM E203, and the amine value is obtained by titration and reported in mg KOH/g. The molecular formula and molecular mass are not printed on the product page, so both are calculated and should be confirmed against the current certificate of analysis. Two columns in the later tables are computed rather than measured: amine hydrogen equivalent weight, and the hardener demand that follows. 3. Results and Discussion Reaction with isocyanate is slow for DMTDA, and the reason sits in two methylthio groups. 3.1 Structure and Reactivity of DMTDA Each molecule carries two primary amine groups on a toluene ring, with one methylthio group (–S–CH3) beside each nitrogen. Those sulfur groups are bulky and electron-donating, so the nitrogen lone pair is shielded and the rate of attack on an isocyanate falls. Ring rigidity then raises hardness, modulus and heat resistance in the cured network. The product page states the consequence: the reaction rate with isocyanate is lower than that of DETDA. A slow reaction is not a defect everywhere. In a large casting it extends the pour window; in a small, fast-demould part it costs productivity. The published amine value of 515-535 mg KOH/g is consistent with the calculated mass of 214.3 g/mol. 3.2 Comparison with Alternative Amine Systems Several amine families compete for the same work, and in practice the choice turns on physical state, equivalent weight and reaction rate rather than price per kilogram. DETDA is the closest relative: same diaminotoluene core, also a liquid, and the same polyurea and cast elastomer applications. Its published amine value of 625-640 mg KOH/g is higher, so it carries more amine groups per kilogram and a lower equivalent weight. Less mass is needed per equivalent and the reaction runs faster; DMTDA runs longer, so the two are often blended to set gel time. Alicyclic amines sit at the fast end. 1,2-diaminocyclohexane DACH carries a published AHEW of 28.5 g/eq, roughly double the amine density of DMTDA. m-xylylenediamine MXDA and 1,3-cyclohexanebis(methylamine) are aromatic in character but aliphatic in behaviour. Table 3. DMTDA against alternative amine hardeners, at published and calculated values. Property DMTDA DETDA DACH MXDA 1,3-BAC CAS No. 106264-79-3 68479-98-1 694-83-7 1477-55-0 2579-20-6 Amine value, mg KOH/g 515-535 625-640 900 minimum not published not published Water content, maximum 0.10% 0.10% 0.30% 0.50% 0.30% AHEW, g/eq 53.6 calculated 44.6 calculated 28.5 published 34.1 calculated 35.6 calculated Hardener for EEW 187, phr 28.7 23.8 15.2 18.2 19.0 Read the last row as a cost line. For 100 g of resin, DMTDA needs 28.7 phr, DETDA 23.8 phr and DACH only 15.2 phr, so price per kilogram says little about mix cost. 4. Formulation and Dosage Calculation Hardener demand in an epoxy system comes from one relation: phr = 100 × AHEW ÷ EEW. Four active hydrogens on a molecular mass of 214.3 g/mol give DMTDA an AHEW of 214.3 ÷ 4 = 53.6 g/eq. Table 4. Theoretical DMTDA demand for common liquid epoxy resins. Epoxy resin, published EEW EEW, g/eq DMTDA, phr DETDA, phr Liquid bisphenol A resin YLE-127 176-184 30.5-29.1 25.3-24.2 Liquid bisphenol A resin YLE-128 184-190 29.1-28.2 24.2-23.5 Liquid bisphenol A resin YLE-121 170-176 31.5-30.5 26.2-25.3 Phenolic epoxy resin YLEP-638 170-190 31.5-28.2 26.2-23.5 The resin EEW values come from the liquid bisphenol A epoxy resin grades and the YLEP-638 multifunctional epoxy resin page. Recalculate from the batch EEW. Chain extension is counted differently. The equivalent weight against isocyanate is taken per amine group, so it is 214.3 ÷ 2 = 107 g/eq, calculated. Table 5. Worked chain-extender demand for a cast polyurethane formulation. Parameter Value Prepolymer NCO content 8.0% Isocyanate equivalent weight 525 g/eq NCO equivalents in 100 g prepolymer 0.190 Curative equivalent weight, calculated 107 g/eq Curative at 100% index 20.4 g Index is the lever. A 95% index leaves unreacted isocyanate and a softer part; above 100% the isocyanate is consumed, but unreacted amine can plasticise the elastomer. The right index depends on the hardness target, so verify it on a trial casting. Blending is the second lever. Because DMTDA can be used together with DETDA, the ratio sets both working time and hardness. Start from the equivalent-weight average, then adjust on a gel-time trial. 5. Processing Notes and Operating Window Ambient-temperature liquid means DMTDA can be pumped and metered without a melt tank. Handling rules follow. • Keep the drum closed between uses. Amines take up moisture and carbon dioxide from air, and an open drum drifts past the 0.10% water limit. • Do not heat the drum unless the shop is cold. There is no melting step to justify it, and heat accelerates oxidation. • Watch the blend, not just the two components. If DETDA is added for speed, gel time falls faster than the equivalent-weight average predicts. • Wear nitrile gloves, goggles and a coverall. Aromatic diamines are skin sensitisers, and the safety data sheet carries the PPE list. Figure 2. Metering DMTDA into a polyurethane prepolymer before casting. 6. Applications The product page names three directions: a chain extender and curing agent for polyurethane and polyurea systems, an epoxy curing agent, and an industrial lubricant. Table 6. Application areas for DMTDA and the formulation note for each. Application Role Formulation note Cast polyurethane elastomers chain extender room-temperature or hot casting with an MDI prepolymer Polyurea spraying systems chain extender the slower reaction widens the spray window Other polyurethane products chain extender often blended with DETDA to set demould time Epoxy casting and coatings curing agent requires heat; dosage from the AHEW relation Industrial lubricants functional additive listed on the product page, with no dosage given Figure 3. Polyurea floor coating applied over concrete, a typical end use for DMTDA chain extension. 7. Limitations and Material Verification Three situations call for an amine other than DMTDA. 7.1 Known Limitations and Unsuitable Uses Room-temperature epoxy cure is the first limit. An aromatic amine needs heat for full conversion, so a casting left at 20 °C stays soft in the core. Without an oven cycle or an accelerator, an alicyclic amine such as DACH is the better starting point. Colour is the second, and it matters when the finish is white or light grey. Aromatic amines oxidise in air, so a non-yellowing coating is the wrong place for DMTDA. The third is dosage mass. The high equivalent weight means more hardener mass per kilogram of resin than DETDA or DACH needs. That is a freight cost, not a performance penalty, so quote it per equivalent. 7.2 Incoming Inspection, Packaging, Storage and Safety Four checks catch most incoming-lot problems: appearance against the light yellow reference, water by Karl Fischer titration according to ASTM E203, amine value by titration, and diamine content by the certificate of analysis (COA) method. Run the water check in duplicate on the first drum of each delivery. Drum packaging is standard. Store in a well-ventilated area away from flames and direct sunlight, keep the cap closed after use, and expect a shelf life of at least 12 months from manufacture in the original packing. Safety data sit in the material safety data sheet. Treat the liquid as an irritant and a skin sensitiser, and read the sheet before the first drum is opened. 8. Frequently Asked Questions What is the equivalent weight of DMTDA? For epoxy formulation the amine hydrogen equivalent weight is 53.6 g/eq, calculated as 214.3 g/mol divided by four active hydrogens. For isocyanate chain extension it is taken per amine group and equals 107 g/eq. Confirm both against the current certificate of analysis. How much DMTDA does 100 g of epoxy resin need? For a liquid bisphenol A resin of EEW 187 the theoretical dosage is 100 × 53.6 ÷ 187 = 28.7 phr. The figure moves with the resin: EEW 173 gives 31.0 phr and EEW 250 gives 21.4 phr. Does DMTDA react faster or slower than DETDA with isocyanate? Slower. The product page states that the reaction rate with isocyanate is lower than that of DETDA, which is why DMTDA is described as a slower chain extender. A blend of the two lets a formulator set demould time without changing the stoichiometry. Can DMTDA be processed at room temperature? Handling and metering need no heat, because DMTDA is a liquid at ambient temperature and room-temperature casting of polyurethane elastomers is an established use. Room-temperature epoxy cure is different: an aromatic amine needs heat for full conversion. What is the shelf life and how should DMTDA be stored? At least 12 months from the date of manufacture in the original packing at ambient temperature, according to the product page. Keep the drum closed, in a well-ventilated area away from flames and direct sunlight. A part-used drum left open can fail the 0.10% water limit. Can DMTDA replace a solid aromatic diamine curative? In many cast polyurethane and polyurea systems it can, because a liquid curative removes the melt and hold-temperature steps a solid one requires. It is not a drop-in replacement everywhere: the equivalent weight is higher, so the dosage changes, and the cured colour is darker. 9. Conclusions DMTDA is a liquid aromatic diamine whose published specification covers appearance, diamine content, TDA content, water and amine value, with a calculated amine hydrogen equivalent weight of 53.6 g/eq. Its place in a formulation rests on a pumpable liquid at room temperature, an isocyanate reaction slower than that of DETDA, and the stiffness the aromatic ring gives the cured network. Dosage follows two relations. For epoxy, phr = 100 × AHEW ÷ EEW gives 28.7 phr against a resin of EEW 187. For chain extension, the equivalent weight of 107 g/eq per amine group gives 20.4 g per 100 g of an 8% NCO prepolymer at a 100% index. 10. References 1. Yolatech product page: https://www.yolatech.com/dimethyl-thio-toluene-diamine-dmtda-cas-106264-79-3 (accessed 2026-10-10). 2. Yolatech Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for DMTDA, CAS 106264-79-3 (available on request). 3. ASTM E203, water content by Karl Fischer titration. 4. ASTM D1652, epoxy content of epoxy resins (EEW). 5. ISO 3001, determination of epoxy equivalent. 6. ISO 9702, amine group nitrogen content of amine epoxide hardeners.
    Read More
  • YLSE-186 Epoxy Resin: Trifunctional Low-Viscosity Grade
    YLSE-186 Epoxy Resin: Trifunctional Low-Viscosity Grade
    Oct 10, 2026
    YLSE-186 epoxy resin is a trifunctional alicyclic epoxy resin, CAS 25293-64-5, that carries one cycloaliphatic epoxide and two glycidyl ester groups on a ring. Its published EEW is 100-111 g/eq at 2000-4000 cps, close to a quarter of liquid bisphenol A viscosity, so it wets fibres without a diluent. Figure 1. YLSE-186 epoxy resin as supplied: a pale straw liquid. Product Code: YLSE-186 / YLSE-186C Chemical Name: 4,5-Epoxytetrahydrophthalic acid diglycidylester CAS No.: 25293-64-5 Product Category: Trifunctional alicyclic epoxy resin 1. Introduction Solvent-free composite work sets two demands against each other. A resin must wet a dry fibre tow easily, yet cure into a stiff matrix. YLSE-186 epoxy resin (CAS 25293-64-5) sits in that gap. All data below come from the public product page for 4,5-epoxytetrahydrophthalic acid diglycidylester. Where the page is silent, figures are marked literature or calculated, and every dosage number can be recomputed. 2. Materials and Methods YLSE-186 ships as a clear to pale yellow liquid in drums, in two commercial grades. Only six parameters are published, so the tables separate measured values from structural inference. 2.1 Product Identification and Specification Table 1 lists the identification data used in this paper, and Table 2 the published specification for both grades. Nothing outside those items is a quality claim. Table 1. Identification data of YLSE-186 epoxy resin (CAS 25293-64-5). Item Information Product Code YLSE-186 (high purity) and YLSE-186C (economy grade) Chemical Name 4,5-Epoxytetrahydrophthalic acid diglycidylester CAS No. 25293-64-5 Epoxy groups per molecule 3: one alicyclic epoxide plus two glycidyl ester groups Appearance Colorless to light yellow liquid, light yellow for YLSE-186C Table 2. Published specification of the two YLSE-186 grades. Item YLSE-186C YLSE-186 Appearance Light yellow liquid Colorless to light yellow liquid Color, Gardner Max. 2 Max. 2 Viscosity, cps at 25 °C 3000-6000 2000-4000 Epoxy equivalent weight, g/eq 100-125 100-111 Volatiles, % Max. 1 Max. 1 Positioning Lower price High purity 2.2 Test Methods and Data Sources Values marked published come from the YLSE-186 product page. Epoxy equivalent weight is determined by titration according to ASTM D1652 or ISO 3001, viscosity is measured at 25 °C, and color according to ASTM D1544. Molecular mass and theoretical EEW are calculated from the structure (Table 3). Table 3. Constants calculated from the YLSE-186 structure. Property Value Basis Molecular formula C14H18O7 Structure Molar mass About 298 g/mol From formula Theoretical EEW About 99 g/eq 298 ÷ 3 Epoxy equivalents per tonne About 10,100 eq At EEW 99 3. Results and Discussion: YLSE-186 Epoxy Resin Reactivity One alicyclic epoxide and two glycidyl ester groups sit on the same cyclohexane ring, and the three sites do not react at the same rate. 3.1 Structure and Reactivity The glycidyl ester groups open faster than the alicyclic ring, and the published description states that reactivity exceeds general alicyclic epoxy resin. Anhydride systems show the split first: ester groups react early, the ring follows at higher temperature. Three sites on one small molecule also give a denser network than a difunctional ester. The theoretical EEW of about 99 g/eq in Table 3 sits just below the published window of 100-111 g/eq, consistent with a small hydrolysis and volatile fraction. Capacity per tonne decides mix economics: at EEW 100 the resin carries about 10,000 equivalents against 5,300 for a bisphenol A resin at EEW 184-190. 3.2 Comparison with Alternative Systems Table 4 compares YLSE-186 epoxy resin with the grades most often quoted against it. Three families compete for this work: difunctional cycloaliphatic esters, trifunctional glycidylamines, and bisphenol A liquids. Table 4. YLSE-186 against alternative epoxy systems, at published values. Property YLSE-186, this grade Alternative grades, published data Epoxy groups per molecule 3: one alicyclic epoxide, two glycidyl ester groups YLCE-2021 cycloaliphatic epoxy resin: 2. YLSE-0600 trifunctional glycidylamine resin: 3. YLSE-721 tetrafunctional epoxy resin: 4 EEW, g/eq 100-111; 100-125 for YLSE-186C YLCE-2021: 126-132. YLSE-0600: 102-110. YLSE-721: 105-120. Liquid bisphenol A epoxy resin YLE-128: 184-190 Viscosity at 25 °C 2000-4000 cps; 3000-6000 cps for YLSE-186C YLCE-2021: 220-250 mPa·s. YLSE-0600: 7000-20000 cps. YLSE-721: 3000-7000 cps at 50 °C. YLE-128: 11000-15000 mPa·s Typical role Solvent-free composite matrix, adhesive base YLCE-2021: thin impregnation. YLSE-0600, YLSE-721: high-crosslink laminating. YLE-128: general purpose. YLEP-638 novolac epoxy resin: hot chemical resistance Read the viscosity column first. YLCE-2021 flows at 220-250 mPa·s, an order of magnitude thinner than YLSE-186, but with only two epoxy groups. Hardener cost is the trade-off buyers miss. Doubling the epoxy equivalents per tonne roughly doubles the amine bought, so a cheap high-functionality grade can lose on mix cost. Price the mix, not the drum. 4. Formulation and Dosage Calculation Amine-cured mixes follow phr = 100 × AHEW ÷ EEW. With YLSE-186 in the 100-111 g/eq window, a hardener of AHEW 96 g/eq is needed at roughly 90 phr, close to double the 50 phr the same hardener asks against a bisphenol A liquid. Table 5. Theoretical hardener demand for an amine of AHEW 96 g/eq. Resin grade, published EEW EEW, g/eq Theoretical hardener, phr YLSE-186 100-111 96.0-86.5 YLSE-186C 100-125 96.0-76.8 Liquid bisphenol A resin YLE-127 176-184 54.5-52.2 Liquid bisphenol A resin YLE-128 184-190 52.2-50.5 The formula is worth checking against published hardener data: YLH-6004 modified amine hardener lists AHEW 96 g/eq and an added weight of 50 phr against a resin of EEW 190, and 100 × 96 ÷ 190 = 50.5. The trap is that 50 phr line. At 50 phr against YLSE-186 you are near half the stoichiometric hardener, so the skin sets hard while the core stays soft. Recalculate from the batch EEW, then confirm with a gel-time check. Anhydride stoichiometry uses a different number: phr = 100 × anhydride equivalent weight ÷ EEW. For a mono-anhydride such as MHHPA anhydride hardener the equivalent weight is about 168 g/eq (calculated), so full stoichiometry at EEW 100 is 168 phr, and most shops run 85-90% of that near 143-151 phr. Viscosity gives one more lever. If 2000 cps is too thick for the mould, blend rather than heat: a glycidyl ester diluent such as YLD-9012 glycidyl ester diluent at 600-1200 mPa·s thins the mix and stays reactive. 5. Processing Notes and Operating Window Three epoxy groups per molecule release more heat per kilogram than a difunctional resin, and the low viscosity moves that heat faster. Exotherm is the first variable to control. • Keep trial mixes near 100 g in a wide container. The same mix in a full pail can gel in a fraction of the time. • Store sealed below 4 °C, and let a cold drum reach room temperature before opening. Condensation goes straight into the resin. • Work in dry air. Alicyclic epoxides hydrolyse slowly, and a humid shop shows up later as a drifting EEW rather than an obvious defect. • De-gas the mixed resin before cure. At 2000-4000 cps it still traps air, and voids in a wound part are expensive to fix. • Wear nitrile gloves, goggles and a coverall. Epoxy resins are skin sensitisers, and the MSDS carries the PPE list. Figure 2. Wet-out of carbon fibre tow in a YLSE-186 resin bath. 6. Applications The product page names two application directions: carbon fibre composites such as high-pressure gas bottles and motor rotors, and high-temperature adhesives. Table 6 sets out what each asks of the resin. Table 6. Application areas for YLSE-186 and the constraint in each. Application What YLSE-186 contributes Where the constraint sits Filament-wound pressure vessels Thin bath for fibre wet-out, more crosslink density per tonne Warm or oven cure; voids if the bath is not de-gassed Motor rotors and rotating parts Stiff matrix with strong fibre binding at a manageable mass Exotherm has to be controlled on thick sections High-temperature adhesives Three reactive sites and a low-viscosity base that accepts fillers Color is loose on YLSE-186C, so use the base grade for visible bond lines Two application lines on a product page are a starting point, not a scope limit. If the part runs through an anhydride bath and needs a stiff matrix, this grade fits; for a cheap filled casting it does not. Figure 3. Filament-wound pressure vessel wound with YLSE-186 epoxy resin. 7. Limitations and Material Verification Two areas limit how YLSE-186 epoxy resin can be specified: the published data set, and the storage behaviour of an alicyclic epoxide. 7.1 Known Limitations The specification covers appearance, color, viscosity, EEW, volatiles and positioning only. Density, flash point, chlorine content, gel time and a titration epoxy value are not on the page, so any dosage plan stays theoretical until a batch COA confirms it, and large neat castings sit outside the grade. 7.2 Incoming Material Verification, Packaging and Safety Drum-to-drum variation exists on any epoxy line, so incoming checks on viscosity, EEW and volatiles are recommended for every lot. Water content is determined by Karl Fischer titration where a lot is disputed, and color is measured according to ASTM D1544. Supply is by drum package, and the page carries two storage statements that do not agree: sealed storage below 4 °C with a shelf life of about six months, and 24 months in original packing. Two numbers that far apart usually describe different conditions, so take the shorter one. Alicyclic epoxides hydrolyse slowly in warm, damp storage: keep drums sealed, use opened drums first, and take hazard information from the Material Safety Data Sheet. 8. Frequently Asked Questions What is the published EEW of YLSE-186 epoxy resin? YLSE-186 is published at 100-111 g/eq and YLSE-186C at 100-125 g/eq. The structure gives a theoretical 99 g/eq, so the window fits a three-functional molecule. Verify the batch value by titration before fixing a ratio. How much hardener does YLSE-186 epoxy resin need per 100 parts of resin? For an amine hardener, phr = 100 × AHEW ÷ EEW. A hardener of AHEW 96 g/eq such as YLH-6004 needs 96.0 phr at EEW 100 and 86.5 phr at EEW 111. Filler load and temperature move the ratio. Can YLSE-186 epoxy resin be cured at room temperature? It can, but slowly. The published description allows amines as a cure route, and the two glycidyl ester groups are the reactive part. Cycloaliphatic epoxies cure slowly with amines in general, so a 15-20 °C workshop cure needs time or a warm post-cure. What is the difference between YLSE-186 and YLSE-186C? Both are the same molecule at the same color ceiling, and the page separates them on price and purity. YLSE-186C has a wider EEW window of 100-125 g/eq and a light yellow tone; YLSE-186 is the high-purity grade at 100-111 g/eq. Can YLSE-186 epoxy resin replace a standard cycloaliphatic epoxy resin? Not as a straight swap. YLCE-2021 carries two epoxy groups at EEW 126-132 g/eq and flows at 220-250 mPa·s, so a substitution changes the hardener ratio and the bath viscosity. YLSE-186 raises crosslink density and roughly doubles the amine charge. Why is YLSE-186 epoxy resin stored below 4 °C? The page instructs storage below 4 °C with a sealed shelf life of half a year, and also repeats the standard line of 24 months in original packing. Plan around the shorter figure: cold storage slows the hydrolysis and color drift of alicyclic epoxides. 9. Conclusions This trifunctional alicyclic epoxy (CAS 25293-64-5) pairs a published EEW of 100-111 g/eq with a viscosity of 2000-4000 cps, so it wets fibre without a diluent and still cures to a high crosslink density. Its practical roles are a solvent-free composite matrix and a base for high-temperature adhesives. Its limits are the thin published data set, a hardener demand near 90 phr with an amine, and a cold, sealed storage requirement. Numbers above are published values or figures marked calculated and literature, and the current TDS / MSDS / COA governs the specification. Grade availability for YLSE-186 epoxy resin is confirmed against a target EEW. 10. References • Yolatech product page, 4,5-Epoxytetrahydrophthalic acid diglycidylester YLSE-186: https://www.yolatech.com/45-epoxytetrahydrophthalic-acid-diglycidylester-ylse-186-cas-25293-64-5 (accessed 2026-10-09). • Yolatech Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for YLSE-186, CAS 25293-64-5 (available on request). • ASTM D1652, epoxy content of epoxy resins (EEW). • ISO 3001, determination of epoxy equivalent. • ASTM D445, kinematic viscosity. • ASTM D1544, Gardner color of transparent liquids.
    Read More
  • DMAPA Curing Agent: Dosage, Pot Life and Blush Control
    DMAPA Curing Agent: Dosage, Pot Life and Blush Control
    Oct 09, 2026
    DMAPA curing agent is a colourless primary amine, N,N-Dimethyl-1,3-propanediamine (CAS 109-55-7), that also carries a tertiary nitrogen. Its theoretical AHEW is 51.1 g/eq, so a liquid bisphenol A resin of EEW 190 needs about 27 phr, and this stoichiometry is where most dosage errors begin at mixing. Figure 1. DMAPA as supplied: a water-clear, mobile liquid. Product Code: DMAPA Chemical Name: N,N-Dimethyl-1,3-propanediamine CAS No.: 109-55-7 Product Category: Amine curing agent / functional chemical 1. Introduction Ambient-cure epoxy systems need an amine hardener fast enough for hand-applied coatings yet slow enough to be mixed in a pail, and DMAPA (CAS 109-55-7) sits at the fast end of that range. The data reported here come from the public product page for N,N-Dimethyl-1,3-propanediamine and its published specification. Values the page omits are labelled literature or theoretical. 2. Materials and Methods: DMAPA Curing Agent Grade Data DMAPA is supplied as a colorless liquid in drum packages with a published purity of min. 99.5% and a water limit of max. 0.30%. Only four items are published, so the data below separate published values from structural inference. 2.1 Product Identification and Specification Table 1 lists the identification data used throughout this paper. Table 2 gives the four published specification items; nothing outside it is a quality claim. Table 1. Identification data of DMAPA (CAS 109-55-7). Item Information Product Code DMAPA Chemical Name N,N-Dimethyl-1,3-propanediamine CAS No. 109-55-7 Molecular Formula C5H14N2 (literature) Molecular Weight 102.18 g/mol (literature) Active Hydrogens 2, primary amine only Table 2. Published specification of DMAPA. Item Specification Appearance Colorless liquid Color, APHA Max. 20 Purity Min. 99.5% Water Max. 0.30% 2.2 Test Methods and Data Sources Values marked published come directly from the DMAPA product page. Boiling point, flash point, density and viscosity appear in Table 3 as literature values for CAS 109-55-7 rather than specification limits. Water content is determined by Karl Fischer titration and color is measured according to the APHA scale. Table 3. Physicochemical properties of DMAPA; literature and theoretical values for CAS 109-55-7. Property Typical value Basis Boiling point 132-140 °C at 1013 hPa Literature Flash point About 32 °C, closed cup Literature; ISO 3679 Density About 0.82 g/cm³ at 20 °C Literature Viscosity About 1.2-1.6 mPa·s at 20 °C Literature; ASTM D445 Amine value Not published; about 1098 mg KOH/g theoretical Theoretical; ISO 9702 AHEW 51.1 g/eq theoretical 102.18 ÷ 2 3. Results and Discussion: DMAPA Curing Agent Reactivity DMAPA carries a primary amine and a tertiary amine on one three-carbon chain, and the two nitrogens do different jobs in an epoxy cure. 3.1 Structural Basis of Reactivity The primary amine carries the two active hydrogens, so it alone sets the stoichiometry: 102.18 g/mol divided by two gives a theoretical AHEW of 51.1 g/eq. The tertiary nitrogen has no N-H hydrogen, so it contributes no crosslink and only catalyses the epoxy-hydroxyl reaction, shortening gel time. A short chain with two reactive nitrogens gives a fast, tightly crosslinked and hydrophilic network, so a slow, low-blush room-temperature system is not a realistic target for neat DMAPA. 3.2 Comparison with Alternative Curing Systems Table 4 compares DMAPA with the amine hardeners most often quoted against it, using published figures where a product page states them. Table 4. DMAPA against common amine curing agents, at published or theoretical values. Property DMAPA Common alternatives Active hydrogens / AHEW 2; 51.1 g/eq theoretical DETA 20.6 g/eq; MACM 60 g/eq; YLH-3101 110 g/eq, published Viscosity, published Not published; about 1-2 mPa·s at 20 °C MACM 80-120 mPa·s; YLH-3101 300-1000 cps at 25 °C Water miscibility Miscible MACM insoluble; MXDA soluble; polyetheramine D-230 slightly soluble Blush tendency in humid cure High Lower for water-insoluble amines such as MACM Typical role Co-hardener, accelerator, amidoamine building block DETA, MXDA primary hardeners; MACM high-performance; YLH-3101 modified ready-to-use Color stability of stock Darkens in air once opened DACH also yellows in air; modified grades hold color better For a neat room-temperature coating, DMAPA alone is rarely the right answer. The defensible placement is three roles: an amidoamine building block condensed with fatty or dimer acids, a reactivity booster alongside slower polyetheramines, and a small-dose accelerator where DMP-30 is not wanted. Rigid diamines are another route. 1,3-BAC and MACM trade higher viscosity for water resistance and strength, and N4-AMINE adds a fourth reactive nitrogen for higher crosslink density. If toughness matters more than speed, a polyamide such as YLH-5101 usually out-cures DMAPA on film properties. 4. Formulation and Dosage Calculation Dosage follows the standard amine rule, phr = 100 × AHEW ÷ EEW, which for DMAPA reduces to 100 × 51.1 ÷ EEW because only the two hydrogens on the primary amine count. Table 5. Theoretical DMAPA dosage against published resin EEW values. Resin grade (published EEW) EEW, g/eq Theoretical DMAPA, phr Liquid bisphenol A epoxy resin YLE-128 184-190 26.9-27.8 Liquid bisphenol A epoxy resin YLE-127 176-184 27.8-29.0 Bisphenol F epoxy resin YLE-170 165-175 29.2-31.0 Low-viscosity bisphenol A epoxy resin YLE-121 170-176 29.0-30.1 The error worth guarding against sits in the other nitrogen. If the tertiary amine is counted as active, the same calculation returns 34.1 g/eq and about 18 phr, and the batch gels on top while the underlayer stays soft. Whenever a mix cures unevenly, that arithmetic is the first thing to re-check. A cross-check comes from the same hardener range. YLH-6004 lists AHEW 96 g/eq at 50 phr, and YLH-3101 lists 110 g/eq at 55-60 phr, both against a resin of EEW 190. Treat every value above as a starting point. The working ratio depends on filler loading, resin purity and ambient temperature, and in practice it is confirmed by a gel-time check and a thin-film cure test on about 100 g. 5. Processing Notes and Operating Window Exotherm is the first variable to control: a loading near 27 phr against an EEW 190 resin releases a large amount of heat in a small mass, and the temperature spike shortens working time further. • Keep trial mixes at about 100 g in wide containers; the same mix in a 1 kg pail can gel in a fraction of the time. • Mix cool and post-cure warm. If the film blushes, raise the cure temperature rather than adding more amine. • Watch humidity. Blush forms fastest in cold, damp shops, so schedule amine-cured work away from the wettest part of the day. • Ventilate locally. Keep the drum closed and draw through a pump instead of pouring from an open bung. • Wear nitrile gloves, splash goggles and protective clothing; DMAPA is corrosive and a skin sensitiser, and the MSDS carries the PPE list. • Verify water content on opened drums. Moisture above the 0.30% limit shows up as haze long before a routine COA catches it. Figure 2. Decanting DMAPA under local exhaust ventilation. 6. Applications The product page lists six application directions for DMAPA: cosmetic raw materials, dyestuffs, ion exchange resins, epoxy resin curing agent, non-cyanide electroplating additive, and fibre and leather treatment agent. Table 6 separates the epoxy role from the intermediate roles. Table 6. Application areas for DMAPA and its role in each. Application area Role of DMAPA Practical note Epoxy resin curing Reactive hardener and accelerator About 27 phr against EEW 190 resin; watch blush and exotherm Amidoamine hardeners Amine building block Condensed with fatty or dimer acids Ion exchange resins Amine functionalisation intermediate Amine source for polymer backbones Cosmetic raw materials Intermediate for betaine surfactants An industrial intermediate, not a cosmetic ingredient as supplied Dyestuffs Synthesis intermediate Dye intermediate manufacture Electroplating additive Non-cyanide bath additive Bath formulation is the customer's scope Fibre and leather treatment Treatment agent component Formulated into baths, not applied neat Neat casting in thick sections, food-contact claims, and any specification requiring a published amine value or gel time sit outside what this grade supports on paper. Figure 3. Amine-cured epoxy coating on the internal wall of a steel tank. 7. Limitations and Material Verification Two areas limit how DMAPA can be specified: the published data set itself, and the behaviour of the material in humid air or thick sections. 7.1 Known Limitations The specification covers appearance, color, purity and water only. No gel time, equivalent weight or official amine value is published, so any dosage plan stays theoretical until a batch COA confirms it. Blush is a property rather than a defect, and thick-section casting sits outside the grade because the exotherm of a neat amine in a large mass is hard to control. 7.2 Incoming Material Verification, Packaging and Safety Drum-to-drum variation exists on any amine line, so incoming checks on water content and color are recommended for every lot. Water content is determined by Karl Fischer titration and color is measured according to the APHA scale. DMAPA ships as a drum package with a published shelf life of at least 12 months in unopened packing at ambient temperature. Store in a well-ventilated area away from flames and direct sunlight, and close the cap tightly after each draw. The material is flammable, corrosive and a skin sensitiser; the hazard information is in the Material Safety Data Sheet. 8. Frequently Asked Questions How much DMAPA curing agent is needed per 100 parts of epoxy resin? Divide 5,110 by the resin EEW. The theoretical AHEW of 51.1 g/eq gives about 26.9 phr at EEW 190 and about 31.0 phr at EEW 165. Filler and temperature shift the ratio, so verify by gel time first. Why does the surface of a DMAPA-cured epoxy turn white or stay tacky? Two mechanisms produce that look. A white carbamate film is the amine reacting with CO2 in humid air; a tacky underlayer means under-stoichiometry from counting the tertiary nitrogen as an active hydrogen. Cure warmer and drier, and recalculate at 51.1 g/eq. Can DMAPA replace a modified amine hardener such as YLH-3101 in a floor coating? No, not as a one-for-one swap. YLH-3101 is a modified alicyclic hardener with a published AHEW of 110 g/eq, 55-60 phr loading and a 40-70 min gel time, and its modification exists to control blush. Neat DMAPA cures faster but blushes more. Does the tertiary amine in DMAPA count as an active hydrogen? It does not. The tertiary nitrogen has no N-H hydrogen, so it contributes catalysis but not stoichiometry, and the equivalent weight stays at 102.18 ÷ 2 = 51.1 g/eq. Counting three nitrogens returns 34.1 g/eq and roughly 18 phr, which under-cures the batch. How long can DMAPA be stored, and what does the packing look like? The published shelf life is at least 12 months in the original packing at ambient temperature, supplied as a drum package. No net drum weight is published, so confirm the packing list at order. Opened drums are closed tightly after each draw. Why does DMAPA darken or smoke when a drum is left open? The product page describes the material as flammable and corrosive, one that will smoke and blacken in air. Low-molecular-weight amines absorb water and CO2 quickly, and the reaction shows up as darkening. Keep the cap tight. 9. Conclusions This diamine (CAS 109-55-7) is fast, low-viscosity and water-miscible, and its theoretical AHEW of 51.1 g/eq gives about 27 phr against an EEW 190 resin. Its practical roles are an amidoamine building block, a reactivity booster and a small-dose accelerator. Its limits are humid-cure blush, exotherm in thick sections, and no published gel-time or amine-value data. Values quoted here are published data or figures labelled theoretical and literature; where the product page is silent, the current TDS / MSDS / COA governs. Grade availability for N,N-Dimethyl-1,3-propanediamine DMAPA is confirmed against a target EEW. 10. References • Yolatech product page, N,N-Dimethyl-1,3-propanediamine DMAPA: https://www.yolatech.com/nn-dimethyl-13-propanediamine-dmapa-cas-109-55-7 (accessed 2026-10-09). • Yolatech Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for DMAPA, CAS 109-55-7 (available on request). • ASTM D1652, epoxy content of epoxy resins (EEW). • ISO 3001, determination of epoxy equivalent. • ISO 9702, amine group nitrogen content of amine epoxide hardeners. • ASTM E203, water content by Karl Fischer titration. • ASTM D1544, Gardner color of transparent liquids.
    Read More
  • Trifunctional Epoxy Resin YLSE-0600: Cure and Dosage Guide
    Trifunctional Epoxy Resin YLSE-0600: Cure and Dosage Guide
    Oct 08, 2026
    Trifunctional epoxy resin YLSE-0600 is a glycidylamine epoxy resin carrying three epoxy groups per molecule at EEW 102-110 g/eq. The resin is a reddish brown liquid of 7000-20000 mPa·s at 25 °C. CAS 71604-74-5. Formulators pick it for high-temperature composites, laminating and structural adhesives. Product Code: YLSE-0600 CAS No.: 71604-74-5 Product Category: Multifunctional epoxy resin, glycidylamine type 1. What YLSE-0600 Is: A Trifunctional Epoxy Resin YLSE-0600 is the Yolatech grade code for a trifunctional epoxy resin built on a 3-glycidyloxy-N,N-diglycidylaniline backbone. CAS 71604-74-5. Two of the three oxirane rings hang on the aromatic nitrogen and the third sits on the phenoxy oxygen, so one molecule offers three amine-reactive sites. Molecular weight works out to 277.3 g/mol from C15H19NO4, which puts the theoretical epoxy equivalent weight at 92.4 g/eq. The product page lists a measured range of 102-110 g/eq. The gap is normal for a glycidylamine made via epichlorohydrin: residual oligomer and hydrolyzable chloride push EEW above theory. If a quote shows EEW below 100 for this CAS number, ask for the lot data behind it. Table 1 gathers the identity data in one place. Item Information Product code YLSE-0600 Chemical name 3-Glycidyloxy-N,N-diglycidylaniline CAS No. 71604-74-5 Epoxy functionality 3 groups per molecule Molecular weight 277.3 g/mol (calculated, C15H19NO4) Theoretical EEW 92.4 g/eq (277.3 / 3) Measured EEW 102-110 g/eq Appearance Reddish brown viscous liquid 2. Published Specifications of YLSE-0600 Five parameters are published for YLSE-0600. Together they define the handling envelope. Item Specification Appearance Reddish brown viscous liquid Color, Gardner Max. 11 Epoxy equivalent weight 102-110 g/eq Viscosity, 25 °C 7000-20000 mPa·s Volatiles Max. 1.0% Two of the five deserve comment. A Gardner color of max. 11 means cured parts will not be water-clear; expect reddish brown castings and films. The viscosity band is also wide, so batch-to-batch flow can drift if your process is tuned tightly. Confirm each lot against the TDS or COA before locking a pump setting or a preheat temperature. 3. Why Three Epoxy Groups Change the Cure Behavior Functionality is the whole story of this resin. DGEBA carries two oxirane rings per molecule; YLSE-0600 carries three, and the tertiary anilinic nitrogen left after glycidylation accelerates the neighboring epoxy-amine reactions. The practical result is a resin that gels faster and builds crosslink density sooner than a bisphenol A grade of comparable viscosity. The product page states the failure mode plainly: even moderate amounts, when cured with aliphatic amines, can develop enough exotherm to char the mass and evolve smoke. That is not boilerplate. A 500 g trial batch of a fast trifunctional epoxy can run away where a 2 kg batch of DGEBA would barely warm. Higher crosslink density usually buys higher glass transition temperature and better hot strength. Yolatech does not publish a Tg figure for YLSE-0600, so treat Tg as formulation-specific: it depends on the hardener, the cure schedule and the post-cure. Verify it on your own laminate before writing a datasheet claim. 4. YLSE-0600 Against Difunctional and Tetrafunctional Alternatives The comparison below uses only parameters published on the Yolatech product pages. Property YLSE-0600 (this resin) YLE-128 (bisphenol A) YLSE-721 (tetrafunctional) Epoxy groups per molecule 3 2 4 EEW, g/eq 102-110 184-190 105-120 Viscosity, mPa·s 7000-20000 at 25 °C 11000-15000 at 25 °C 3000-7000 at 50 °C Color Gardner max. 11, reddish brown not published Gardner max. 10, light yellow Volatiles / water max. 1.0% not published max. 0.6% Backbone aromatic glycidylamine bisphenol A ether aromatic glycidylamine Where does that leave a buyer? If you can heat the resin bath to 50 °C and want maximum crosslink density, YLSE-721 tetrafunctional epoxy resin is the stronger molecule. If you want the lowest hardener demand and the widest supply base, a standard liquid DGEBA is the cheaper answer. YLSE-0600 sits between the two: three epoxy groups per molecule, no heating demanded by the datasheet, and a color that rules out clear finishes. Against a standard liquid DGEBA such as liquid bisphenol A epoxy resin YLE-128, the trade is clearer still: YLSE-0600 asks for far more amine hardener by weight but returns a tighter network. For a phenolic backbone, PNE type phenolic epoxy resin YLEP-631 averages 2.7 epoxy groups per molecule; YLEP-638 semi-solid novolac epoxy resin is its higher-viscosity sibling, usually used in solution. 5. Hardener Dosage: Worked Examples The stoichiometry rule is short: phr = 100 × AHEW / EEW. AHEW values below come from the hardener product pages where published; where a page lists none, the value is theoretical or derived from the amine value. Table 4 covers six hardener families with the dose recalculated at both ends of the resin EEW band. Hardener AHEW, g/eq phr at EEW 102 phr at EEW 110 Source of AHEW Diethylenetriamine DETA 20.6 20.2 18.7 theoretical, 5 active H PACM diamine 52.5 51.5 47.7 theoretical, MW 210.4 / 4 MACM amine hardener 60 58.8 54.5 product page DETDA aromatic diamine approx. 44.6 43.7 40.5 derived from amine value 625-640 mg KOH/g Polyetheramine D-230 approx. 66.7 65.4 60.6 derived from amine value min. 7.5 mmol/g Polyamide hardener YLH-5101 160-200 157-196 145-182 product page For the same DETA on YLE-128 at EEW 184-190 g/eq, the dose drops to about 10.8-11.2 phr. YLSE-0600 therefore consumes roughly 75% more amine by weight per 100 parts resin. That is a real cost line, not a rounding error, and it belongs in your formulation economics next to the gain in crosslink density. Two cautions. These are stoichiometric starting points; in practice many aliphatic-amine systems run at 0.85-0.95 of the theoretical dose to control blush and exotherm. And check the arithmetic against your own certificate of analysis — if the COA says 107 g/eq, use 107, not the midpoint. 6. Cutting Viscosity Without Losing Functionality At 7000-20000 mPa·s, YLSE-0600 wets fiber well but will not self-level at room temperature. Reactive dilution is the standard fix, and the log rule gives a serviceable first estimate: blend viscosity falls roughly geometrically with diluent share. The diluent candidates below are published on the Yolatech site with their own viscosity and EEW. Diluent EEW, g/eq Viscosity, mPa·s Note for use with YLSE-0600 Butyl glycidyl ether YLD-9004A 147-157 max. 2 at 25 °C strongest thinning per part; monofunctional C8-10 alkyl glycidyl ether YLD-7004 220-250 3-10 at 25 °C gentler, needs more parts for the same drop Resorcinol diglycidyl ether YLD-6010 117-129 40-100 at 40 °C aromatic, keeps heat resistance Trimethylolpropane triglycidyl ether YLD-6012 135-145 100-200 at 25 °C trifunctional, preserves network density Pentaerythritol glycidyl ether YLD-6013 125-173 100-800 at 25 °C tetrafunctional character, wider EEW band Take 70 parts of YLSE-0600 at 15000 mPa·s with 30 parts of YLD-6012. The log blend lands near 3300-4100 mPa·s, workable for most impregnation equipment. Blend EEW rises to about 114 g/eq, so the DETA dose falls from 19.4 to 18.0 phr. Both numbers move; recompute both. Dilution is not free. Every part of monofunctional diluent removes reactive sites from the network, and hydrolyzable chloride from the diluent transfers into your system. For electronic work, check the diluent TDS for the chloride line first. 7. Processing Notes and Exotherm Control Batch size is your main exotherm control. • Pre-warm the resin to 40-50 °C before metering if your equipment allows it; as a rule of thumb, epoxy viscosity drops roughly by half for every 10-15 °C of heating. • Keep trial batches under 200 g until the gel behavior of your chosen hardener is known. • Aliphatic amines are the fast path and the fast failure; aromatic amines, MHHPA methyl hexahydrophthalic anhydride with an accelerator, or dicyandiamide systems trade speed for thermal margin. • Mix ratio errors show up as undercure in the core of a casting, not at the surface, so log actual weighed amounts rather than trusting pump settings. • Close the container tightly after drawing; the storage instruction matters more in a humid coastal workshop. When a casting chars or smokes, check batch size first, then hardener choice, then resin quality. In that order. 8. Applications of This Trifunctional Epoxy Resin The product page names six application fields for YLSE-0600: high temperature resistant composites, laminating, resin modification, adhesives, coatings and electronics. Each field below maps to the published data. Application Why this resin fits Numbers behind the judgment High-temperature composites three epoxy groups per molecule build a dense network EEW 102-110 g/eq; viscosity 7000-20000 mPa·s suits preheated impregnation Filament winding and laminating wets fiber after preheat Gardner max. 11 is acceptable on black carbon fiber parts Structural adhesives fast strength build-up with amine hardeners DETA dose approx. 19-20 phr at EEW 106 g/eq Resin modifier small additions raise crosslink density of DGEBA systems 10-30 phr as a modifier is the usual working band Coatings chemical resistance from the aromatic amine backbone plan on pigmentation; the resin itself is reddish brown Electronics used where heat resistance matters more than clarity volatiles max. 1.0% For clear or light-colored work, the honest answer is that Gardner max. 11 is a limitation. YLSE-186 alicyclic glycidyl ester epoxy stays at Gardner max. 2 with EEW 100-111 g/eq, at the price of a different cure profile. For a bisphenol F backbone with lower viscosity, bisphenol F epoxy resin YLE-170 runs 3500-4500 mPa·s but carries only two epoxy groups per molecule. 9. Frequently Asked Questions Can YLSE-0600 replace a bisphenol A resin one for one? No. Swapping YLE-128 for YLSE-0600 roughly doubles the amine dose, from about 11 phr to 19-20 phr of DETA, and gel time shortens. Pot life, exotherm and mix viscosity all move with it. If a plant meters both grades on the same pump, recalibrate the ratio before the first shot. How much amine hardener does YLSE-0600 need? phr = 100 × AHEW / EEW. At the EEW midpoint of 106 g/eq, that gives 19.4 phr for DETA (AHEW 20.6), 49.5 phr for PACM (AHEW 52.5) and 56.6 phr for MACM (AHEW 60). Use the EEW printed on your own COA, not the midpoint; the published band spans 102-110 g/eq. Why does YLSE-0600 cure faster than a bisphenol A epoxy? Three reasons stack up: a third epoxy group per molecule, a tertiary anilinic nitrogen that accelerates the adjacent epoxy-amine reaction, and a low EEW that packs more reactive sites into every 100 g. The downside is heat. Cured with aliphatic amines, even moderate batches can exotherm hard enough to char and smoke, so scale up slowly. Can I thin YLSE-0600 with a reactive diluent? Yes, and the log rule estimates the blend viscosity well enough for pump selection. Roughly 30 parts of YLD-6012 per 70 parts of YLSE-0600 brings 15000 mPa·s down to the 3300-4100 mPa·s range. Butyl glycidyl ether thins harder per part; C8-10 alkyl glycidyl ether needs more. Whatever you pick, recompute the hardener dose from the blend EEW. What is the shelf life and storage condition for YLSE-0600? Shelf life is normally 6 months from the date of manufacture in the original packing at suitable temperatures. Store in a well-ventilated area, keep the drum away from flames and direct sunlight, and close the cap tightly immediately after use. If a drum has sat through a hot summer, check viscosity against the COA before charging the tank. Is YLSE-0600 suitable for clear coatings? It is not. A Gardner color of up to 11 in a reddish brown liquid will read through any clear film. Use it where the part is pigmented, black or hidden inside a laminate. If clarity matters, YLSE-186 with its Gardner limit of 2 is the closer match. 10. Packaging, Storage and Safety YLSE-0600 ships in drum packages. Shelf life is normally 6 months from the date of manufacture in the original packing at suitable temperatures. Store in a well-ventilated area, away from flames and direct sunlight, and close the cap tightly immediately after use. Full safety and handling information is provided in the Material Safety Data Sheet. All parameters quoted here come from the YLSE-0600 product page and should be reconfirmed against the TDS, MSDS or COA of the lot you actually receive. Nothing in this article overrides those documents.
    Read More
1 2 3 4 5 6 7 8
A total of8pages

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit

home

products

WhatsApp

Contact Us