Home

Multifunctional epoxy resin

  • Liquid Phenolic Epoxy Resin YLEP-631: Seven Field Failures
    Liquid Phenolic Epoxy Resin YLEP-631: Seven Field Failures
    Oct 20, 2026
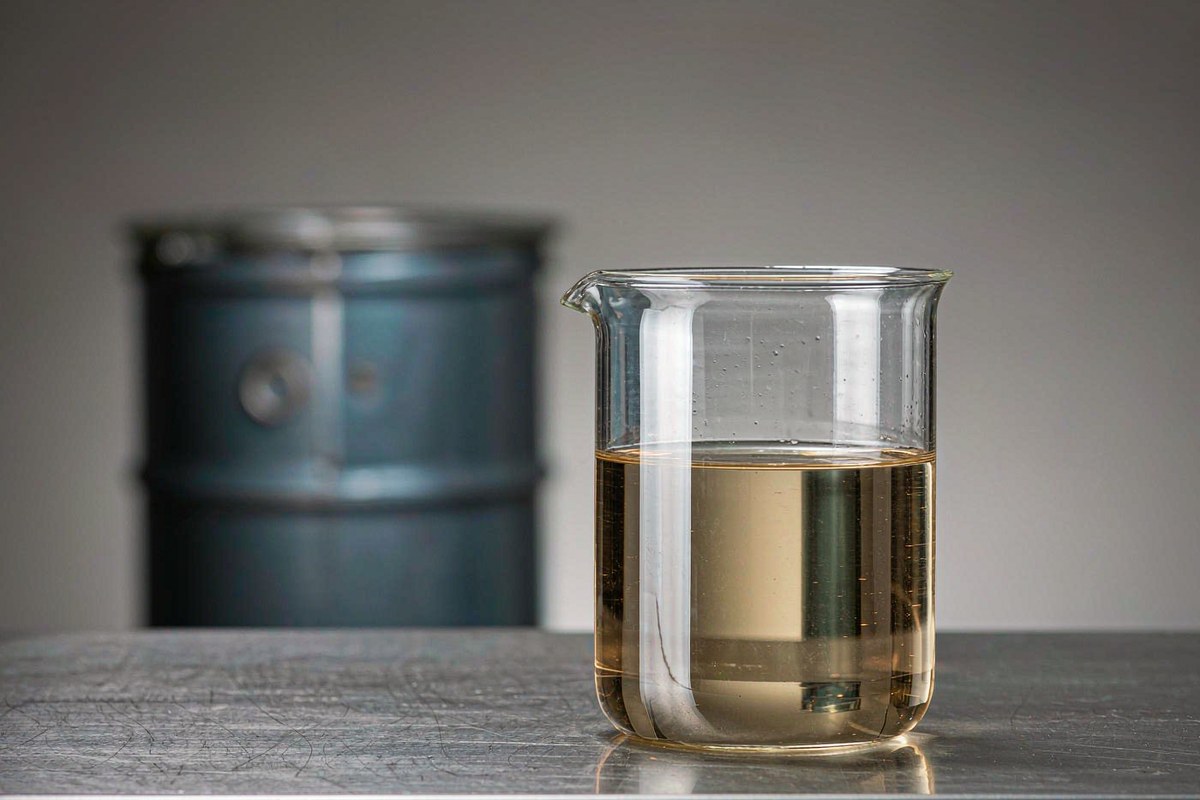
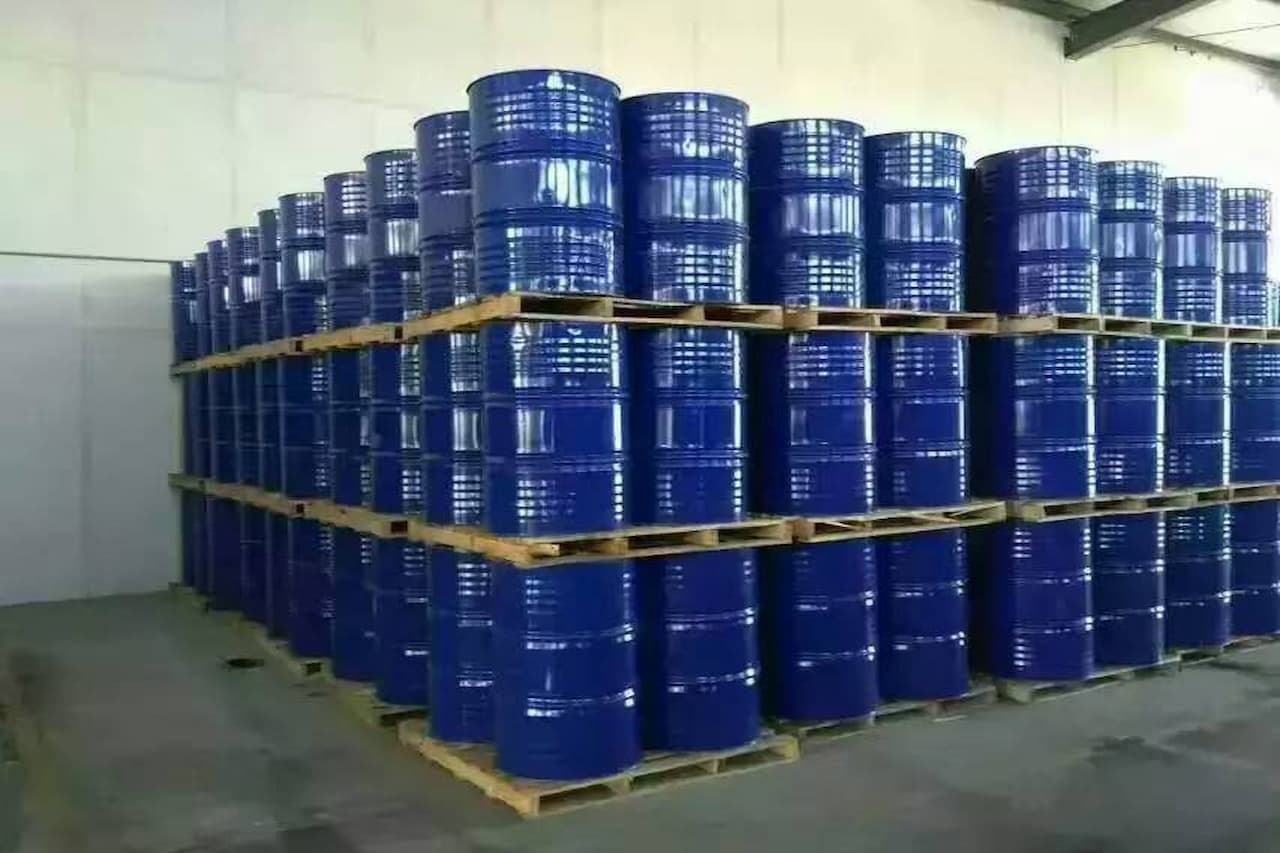
    Liquid phenolic epoxy resin YLEP-631 is a PNE-type novolac grade with 2.7 epoxy groups per molecule. Its published window is an EEW of 168-180 g/eq, a viscosity of 1100-1700 mPa·s at 52 °C and hydrolyzable chlorine below 500 ppm. Seven recurring failure patterns cover most field complaints about it. Figure 1. YLEP-631 pours warm and ships in steel drums; the color sits inside the Gardner limit of 3. 1. Introduction Heat service above 150 °C is the usual reason a formulator leaves a bisphenol A liquid for a novolac epoxy; the same move narrows the process window. YLEP-631 comes from a phenol-formaldehyde novolac glycidylated with epichlorohydrin; the oligomer mixture averages 2.7 epoxide rings per molecule against a fixed two for bisphenol A diglycidyl ether. Diagnosis first. Dosage second. 2. Materials and Methods: Identity and Test Basis for Liquid Phenolic Epoxy Resin YLEP-631 The product page publishes five specification items and a functionality statement; Table 1 sets identity beside them. 2.1 Product Identification and Published Specification Three gaps matter for procurement: no CAS number, density or flash point is published, so transport classification leans on the TDS and MSDS. Table 1. Identity and published specification of YLEP-631. Item Information CAS No. Not published; confirm on the current TDS / MSDS / COA Appearance Colorless to yellowish liquid Color, Gardner 3 maximum EEW, g/eq 168-180 Viscosity 1100-1700 mPa·s at 52 °C Hydrolyzable chlorine, ppm 500 maximum Epoxy functionality 2.7 groups per molecule (as published) Shelf life At least 12 months from manufacture in the original drum 2.2 Test Methods and Data Sources Values in Table 1 are reproduced as published, not re-measured; the lot COA overrides the catalogue window. Epoxy equivalent weight is determined by titration; ASTM D1652 and ISO 3001 describe the two routes in common use. Viscosity is quoted at 52 °C because the grade thickens sharply as it cools; a 25 °C reading is not comparable without a measured curve. Color follows ASTM D1544; hydrolyzable chlorine is a single ceiling, which suits buyers screening lots for ionic contamination. Incoming checks are usually performed in duplicate at two positions in the drum, with a third determination (n = 3) when the pair disagrees. 3. Results and Discussion: Where a 2.7-Functionality Resin Fails Two numbers set the operating window for YLEP-631: 2.7 epoxy groups per molecule and a viscosity specified at 52 °C. 3.1 Structure and the Reactivity Penalty Per kilogram, an EEW of 168-180 g/eq delivers 5.56-5.95 epoxy equivalents; a 184-190 g/eq bisphenol A liquid delivers 5.26-5.43. The gap is 5 to 10 percent. The novolac earns its price elsewhere: 2.7 reactive ends per molecule build network nodes faster than a difunctional resin can, lifting heat deflection and hot wet strength. The same 2.7 ends cause most field failures: more heat per unit mass during cure, less elongation, a shorter margin between workable viscosity and gel. Functionality buys heat resistance with process time. Moisture adds a second penalty: water picked up in a humid storeroom consumes epoxide and feeds the amine blush that spoils thin coatings; drums opened through a coastal summer gel early. 3.2 Field Failure Modes: Symptom, Root Cause, Countermeasure Seven patterns cover most failures reported for systems built on this grade, and each maps to a published number in Table 1. Table 2. Failure modes reported for liquid phenolic epoxy resin YLEP-631 systems. Observed symptom Likely root cause Countermeasure Viscosity creep or gel in a partly used drum Repeated opening in humid air; moisture starts headspace reaction Reseal at once, oldest stock first, re-check at 52 °C Runaway exotherm or char in thick castings 2.7 epoxides per molecule release more heat per unit mass Cast in layers, chill the mould, use a slower amine Cracks or brittle fracture after demoulding High crosslink density, low elongation Blend 20-30 phr of a difunctional liquid, ramp the cure Dry spots on fibre in laminates Bath cooled below the 52 °C reference Hold the bath at 55-60 °C and log it Ionic leakage or copper corrosion Chlorine ceiling is 500 ppm, not zero Screen lot COA; extraction-test the laminate Amine blush or oily film on coatings Moisture condensing on a cold substrate Keep substrate 3 °C above dew point, thin coats Batch color drift in clear parts Gardner 3 maximum allows a wide visual window Agree an internal limit tighter than 3 per lot Two are thermal, two are moisture or stoichiometry errors, the rest storage or specification gaps. Each costs more to fix than the resin. 3.3 Comparison with Alternative Systems Table 3 places YLEP-631 beside four alternatives, using published values only. Table 3. Property comparison of YLEP-631 with alternative epoxy systems (published values). Property YLEP-631 YLEP-638 YLE-128 (DGEBA) YLE-170 (BPF) YLSE-721 EEW, g/eq 168-180 170-190 184-190 160-180 110-125 Form at 25 °C Liquid Semi-solid Liquid Liquid Liquid Viscosity 1100-1700 mPa·s at 52 °C Not published; softening point 36-40 °C 11000-15000 mPa·s at 25 °C 2000-5000 mPa·s at 25 °C 6000-11000 mPa·s at 25 °C Epoxy groups per molecule 2.7 Above 2 2 2 4 YLE-128 bisphenol A epoxy resin stays the reference for room-temperature work: no heating, familiar dosage, two epoxides, a lower heat ceiling. The semi-solid sibling YLEP-638 novolac grade differs in one number: a 36-40 °C softening point instead of a pourable viscosity. YLE-170 bisphenol F resin runs at 2000-5000 mPa·s without warming and shares the 160-180 g/eq bracket but builds a less dense network. YLSE-721 tetrafunctional resin, a glycidylamine at 110-125 g/eq, is the harder-edged route: four epoxides, higher viscosity even at 25 °C, a Gardner allowance of 10. Color is a selection criterion, not a detail, for visible parts. 4. Formulation and Dosage Calculation Stoichiometric hardener demand follows one line, phr being parts per hundred of resin by weight. phr = 100 × AHEW ÷ EEW Table 4 works the equation across the published EEW window. Table 4. Stoichiometric hardener dosage for YLEP-631 across the published EEW window. Hardener Equivalent weight, g/eq phr at EEW 168 phr at EEW 174 phr at EEW 180 DETA (CAS 111-40-0), theoretical AHEW 20.6 12.3 11.8 11.4 MACM (CAS 6864-37-5), published AHEW 60 35.7 34.5 33.3 YLH-9101 (modified amine), published AHEW 92 54.8 52.9 51.1 MHHPA (CAS 25550-51-0), anhydride at ratio 0.85 143.0 85.1 82.2 79.4 Worked example: 2 kg at 174 g/eq takes 100 × 92 ÷ 174 = 52.9 phr of YLH-9101 modified amine, or 1058 g weighed separately. Blends move the target: seventy parts at 174 g/eq with thirty at 170 g/eq give a blend EEW of 172.8 g/eq, and a DETA demand of 11.9 phr. Treat every figure as a starting point: delivered EEW drifts inside its window, and a 10 g error is tolerable in 2 kg but is five percent in a 200 g lab mix. Post-cure belongs in the decision: heat resistance appears only after an elevated-temperature schedule; the current TDS governs the steps. 5. Processing Notes and Operating Window Warming the drum is the first operation, and where most batches go wrong. • Heat indirectly with a water bath or drum heater at 50-60 °C; open flame is out, per the product page. • A 200 L drum needs hours on the heater before the bulk reaches temperature. • Log viscosity at 52 °C against 1100-1700 mPa·s before charging the bath or the mixer. • Weigh resin and hardener by mass, never by volume, and degas 10-15 minutes under vacuum for sections above about 25 mm. • Ramp the cure: hold near 80 °C before climbing to 150-180 °C so the exotherm does not stack. Figure 2. A heater jacket warms the drum for decanting; indirect heat keeps the wall below the reaction point. 6. Applications Six routes appear on the product page, and each spends a different part of the specification. Electronic laminates use the dense network and the 500 ppm chlorine ceiling, watching ionic extraction on fine-line boards. Heat-resistant adhesives take hot strength from the tighter mesh but fail as brittle joints under impact. High-temperature coatings gain chemical resistance after post-cure and lose finish to amine blush on cold substrates. Composites wet out fibre at 1100-1700 mPa·s, but only while the bath holds 55-60 °C. Potting and casting risk exotherm cracking in thick sections; civil engineering grouts and epoxy vinyl inks take chemical resistance from the same network. None runs neat at room temperature; each starts from a warmed bath, a heated substrate or a blend. Figure 3. Wet lay-up shows the 52 °C viscosity first: fabric must be wet out while the bath holds temperature. 7. Limitations and Material Verification 7.1 Known Limitations and Unsuitable Cases This is not the resin for room-temperature hand lay-up, for impact-critical parts, or for flame retardance without additives. The molecule carries neither phosphorus nor bromine; a halogen-free flame-retardant laminate needs a co-resin such as YLDP-320 phenolic flame-retardant resin at 3.0% phosphorus. Viscosity exists only at 52 °C. If your process runs at 25 °C, ask for a measured curve instead of extrapolating. Clear parts need a color agreement tighter than Gardner 3; two compliant lots can look visibly different side by side. 7.2 Incoming Inspection, Packaging, Storage and Safety Incoming inspection should verify EEW by titration against the lot COA, plus color and hydrolyzable chlorine. Reject a lot outside 168-180 g/eq; every dosage moves with it. Storage is standard: well-ventilated, away from flames and direct sunlight, cap closed after use, oldest stock first. Shelf life is at least 12 months in the original drum. Safety information lives in the MSDS. Novolac epoxies are skin sensitisers; gloves and eye protection belong in the written procedure. 8. Frequently Asked Questions Why does a liquid grade need warming before use? YLEP-631 is liquid at 52 °C with 1100-1700 mPa·s, but the novolac backbone thickens sharply as temperature falls. Warming to 50-60 °C restores a workable viscosity. How is the hardener ratio calculated for a 168-180 g/eq novolac? phr = 100 × AHEW ÷ EEW. With MACM cycloaliphatic diamine at AHEW 60 g/eq, 100 g of resin at 174 g/eq takes 34.5 g of hardener. Use the lot COA value, not the catalogue midpoint. What causes cracking in thick YLEP-631 castings? Crosslink density: 2.7 epoxides per molecule build a rigid, low-elongation network, and a thick section adds thermal stress from its own exotherm. Cast in layers, ramp the cure, and consider 20-30 phr of a difunctional liquid. Is 500 ppm hydrolyzable chlorine low enough for electronic laminates? A ceiling, not a guarantee: a lot at 480 ppm passes specification yet may still run high for a fine-line board. Screen each lot COA and extraction-test the laminate when ionic cleanliness is critical. Can YLEP-631 be blended with a bisphenol A resin? Yes, and in practice it usually is. Blending cuts viscosity and cost while the novolac fraction keeps the heat resistance. Recalculate the blend EEW from 100 ÷ (sum of parts ÷ EEW of each) before fixing the hardener weight. Does YLEP-631 provide flame retardance? No. The molecule contains neither bromine nor phosphorus; flame retardance must come from a hardener, a co-resin or an additive, with any RoHS or UL 94 claim verified against current certificates. 9. Conclusions Liquid phenolic epoxy resin YLEP-631 is specified at 168-180 g/eq, 1100-1700 mPa·s at 52 °C, Gardner 3 maximum and 500 ppm hydrolyzable chlorine, with 2.7 epoxy groups per molecule. Its failure history is a history of that functionality: exotherm and brittleness in cure, viscosity and moisture in storage, ionic chlorine in electronics. Used warm, dosed from the lot COA and post-cured on schedule, the grade delivers the heat resistance it is priced for. 10. References 1. Product page, PNE type phenolic epoxy resin YLEP-631, Yolatech: https://www.yolatech.com/pne-type-phenolic-epoxy-resin-ylep-631 (accessed 2026-10-20). 2. Product page, PNE type phenolic epoxy resin YLEP-638, Yolatech: https://www.yolatech.com/pne-type-phenolic-epoxy-resin-ylep-638 (accessed 2026-10-20). 3. Product pages, bisphenol A epoxy resin YLE-127/YLE-128 and bisphenol F epoxy resin YLE-170, Yolatech: https://www.yolatech.com/bisphenol-a-epoxy-resin / https://www.yolatech.com/bisphenol-f-epoxy-resin 4. Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for YLEP-631, Yolatech (available on request). 5. ASTM D1652 (epoxy content, EEW) with ISO 3001 (epoxy equivalent), together with ASTM D1544 (Gardner color), ASTM D445 (kinematic viscosity) and ASTM E203 (Karl Fischer water).
    Read More
  • Phenolic Novolac Epoxy Resin: YLEP-638 Selection Guide
    Phenolic Novolac Epoxy Resin: YLEP-638 Selection Guide
    Oct 13, 2026
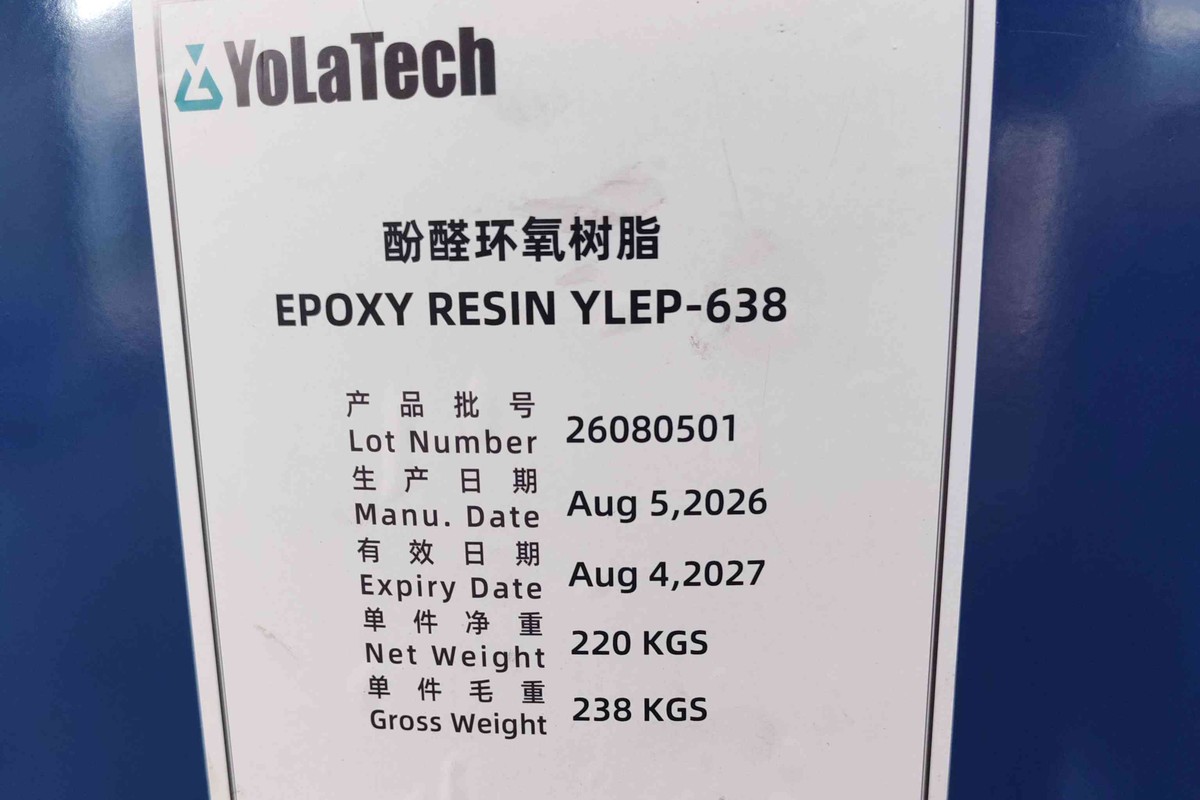
    Phenolic novolac epoxy resin YLEP-638 is a multifunctional epoxy resin from phenol-formaldehyde novolac and epichlorohydrin. Its published specification lists an epoxy equivalent weight of 170-190 g/eq, Gardner color 3.0 maximum, a softening point of 36-40 °C and hydrolyzable chlorine below 500 ppm. Figure 1. YLEP-638 phenolic novolac epoxy resin is supplied in steel drums and is a semi-solid at room temperature; the printed label carries the lot number, manufacturing date and expiry date. 1. Introduction Continuous service above roughly 150 °C is where a difunctional bisphenol A epoxy resin stops being the obvious answer. Phenolic novolac epoxy resin trades easy flow for a denser cured network. Built on a phenol-formaldehyde novolac core condensed with epichlorohydrin, YLEP-638 carries more than two epoxide rings per molecule on average. Published data on the sibling grade YLEP-631 records an average of 2.7 epoxy groups per molecule, against two for bisphenol A diglycidyl ether. Specification values below are quoted from the public Yolatech product pages, derived constants are marked calculated, and every dosage figure is a worked example rather than a recipe. Selection comes first. Dosage comes second. 2. Materials and Methods: Identification of Phenolic Novolac Epoxy Resin YLEP-638 The YLEP-638 product page publishes five specification items and a five-line application list. Table 1 sets identity data beside those published values. 2.1 Product Identification and Specification Table 1 collects identity data from the product page and flags the derived rows. Table 1. Identity and published specification of phenolic novolac epoxy resin YLEP-638. Item Information Product name PNE type phenolic epoxy resin YLEP-638 Chemical family Phenolic novolac (PNE) multifunctional epoxy resin CAS No. Not published; confirm on the current TDS / MSDS / COA Appearance Colorless to yellowish liquid (as published) Color, Gardner 3.0 maximum EEW, g/eq 170-190 Softening point (SP), °C 36-40 Hydrolyzable chlorine, ppm 500 maximum Epoxy functionality Above 2 (YLEP-631 published at 2.7) Packaging Drum Shelf life At least 12 months in original packing 2.2 Test Methods and Data Sources Values in Table 1 are quoted as published. No independent laboratory work was performed for this report. Epoxy equivalent weight is determined by titration, and the figure in the current TDS governs. ASTM D1652 and ISO 3001 describe the two common routes. Color is determined by ASTM D1544. Viscosity of the liquid comparator grades is measured at 25 °C; the YLEP-631 figure is quoted at 52 °C because that grade is not free-flowing at ambient. Hydrolyzable chlorine is given as one ceiling instead of a range, which matters where ionic chloride drives copper corrosion. Water content is normally found by Karl Fischer titration. Incoming checks on a novolac epoxy lot are usually run in duplicate, or as n = 3 determinations from separate positions in the same drum. 3. Results and Discussion: Structure, Reactivity and Grade Selection Two structural facts drive most selection decisions around YLEP-638: the novolac backbone and the 170-190 g/eq epoxy equivalent weight. 3.1 Structure and Reactivity of the Novolac Backbone Phenol and formaldehyde condense under acid catalysis into a novolac oligomer carrying several phenolic hydroxyls. Epoxidation with epichlorohydrin converts those hydroxyls into glycidyl ether groups, so one molecule can end in more than two epoxide rings. Higher functionality raises crosslink density after cure. Heat deflection temperature, chemical resistance and hot wet strength climb with it. Elongation falls. An epoxy equivalent weight of 170-190 g/eq sits close to the 184-190 g/eq of a standard liquid bisphenol A grade, so hardener demand per 100 g of resin stays in the same bracket. Functionality is the difference maker, not EEW. 3.2 Comparison with Alternative Systems Table 2 places YLEP-638 beside four published grades that buyers weigh against it. Table 2. Property comparison of YLEP-638 with alternative epoxy systems (published values). Property YLEP-638 YLEP-631 YLE-128 (DGEBA) YLE-170 (BPF) YLDP-320 EEW, g/eq 170-190 168-180 184-190 160-180 300-340 Form at ambient Semi-solid Liquid Liquid Liquid Solid Softening point, °C 36-40 Not published Not published Not published 70-85 Viscosity Not published 1100-1700 mPa·s at 52 °C 11000-15000 mPa·s at 25 °C 2000-5000 mPa·s at 25 °C Not published Epoxy groups per molecule Above 2 2.7 2 2 Not published Bisphenol F resin YLE-170, at 160-180 g/eq and 2000-5000 mPa·s, is the low-viscosity liquid option and wets fibre better than a novolac melt. Its cured heat resistance sits a little lower. YLEP-631 is the same chemistry at 168-180 g/eq with a published 1100-1700 mPa·s viscosity at 52 °C, so it pours where PNE type phenolic epoxy resin YLEP-638 will not flow unassisted. YLDP-320 answers a different question: 300-340 g/eq, 3.0% phosphorus, supplied as a solid for halogen-free flame-retardant laminates. Same backbone, different job. 4. Formulation and Dosage Calculation For an amine-cured system the stoichiometric hardener loading follows one equation, with phr read as parts per hundred parts of resin by weight. phr = 100 × AHEW ÷ EEW Anhydride curing uses the same logic with an anhydride equivalent weight, and the practical ratio usually falls between 0.85 and 1.00 of the theoretical figure. Table 3. Stoichiometric hardener dosage for phenolic novolac epoxy resin YLEP-638, calculated from the published EEW window. Hardener Equivalent weight, g/eq phr at EEW 170 phr at EEW 180 phr at EEW 190 DETA (CAS 111-40-0), theoretical AHEW 20.6 12.1 11.4 10.8 MACM (CAS 6864-37-5), published AHEW 60 35.3 33.3 31.6 MHHPA (CAS 25550-51-0), anhydride weight at ratio 0.90 151.2 88.9 84.0 79.6 A 500 g batch of YLEP-638 measuring 180 g/eq needs 100 × 60 ÷ 180 = 33.3 phr of MACM curing agent, or about 167 g weighed into the mix. Treat 33.3 phr as a starting point. Delivered epoxy equivalent weight moves inside the 170-190 g/eq window, and the amine content of a hardener lot rarely lands on the published figure. 5. Processing Notes and Operating Window YLEP-638 does not pour at room temperature. Warming the drum to 60-80 °C brings it to a workable viscosity, and blending with a liquid grade or a reactive diluent does the same at lower temperature. Pre-warm resin and hardener separately. Check the MHHPA anhydride or amine against its own viscosity or melting point before either enters the mix. Mix in one direction and keep the vortex shallow. Air whipped into a high-viscosity novolac blend is hard to remove afterwards. Degas under vacuum if the part is thick. A 10 to 15 minute step covers sections up to about 25 mm. Gel time shortens sharply as batch weight grows, because the exotherm of a novolac system concentrates in the mass. Check pot life at your own mix weight instead of trusting a table value. 6. Applications Five end uses appear on the YLEP-638 product page: coating, potting and casting, adhesive, laminates, and composites. Table 4. Application fit for phenolic novolac epoxy resin YLEP-638 and the grades commonly blended with it. Application Why YLEP-638 fits Companion grade Laminates Dense network, 500 ppm maximum hydrolyzable chlorine YLDP-320 for flame retardance Coatings Chemical and thermal resistance at high service temperature YLE-170 to cut viscosity Adhesives Hot wet strength under sustained load YLE-128 for flexibility Composites Mechanical strength at temperature after post-cure YLE-170 for fibre wet-out Potting and casting Rigid encapsulation of thermally stressed parts YLE-128 to ease flow YLEP-638 rarely runs alone. It is blended with a lower-viscosity resin to reach a processable viscosity, and the blend ratio decides the cured balance between heat resistance and toughness. 7. Limitations and Material Verification 7.1 Known Limitations and Unsuitable Cases Three published details deserve confirmation before YLEP-638 is written into a specification. The specification table labels its 36-40 °C row as viscosity in degrees Celsius, which describes a softening point rather than a viscosity. Confirm the property on the current TDS. Appearance is published as a colorless to yellowish liquid, while the product description calls the same resin semi-solid. Both cannot hold for one drum at 25 °C. No CAS number or epoxy functionality value is published for YLEP-638. Hand lay-up at ambient is not a suitable process for this grade. Neither is a flexible, impact-critical part: the dense network that buys heat resistance costs elongation. Pick YLEP-631 when flow governs the process, and YLEP-638 when heat and chemical resistance govern the part. 7.2 Incoming Inspection, Packaging, Storage and Safety Incoming inspection should confirm epoxy equivalent weight by titration against the lot COA, plus color and hydrolyzable chlorine. Reject a lot whose EEW sits outside 170-190 g/eq, because the dosage table shifts with it. Storage follows the standard epoxy routine: a well-ventilated area, away from flames and direct sunlight, with the cap closed tightly after each use. The product page states at least 12 months from manufacture in the original packing at ambient temperature, and drum is the published package. Safety information sits in the Material Safety Data Sheet. Novolac epoxy resins are skin sensitisers, so gloves and eye protection belong in the handling procedure. Any RoHS, REACH or UL 94 statement must be verified by the customer against current certificates. No certification is implied by a general product description. 8. Frequently Asked Questions What is the epoxy equivalent weight of phenolic novolac epoxy resin YLEP-638? The published range is 170-190 g/eq. Epoxy equivalent weight is determined by titration under the method stated in the current TDS, and ASTM D1652 covers the standard route. Use the lot COA figure for dosage work. How much hardener does YLEP-638 need per 100 g of resin? With MACM curing agent at a published AHEW of 60 g/eq, 100 g of YLEP-638 at 180 g/eq takes 33.3 g. The same 100 g with diethylenetriamine DETA at a theoretical 20.6 g/eq takes 11.4 g. Can YLEP-638 replace a liquid bisphenol A epoxy resin one for one? Not at ambient temperature. YLE-128 is a 11000-15000 mPa·s liquid, while YLEP-638 is a semi-solid with a 36-40 °C softening point, so warming or blending is required. Expect shorter gel time and a stiffer cured part. Why is YLEP-638 supplied as a semi-solid rather than a liquid? The novolac backbone raises functionality, and higher functionality raises viscosity at a given epoxy equivalent weight. That is the trade-off the grade accepts in return for a denser cured network. What is the difference between YLEP-638 and YLEP-631? Both are PNE-type phenolic novolac epoxy resins capped at 500 ppm hydrolyzable chlorine. YLEP-631 is published at 168-180 g/eq with a 1100-1700 mPa·s viscosity at 52 °C; YLEP-638 is published at 170-190 g/eq with a 36-40 °C softening point. Is YLEP-638 suitable for halogen-free electronic laminates? It can serve as the base resin, but it carries neither phosphorus nor bromine, so flame retardance has to come from the hardener, from a co-resin such as YLDP-320 at 3.0% phosphorus, or from an additive. Hydrolyzable chlorine at 500 ppm maximum is the ionic figure that matters. 9. Conclusions YLEP-638 is a PNE-type phenolic novolac epoxy resin published at 170-190 g/eq, 3.0 maximum Gardner color, a 36-40 °C softening point and 500 ppm maximum hydrolyzable chlorine. It ships in drums with a stated 12-month shelf life. Its value lies in crosslink density rather than in flow. Warm it or blend it, then dose by stoichiometry from the measured epoxy equivalent weight of the lot. Choose the lower-viscosity YLEP-631 phenolic novolac grade when flow governs the process, and YLEP-638 when heat and chemical resistance govern the part. 10. References 1. Product page, PNE type phenolic epoxy resin YLEP-638, Yolatech: https://www.yolatech.com/pne-type-phenolic-epoxy-resin-ylep-638 2. Product page, PNE type phenolic epoxy resin YLEP-631, Yolatech: https://www.yolatech.com/pne-type-phenolic-epoxy-resin-ylep-631 3. Product page, bisphenol A epoxy resin grades YLE-127 and YLE-128, Yolatech: https://www.yolatech.com/bisphenol-a-epoxy-resin 4. Product page, bisphenol F epoxy resin grade YLE-170, Yolatech: https://www.yolatech.com/bisphenol-f-epoxy-resin 5. Product page, DOPO-HQ modified phenolic epoxy resin YLDP-320, Yolatech: https://www.yolatech.com/dopo-hq-modified-phenolic-epoxy-resin-yldp-320 6. Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for PNE type phenolic epoxy resin YLEP-638, Yolatech (available on request). 7. ASTM D1652, epoxy content of epoxy resins (EEW); ISO 3001, determination of epoxy equivalent. 8. ASTM D1544, Gardner color of transparent liquids; ASTM D445, kinematic viscosity; ASTM E203, water content by Karl Fischer titration.
    Read More
  • High-Temperature-Resistant Trifunctional Liquid Epoxy Resin YLSE-0500 / YLSE-0510
    High-Temperature-Resistant Trifunctional Liquid Epoxy Resin YLSE-0500 / YLSE-0510
    Nov 21, 2025
    Product Description YLSE-0500 / YLSE-0510 is a high-temperature-resistant trifunctional epoxy resin based on p-aminophenol. The molecular structure contains multiple epoxy groups and aromatic rings, enabling the cured system to form a high crosslink density and aromatic density during curing. As a result, the cured material exhibits excellent heat resistance, high mechanical strength, low curing shrinkage, and good resistance to radiation, water, and chemicals. In addition, its low viscosity makes it easy to process and suitable for solvent-free operations. It is used in electrical insulation castings requiring high thermal resistance, as well as composite manufacturing processes such as carbon fiber and glass fiber filament winding, pultrusion, lamination, and prepreg production. The glass transition temperature (Tg) can exceed 200 °C.   Product Name 4-(2,3-Epoxypropoxy)-N,N-di(2,3-epoxypropyl)aniline CAS No.: 5026-74-4   Structural Formula   Technical Specifications   YLSE-0500 YLSE-0510 Appearance Brown liquid Yellow liquid EEW, g/eq 100-115 93-106 Viscosity, cps@25°C 1500-6000 500-1000 Volatiles, % Max. 1.5 Max.1.0   Main Applications High-temperature structural adhesives Carbon fiber and glass fiber composites for pultrusion and filament winding Electrical insulation materials High-temperature epoxy casting systems used in vacuum casting (RTM, VARTM) and Automatic Pressure Gelation (APG) Potting and sealing of miniature motor components High-temperature epoxy diluent   Properties of Neat Resin Castings Comparison of Casting Performance between YLSE-0500 and YLSE-0510 Using DDS (4,4'-diaminodiphenyl sulfone) as the curing agent, selected performance properties of castings made from YLSE-0500 and YLSE-0510 epoxy resins were tested. Casting preparation procedure: • Heat DDS to 200 °C (melting point 176 °C) until melted. • Preheat the epoxy resin to 100 °C. • Slowly add DDS into the epoxy resin while stirring until uniform. • Defoam under vacuum for 15 minutes. • Pour into molds and heat-cure.   The performance indicators of the resulting castings are shown in the table below: Brand type YLSE-0500 YLSE-0510 Curing agent name DDS Curing agent addition amount phr 49 Curing condition 0.5h/80°C+1h/100°C+1.5h/120°C+2h/180°C Tg(DMA method) °C 245-250 260-270 Bending performance at 25°C Strength Mpa 132 136 Modulus  Gpa 3.5 3.4 Tensile properties at 25°C Strength Mpa 64 70 Modulus  Gpa 3.8 3.6 Elongation at break  % 2.3 2.8   Casting Properties of YLSE-0500 with Methyl Tetrahydrophthalic Anhydride (MTHPA) YLSE-0500 epoxy resin is commonly used together with aromatic amine curing agents (such as diaminodiphenyl sulfone and diaminodiphenylmethane) and anhydride curing agents (such as methyl nadic anhydride, methyl tetrahydrophthalic anhydride, and methyl hexahydrophthalic anhydride).   The casting properties of YLSE-0500 cured with methyl tetrahydrophthalic anhydride (MTHPA) at 25 °C are shown in the table below: Tensile strength Mpa Bending strength Mpa Impact strength Kj/m2 Elongation at break  % Tg(DSC)  %  20-30 90-100 8-10 1.5-2.5 190-200 Mixing ratio(Phr): YLSE-0500/MTHPA=100/150 Curing conditions: 80℃/2h+100℃/2h+130℃/2h+180℃/3h   Precautions Due to its high functionality and high epoxy value, the curing process generates a large amount of heat, so attention must be paid to preventing runaway polymerization. If the viscosity becomes too high and causes difficulty in use, the resin may be heated to 100–120 °C for 1 hour to reduce the viscosity. During heating, please open the container lid to prevent any risk of runaway polymerization.   Equivalent Grades Similar domestic and international product grades include MY-0500, MY-0510, AFG-90, AFG-90H, etc.
    Read More
  • High-Temperature Resistant Tetrafunctional Liquid Epoxy Resin YLSE-721
    High-Temperature Resistant Tetrafunctional Liquid Epoxy Resin YLSE-721
    Nov 13, 2025
    Why is YLSE-721 our star product? What makes it so “hardcore”?   YLSE-721 is a high-performance, amino-based tetrafunctional liquid epoxy resin — an “industrial-grade bonding master” designed specifically for high-strength and high heat-resistant applications. Its name reveals the secret: “tetrafunctional” means each molecule contains four reactive sites, like a “multi-armed warrior” that can form a denser and stronger cross-linked network with curing agents. This is the key reason why its strength far exceeds that of ordinary difunctional epoxy resins. Meanwhile, its liquid form provides excellent flowability, making it ideal for potting, coating, or filling complex structures, ensuring easy and efficient application. What truly impresses users are its “three highs”: high temperature resistance, fast curing, and superior mechanical strength. Heat resistance: Continuous service temperature up to 150°C, and short-term endurance above 180°C, far outperforming standard epoxies (typically ≤120°C). Perfect for engine surroundings, motor coils, and PCB protection under high-temperature conditions. 🔧 Curing speed: Fully cures within 30–60 minutes at 60–80°C, which is 2–3 times faster than conventional epoxy systems — a real time-saver for urgent projects. Mechanical properties: Tensile strength exceeds 50 MPa, flexural strength surpasses 80 MPa, with excellent impact resistance and dimensional stability. It resists cracking even under severe vibration or thermal cycling. In addition, YLSE-721 offers outstanding electrical insulation, oil resistance, water resistance, and chemical durability — truly earning its reputation as the “Iron Man of the industrial world.”   Product Information Chemical Name: N,N,N',N'-Tetraglycidyl-4,4'-diaminodiphenylmethane CAS No.: 28768-32-3 Structural Formula     Main Applications High-temperature resistant composites such as carbon fiber and glass fiber; Potting of electronic components (e.g. power modules, LED drivers); Impregnation and insulation protection for motors and transformer coils; Precision mold manufacturing, including bonding of metals, ceramics, and composites; Bonding and sealing of aerospace structural components; Wear-resistant repair and anti-corrosion coatings for heavy-duty mechanical parts.   Usage Instructions YLSE-721 can be formulated with amine-type, anhydride-type, or imidazole-type curing agents and coupling agents to prepare adhesives, casting compounds, or composite systems for applications requiring excellent heat resistance. Common curing agents include 4,4'-diaminodiphenyl sulfone (4,4'-DDS), 4,4'-diaminodiphenylmethane (DDM), methyl tetrahydrophthalic anhydride (METHPA), methyl nadic anhydride (MNA), and 2-ethyl-4-methylimidazole (2,4EMI). If the resin appears too viscous during use, it can be heated to an appropriate temperature to reduce viscosity before mixing. To improve toughness, additives such as liquid polysulfide rubber or liquid nitrile rubber can be incorporated.   Typical Cured Properties DDS DDM METHPA MNA Test Method Glass Transition Temperature (°C) 250-260 220-230 200-210 235-240 Tensile Strength (MPa) 75 50 50 45 Tensile Modulus (GPa) 3.5 3.3 3.2 3.6 Flexural Strength (MPa) 130 120 100 97 Flexural Modulus (GPa) 3.3 3.4 4.0 3.8 Elongation at Break (%) 2.8 1.6 1.9 1.1 Impact Strength (kJ/m²) 15 10 9 8 Resin-to-Hardener Ratio (by weight) 100:52 100:42 100:42 100:150 Curing Schedule 100℃*2h+130℃*2h+160℃*2h+180℃*2h+200℃*2h   Common Mistakes to Avoid ❌ Incorrect curing agent combination: YLSE-721 must be used with specific anhydride or aromatic amine curing agents. Using general-purpose epoxy hardeners may result in incomplete curing, soft texture, or drastically reduced heat resistance ⚠️. ❌ Neglecting surface preparation: The substrate must be thoroughly cleaned, dried, and sanded; otherwise, adhesion failure or “false bonding” may occur. ❌ Overheating during curing: Although the resin has high thermal resistance, curing should be kept within the recommended temperature range (usually 60–120°C). Excessive temperature may cause bubbling or discoloration.   Precautions Due to its high functionality and epoxy value, YLSE-721 releases a large amount of heat during curing, so precautions should be taken to prevent runaway polymerization. If the viscosity is too high for convenient use, preheat the resin to 100–120°C for about one hour to lower viscosity. ⚠️ When heating, keep the container lid open to prevent polymerization explosion. This epoxy resin is alkali-resistant but not resistant to strong acids.
    Read More
  • YLEP-638 High-Performance Phenolic Epoxy Resin: Structure, Properties, and Applications
    YLEP-638 High-Performance Phenolic Epoxy Resin: Structure, Properties, and Applications
    Nov 06, 2025
    YLEP-638 Structural Characteristics The molecular backbone of YLEP-638 is a phenolic novolac structure formed by the condensation of phenol and formaldehyde, providing a rigid aromatic framework. This backbone itself has very high thermal stability and rigidity. On this phenolic framework, the hydroxyl groups react with epichlorohydrin to introduce multiple epoxy groups, making it a typical multifunctional epoxy resin. Unlike standard bisphenol-A type epoxy resins (such as E-51, functionality ≈ 2), YLEP-638 usually has an average epoxy functionality of 3.5 to 4.0 or even higher. Performance Features of YLEP-638 Outstanding Heat Resistance Origin: High crosslink density (resulting from high functionality) and rigid aromatic backbone. Performance: The cured product exhibits extremely high glass transition temperature (Tg) and heat distortion temperature (HDT), typically above 200°C and even up to 250°C. It maintains mechanical strength and dimensional stability under high temperatures with excellent creep resistance. Exceptional Mechanical Strength and Modulus Origin: Dense three-dimensional crosslinked network and rigid molecular chains. Performance: The cured product shows very high hardness, compressive strength, tensile strength, and modulus, giving it strong load-bearing capacity. Excellent Chemical Resistance Origin: The high crosslink density creates a compact and chemically inert network structure, making it difficult for solvents or chemical agents to penetrate or swell the material. Performance: It offers outstanding resistance to a wide range of organic solvents, acids, and alkalis. Its chemical resistance, particularly at high temperatures, is far superior to that of conventional epoxy resins. Superior Electrical Insulation Properties Origin: Stable chemical structure and high crosslink density. Performance: Maintains excellent dielectric strength and volume resistivity even under high temperature and humidity conditions. Processing Challenges High Viscosity: Due to its high functionality and rigid structure, YLEP-638 has very high viscosity at room temperature and must be heated (e.g., to 60–80°C) for casting, impregnation, or prepreg preparation. High Brittleness: The high crosslink density and rigid structure also result in low toughness, poor impact resistance, and low elongation at break, so it often requires the addition of toughening agents. Main Applications of YLEP-638 YLEP-638 + DOPO Used to produce halogen-free phosphorus-containing epoxy systems, successfully incorporating efficient phosphorus-based flame-retardant units into a high crosslink density epoxy network. The resulting materials combine excellent mechanical properties, heat resistance, and flame retardancy, making them ideal for green electronic encapsulation, halogen-free PCBs, high-performance flame-retardant insulating materials, and aerospace composites. Also used in carbon fiber prepregs, tennis rackets, and golf clubs.   YLEP-638 + Methacrylic Acid / Styrene Used to produce high-temperature- and corrosion-resistant phenolic epoxy vinyl ester resins, widely applied in flue gas desulfurization (FGD), power plant desulfurization tower linings, chemical storage tanks, and scrubbers for harsh environments.   YLE-128 + YLEP-638 + YLE-601 or YLE-604 Used for solder mask inks in copper-clad laminates and for anti-corrosion, high-temperature coatings (such as 900–1200°C heat-resistant and anti-oxidation coatings).   YLEP-638 + Curing Agent DDS Used to produce epoxy insulating varnishes for VPI (Vacuum Pressure Impregnation) processes, forming a strong, integrated “armor” layer on electrical coils. This layer resists high-voltage breakdown and withstands the intense heat and mechanical stress generated during motor operation. It is an essential insulation material for modern high-end electrical equipment, used in high-voltage motors, wind power generators, and traction motor stator coils, providing both insulation and flame-retardant protection. Also used in the manufacture of insulating tubes, rods, and plates.
    Read More
  • Introduction of Dicyandiamide Epoxy Curing Agent
    Introduction of Dicyandiamide Epoxy Curing Agent
    Apr 08, 2024
      Dicyandiamide curing agent belongs to the heating curing class of latent curing agent, solid at room temperature, insoluble in epoxy resin, dispersed in epoxy resin in the form of microparticles, through the heating reaction, once heated to the melting point of the vicinity of the start of the dissolution and rapid reaction curing.   Curing reaction of dicyandiamide The molecular structure of dicyandiamide contains a cyano group (-CN) in addition to four active hydrogens. Cyano group can also participate in the curing reaction as a functional group. The curing reaction temperature of dicyandiamide is generally in the range of 160~180°C, and the curing reaction time is 20~60 minutes. For bisphenol A epoxy resin with 190 epoxy equivalents, the theoretical dosage of dicyandiamide curing agent (calculated on the basis of active hydrogen equivalents) is 11.1 parts, but the actual dosage is often in the range of 4-10 parts (based on 100 parts of the resin by mass). Dicyandiamide micropowder is dispersed into the epoxy resin, has a suitable storage period, is stable in storage, does not delaminate, and does not cure.   The fineness of the dicyandiamide particles may vary from product to product. The finer the dicyandiamide particles, the more obvious the performance advantage for curing reaction Ultra-fine dicyandiamide particles are easier to be evenly dispersed into the epoxy resin liquid. Ultra-fine dicyandiamide particles can be better mixed and dissolved in the epoxy resin liquid than ordinary dicyandiamide.   Application areas of dicyandiamide curing compounds Dicyandiamide epoxy resin has good adhesive property, heat resistance and stable storage period. Dicyandiamide epoxy resins can be widely used in powder coatings, carbon fibre prepregs, heat curable inks, laminates, single component adhesives and other applications. Typical applications: Preparation of prepregs for the manufacture of reinforced composites (wind energy, automotive, aerospace, marine engineering and other industries). Electronic packaging materials, adhesives. Powder coatings (especially heavy duty anti-corrosion function). For epoxy-based adhesives (reinforced materials).   Nanjing Yolatech provides all kinds of high purity and low chlorine epoxy resins, including Bisphenol A epoxy resin, Bisphenol F epoxy resin, Phenolic epoxy resin, Brominated epoxy resin, DOPO modified phenolic epoxy resin, MDI modified epoxy resin, DCPD epoxy resin, Multifunctional epoxy resin, Crystalline epoxy resin, HBPA epoxy resin and so on. And we also could provide all kinds of curing agents or hardeners and diluents.   We will be at your service 24 hours a day. Pls contact us freely.    
    Read More
  • Properties of Epoxy Resin Adhesive
    Properties of Epoxy Resin Adhesive
    Apr 01, 2024
    Epoxy resin adhesive is a reprocessing or modification of epoxy resin to make its performance parameters meet specific requirements. Usually epoxy resin adhesives are also used with curing agents and need to be mixed well to be fully cured. Generally, the epoxy resin adhesive is called A adhesive or main agent, and the curing agent is called B adhesive or curing agent(hardener).   Main properties of epoxy resin adhesives before curing Colur, viscosity, specific gravity, proportioning, gel time, open time, curing time, thixotropy (flow stopping), hardness, surface tension, etc.   Main properties of epoxy resin adhesive after curing Resistivity, proof voltage, water absorption, compressive strength, tensile strength, shear strength, peel strength, impact strength, heat deflection temperature under load, glass transition temperature, internal stress, chemical resistance, elongation, shrinkage coefficient, thermal conductivity, electrical conductivity, weathering resistance, aging resistance, dielectric constant.   Curing characteristics of epoxy resin adhesive Most of the epoxy resin adhesives are heat-setting adhesives. The higher the temperature of the epoxy resin adhesive, the faster the curing. The more the amount mixed at one time, the faster the curing. The curing process has exothermic phenomenon, etc.   Nanjing Yolatech provides all kinds of high purity and low chlorine epoxy resins, including Bisphenol A epoxy resin, Bisphenol F epoxy resin, Phenolic epoxy resin, Brominated epoxy resin, DOPO modified phenolic epoxy resin, MDI modified epoxy resin, DCPD epoxy resin, Multifunctional epoxy resin, Crystalline epoxy resin, HBPA epoxy resin and so on. And we also could provide all kinds of curing agents or hardeners and diluents. We will be at your service 24 hours a day. Pls contact us freely.  
    Read More
  • Why does Epoxy Resin Crystallize
    Why does Epoxy Resin Crystallize
    Mar 28, 2024
    Background Under normal conditions, bisphenol A-type liquid epoxy resins are colorless, transparent and flowable. When the external temperature is lowered, the molecular chain is less active and prone to crystal seeding. Liquid epoxy resin appears grey in color, free-floating crystals, crystal clusters, or hard lumps like curing, we call it the crystallization phenomenon.   Reasons for the crystallization of epoxy resin The reasons for the crystallization of epoxy resin are complex, we mainly summarize the following. High purity. We all know that crystals are highly pure substances, and so is epoxy resin, the higher the purity, the narrower the molecular distribution, the easier it is to crystallize. Low viscosity. The lower the viscosity, the faster the crystallization. Impurities. solid impurities are usually crystalline species for crystal growth, and the addition of certain precipitating pigment fillers can easily lead to crystallization. In contrast, larger particle sizes and higher additions are less likely to induce crystallization. Temperature. A narrow temperature cycle of 20-30°C is a common cause of crystallization, with diurnal temperature fluctuations initiating or accelerating the rate of crystallization. In addition, ultra-low temperatures (below 5°C) will accelerate crystallization. Moisture. The higher the moisture content, the more likely crystallization will occur.   Does crystallization affect the properties of epoxy resins? The crystallization phenomenon does not affect the performance of the epoxy resin, only the epoxy resin morphology has changed, not deterioration. However, it brings a lot of inconvenience to the operation. After practice, the crystalline epoxy resin is dissolved by heating and mixed with the corresponding proportion of curing agent, its tensile strength, flexural strength, compressive strength, and bonding strength have no change in comparison with epoxy resin without crystallization. It can be seen that the crystallization phenomenon does not affect the performance of the epoxy resin, only the epoxy resin morphology has changed, not a qualitative change. In general, the crystallization of epoxy resin adhesive is a reversible process that can be changed with the temperature and has no effect on the bonding performance and reinforcing effect of epoxy resin cured products. Even if the crystallization occurs, heating until it softens and disappears, it can be used normally.   Nanjing Yolatech provides all kinds of high purity and low chlorine epoxy resins, including Bisphenol A epoxy resin, Bisphenol F epoxy resin, Phenolic epoxy resin, Brominated epoxy resin, DOPO modified phenolic epoxy resin, MDI modified epoxy resin, DCPD epoxy resin, Multifunctional epoxy resin, Crystalline epoxy resin, HBPA epoxy resin and so on. If you are interested in them, pls kindly contact us. We will be at service for you any time, thank you.  
    Read More

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit

home

products

WhatsApp

Contact Us