4,4'-DDS Dosage and Cure Schedule: The Numbers Behind Your Tg
Sep 28, 2026
Two decisions settle most of the outcome in a DDS-cured epoxy: how much hardener goes into the mix, and how the part is heated. Both are calculable before the first trial. In practice, both are often set by habit — a ratio copied from an old formulation sheet, or an oven profile carried over from a different hardener.
DDS dosage is not a number to copy. It is a number to calculate from equivalents, and then adjust on purpose.
4,4'-Diaminodiphenyl sulfone carries four active amine hydrogens on a molar mass of 248.30 g/mol. That gives an amine hydrogen equivalent weight (AHEW) of approximately 62.1 g/eq. Combined with the epoxy equivalent weight (EEW) of your resin, that single constant fixes the stoichiometric dosage. Everything after it — running above or below stoichiometry, adding an accelerator, extending the post-cure — is a deliberate adjustment with a measurable consequence.
From equivalents to grams
The calculation is the same one used for every amine hardener:
phr = (AHEW ÷ EEW) × 100
phr = parts of hardener per 100 parts of resin, by weight
For a standard liquid DGEBA at 185–190 g/eq — the workhorse laminating resin — this lands at about 33 phr. Published application data for 4,4'-DDS in DGEBA reports 33.4 phr, which is the same figure reached from the other direction.
Resin system
Typical EEW (g/eq)
Stoichiometric 4,4'-DDS
Note
Standard liquid DGEBA
185–190
≈33 phr
Matches the 33.4 phr reported in DGEBA/DDS application literature
DGEBA / DGEBF blend
170–180
35–37 phr
Lower EEW raises the hardener demand
Novolac-modified laminate resin
175–200
31–35 phr
Calculate on the blend, not on the base resin
TGMDA-based aerospace matrix
165–175 effective
35–38 phr
TGMDA alone is 111–125 g/eq; the blend is what counts
Aminophenol-type multifunctional epoxy
95–110
56–65 phr
High functionality means a high hardener demand
Stoichiometric values calculated from AHEW 62.1 g/eq. Always confirm against the EEW on the current resin lot certificate.
Figure 1. Stoichiometric 4,4'-DDS dosage as a function of epoxy equivalent weight, calculated from AHEW 62.1 g/eq. Original chart.
The case that trips people up: TGMDA
TGMDA — tetraglycidyl methylenedianiline, also written TGDDM and sold as MY-720 or MY-721 — has an EEW of roughly 111–125 g/eq. Read on its own, that suggests a DDS requirement near 50 phr. Aerospace prepreg matrices are not built that way, and the reason is worth understanding.
A widely cited high-performance matrix composition contains four epoxy components and two cure components. The epoxy blend totals 74.0 parts against 25.0 parts of 4,4'-DDS — about 34 phr. Worked back through equivalents, that is roughly 93% of stoichiometry for the blend.
Component
wt%
Role
TGMDA (TGDDM)
56.5
Tetrafunctional base resin; supplies the high crosslink density
Alicyclic diepoxy carboxylate
9.0
Viscosity and toughness modifier
Epoxy cresol novolac
8.5
Reactivity and heat resistance
4,4'-DDS
25.0
Hardener; ≈34 phr on 74.0 parts of epoxy
Boron trifluoride amine complex
1.1
Accelerator
Composition as reported for a standard high-performance epoxy matrix system. Percentages are literature values, not a YolaTech formulation.
The lesson is not the number 34. It is that DDS is dosed against the whole epoxy blend, not against the headline resin on the front of the drum.
Running off stoichiometry, on purpose
Most production formulations do not sit at a stoichiometric index of 100. A typical working band is 90–105. Moving within that band is a way of trading properties, and it is worth being explicit about the trade.
Running epoxy-rich — index below 100 — generally raises Tg and lowers moisture uptake, because the excess epoxy is consumed in secondary reactions rather than left as unreacted amine. The cost is toughness. Running amine-rich can improve toughness and adhesion, but any amine that stays unreacted acts as a plasticiser inside the network and pulls Tg down. Neither direction is universally correct; both are measurable.
The companion article on this blog looks at a published TGPAP/BPF study where eleven design runs varied blend composition and the amine-to-epoxy ratio. A longer processing window did not automatically produce a higher Tg, and the optimised case settled at 181.2 ± 0.8 °C with a stoichiometric ratio of 0.60. That is a useful reminder that DDS performance belongs to the complete formulation, not to the hardener name.
The cure schedule is a ramp, not a temperature
DDS is a latent hardener rather than a fast one. The sulfone bridge withdraws electron density from both amine nitrogens, so reaction onset sits well above room temperature. The practical consequence is useful: the hardener stays effectively inert while the resin is mixed, impregnated or cast, and heat is what starts the cure.
That latency is also why the cure schedule cannot be reduced to one number. Published schedules for DDS systems look like this.
System
DDS level
Cure schedule
DGEBA
30 phr
Isothermal at 180 °C
DGEBF
stoichiometric
Ramp from 35 °C to 180 °C at varied rates; hold 3 h at 180 °C
TGDDM with mixed DDS isomers
33 phr total
150 °C 2 h → 180 °C 1 h → 210 °C 2 h
TMBPBT epoxy
41 phr
Varied cure temperatures and times
Two-stage industrial practice
calculated
130 °C 2 h → 200 °C 2 h
Schedules as reported in DDS application literature and supplier application guidance.
Two patterns are worth noting. First, every schedule finishes high — between 180 and 210 °C — because that is where conversion and Tg are won. Second, the staged ramp exists for a physical reason rather than a traditional one. A thick section driven straight to the final temperature can concentrate the exotherm, which shows up as voids and internal stress. Staging lets the gel point arrive before the exotherm peak.
If the final temperature is a hard process limit, an accelerator is the standard route rather than a longer dwell at a lower temperature. BF3-monoethylamine appears at 1.1 phr in the matrix formulation above. Supplier guidance for DDS also describes adding roughly 0.5–1.2% of an acidic accelerator to bring the cure down to about 100 °C for one hour — but the DDS level has to be recalculated when a catalyst is carrying part of the reaction.
What Tg to expect
DSC data for DDS-cured epoxy is commonly reported in the 180–210 °C band, against roughly 150–170 °C for an aromatic amine such as m-phenylenediamine in a comparable system. Decomposition onset (Td5%) sits near 363 °C. Optimised matrices in the formulation literature report DDS systems above 250 °C.
Those are system-level values, not constants of the molecule. Resin choice, stoichiometric index, cure schedule and post-cure all move the result. A Tg quoted without the resin and the cure schedule behind it is not a specification; it is a claim.
Where the powder goes matters as much as how much
Dosage is only half the job. DDS melts at 175–181 °C, which is above the temperature at which most formulations are mixed. The hardener therefore enters the resin as a solid, and how that solid is distributed decides whether the cured part is uniform.
Three routes are in common use.
Powder dispersion. Fine DDS is dispersed in the liquid resin at 80–100 °C and dissolves progressively as the mix heats. The simplest route, and the most dependent on particle size distribution and mixing energy.
Solution. DDS is dissolved in hot solvent, or introduced as part of a solvent-borne varnish. The best uniformity, at the cost of a drying step and the solvent question that comes with it.
Melt blending. Short residence at 150–170 °C. Fast and uniform, but it consumes the processing time that DDS latency would otherwise give you.
The failure mode to watch for is agglomeration. Clusters of undissolved DDS create hardener-rich and hardener-poor zones at the same time. The hardener-poor zones stay under-cured, and the symptom is deceptive: the part passes a room-temperature test, then shows a low Tg, or a soft core in a thick section, or a scatter of results that cannot be reproduced. Optical microscopy on a cured cross-section is the cheapest way to catch it before it reaches a customer.
Reading an unexpected result
When a DDS formulation does not behave, the symptom usually points at one of six causes.
What you observe
Most likely cause
What to check first
Tg below the design target
Incomplete conversion
Residual exotherm by DSC; extend or raise the post-cure
Soft or tacky core in a thick section
Agglomerated hardener
Cross-section under optical microscopy; particle size distribution
Voids or cracking during cure
Exotherm concentrated by a direct ramp
Ramp rate, section thickness, filler level
Powder has turned pink or red
Surface oxidation in storage
Melting point and assay. A slight tint is cosmetic; deep red or caking is not
Same formula, different result between lots
Dosage copied instead of calculated
EEW on the current resin lot certificate; the phr actually weighed
One-part mix gels in storage
Accelerator level or storage temperature
Storage temperature; accelerator loading; dispersion method
Keep a process log, not just a result
What makes a DDS trial reusable is the record behind it. A minimum log for one trial:
• Resin identity, current-lot EEW, and the phr actually weighed out
• Mixing route, mixing temperature, and how long the DDS was in the resin before use
• Processing window observed, and the method used to judge it
• Cure and post-cure as actually run, not as planned
• Tg by DSC or DMA, with the heating rate stated
• The ageing test that matters for the application — heat, moisture, chemical or thermal cycling
A trial without that log produces a result nobody can repeat, including the person who ran it.
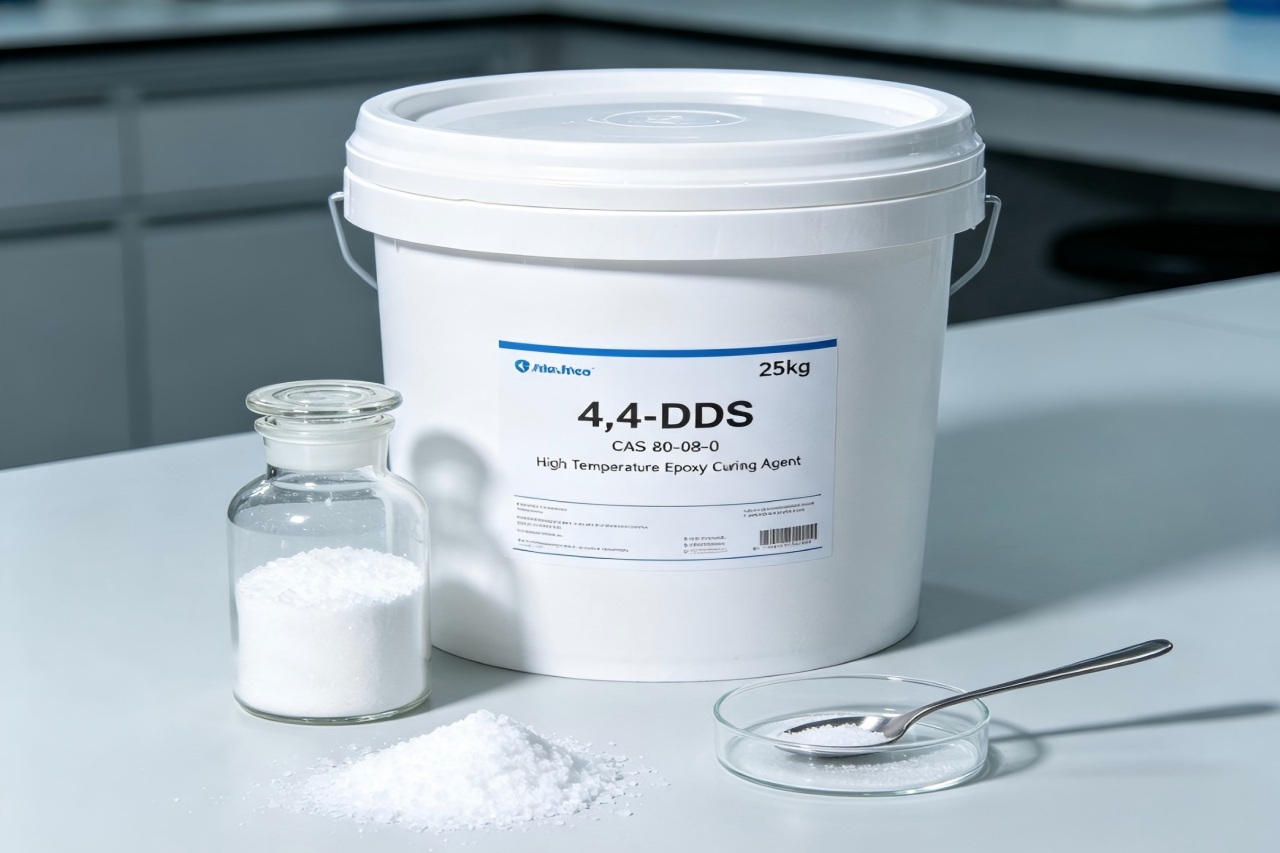
YolaTech 4,4'-DDS at a glance
Property
TDS value
Appearance
White crystal powder
Purity
≥99.0%
Melting point
175–181 °C
Loss on drying
≤0.30%
CAS number
80-08-0
Theoretical AHEW
≈62.1 g/eq, calculated
Primary industrial use
High-temperature epoxy curing agent
Additional TDS use
Material for polysulfone amide and other polymers
Storage
Cool, dry place; avoid direct sunlight
Storage life
12 months in the original sealed container at ambient temperature
Packaging
25 kg fiber drum
The formulation is the answer, not the molecule
4,4'-DDS sets a high ceiling. The molecule supplies the rigid aromatic network that makes 180–210 °C service possible. How much of that ceiling a part actually reaches is decided by four things that are all under the formulator's control: the dosage calculated from equivalents, the uniformity of the dispersion, the shape of the cure ramp, and whether a post-cure was run to completion.
If the question is what the molecule does, the companion article on this blog covers the mechanism and the application map. If the question is what to weigh and how to heat it, this is the part that decides the outcome.
Send us the resin type, the EEW on the current lot, the process temperature limit and the section thickness. We will work the dosage and the cure schedule through with you — and tell you when DDS is not the right hardener for the job.
Read More




 IPv6 network supported