

Language :

Language :
Liquid phenolic epoxy resin YLEP-631 is a PNE-type novolac grade with 2.7 epoxy groups per molecule. Its published window is an EEW of 168-180 g/eq, a viscosity of 1100-1700 mPa·s at 52 °C and hydrolyzable chlorine below 500 ppm. Seven recurring failure patterns cover most field complaints about it.
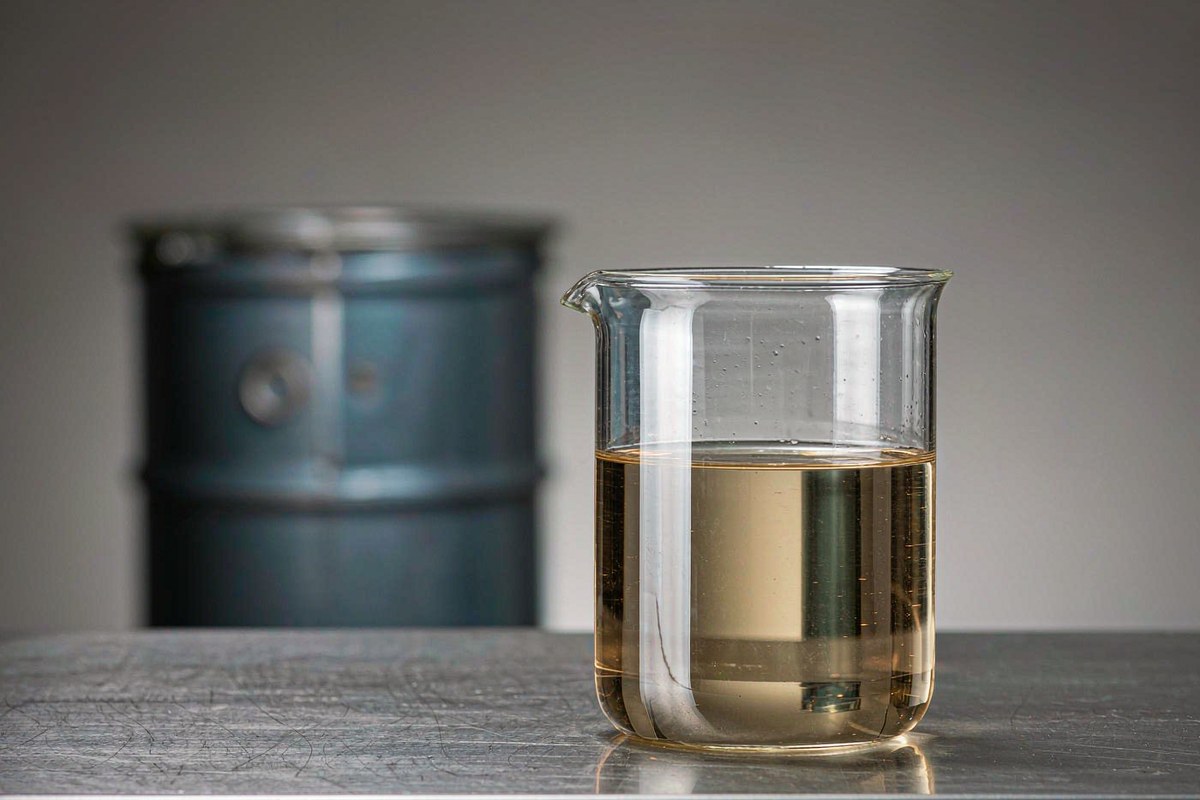
Figure 1. YLEP-631 pours warm and ships in steel drums; the color sits inside the Gardner limit of 3.
Heat service above 150 °C is the usual reason a formulator leaves a bisphenol A liquid for a novolac epoxy; the same move narrows the process window.
YLEP-631 comes from a phenol-formaldehyde novolac glycidylated with epichlorohydrin; the oligomer mixture averages 2.7 epoxide rings per molecule against a fixed two for bisphenol A diglycidyl ether.
Diagnosis first. Dosage second.
The product page publishes five specification items and a functionality statement; Table 1 sets identity beside them.
Three gaps matter for procurement: no CAS number, density or flash point is published, so transport classification leans on the TDS and MSDS.
Table 1. Identity and published specification of YLEP-631.
Item |
Information |
CAS No. |
Not published; confirm on the current TDS / MSDS / COA |
Appearance |
Colorless to yellowish liquid |
Color, Gardner |
3 maximum |
EEW, g/eq |
168-180 |
Viscosity |
1100-1700 mPa·s at 52 °C |
Hydrolyzable chlorine, ppm |
500 maximum |
Epoxy functionality |
2.7 groups per molecule (as published) |
Shelf life |
At least 12 months from manufacture in the original drum |
Values in Table 1 are reproduced as published, not re-measured; the lot COA overrides the catalogue window.
Epoxy equivalent weight is determined by titration; ASTM D1652 and ISO 3001 describe the two routes in common use.
Viscosity is quoted at 52 °C because the grade thickens sharply as it cools; a 25 °C reading is not comparable without a measured curve.
Color follows ASTM D1544; hydrolyzable chlorine is a single ceiling, which suits buyers screening lots for ionic contamination.
Incoming checks are usually performed in duplicate at two positions in the drum, with a third determination (n = 3) when the pair disagrees.
Two numbers set the operating window for YLEP-631: 2.7 epoxy groups per molecule and a viscosity specified at 52 °C.
Per kilogram, an EEW of 168-180 g/eq delivers 5.56-5.95 epoxy equivalents; a 184-190 g/eq bisphenol A liquid delivers 5.26-5.43. The gap is 5 to 10 percent.
The novolac earns its price elsewhere: 2.7 reactive ends per molecule build network nodes faster than a difunctional resin can, lifting heat deflection and hot wet strength.
The same 2.7 ends cause most field failures: more heat per unit mass during cure, less elongation, a shorter margin between workable viscosity and gel.
Functionality buys heat resistance with process time.
Moisture adds a second penalty: water picked up in a humid storeroom consumes epoxide and feeds the amine blush that spoils thin coatings; drums opened through a coastal summer gel early.
Seven patterns cover most failures reported for systems built on this grade, and each maps to a published number in Table 1.
Table 2. Failure modes reported for liquid phenolic epoxy resin YLEP-631 systems.
Observed symptom |
Likely root cause |
Countermeasure |
Viscosity creep or gel in a partly used drum |
Repeated opening in humid air; moisture starts headspace reaction |
Reseal at once, oldest stock first, re-check at 52 °C |
Runaway exotherm or char in thick castings |
2.7 epoxides per molecule release more heat per unit mass |
Cast in layers, chill the mould, use a slower amine |
Cracks or brittle fracture after demoulding |
High crosslink density, low elongation |
Blend 20-30 phr of a difunctional liquid, ramp the cure |
Dry spots on fibre in laminates |
Bath cooled below the 52 °C reference |
Hold the bath at 55-60 °C and log it |
Ionic leakage or copper corrosion |
Chlorine ceiling is 500 ppm, not zero |
Screen lot COA; extraction-test the laminate |
Amine blush or oily film on coatings |
Moisture condensing on a cold substrate |
Keep substrate 3 °C above dew point, thin coats |
Batch color drift in clear parts |
Gardner 3 maximum allows a wide visual window |
Agree an internal limit tighter than 3 per lot |
Two are thermal, two are moisture or stoichiometry errors, the rest storage or specification gaps. Each costs more to fix than the resin.
Table 3 places YLEP-631 beside four alternatives, using published values only.
Table 3. Property comparison of YLEP-631 with alternative epoxy systems (published values).
Property |
YLEP-631 |
YLEP-638 |
YLE-128 (DGEBA) |
YLE-170 (BPF) |
YLSE-721 |
EEW, g/eq |
168-180 |
170-190 |
184-190 |
160-180 |
110-125 |
Form at 25 °C |
Liquid |
Semi-solid |
Liquid |
Liquid |
Liquid |
Viscosity |
1100-1700 mPa·s at 52 °C |
Not published; softening point 36-40 °C |
11000-15000 mPa·s at 25 °C |
2000-5000 mPa·s at 25 °C |
6000-11000 mPa·s at 25 °C |
Epoxy groups per molecule |
2.7 |
Above 2 |
2 |
2 |
4 |
YLE-128 bisphenol A epoxy resin stays the reference for room-temperature work: no heating, familiar dosage, two epoxides, a lower heat ceiling.
The semi-solid sibling YLEP-638 novolac grade differs in one number: a 36-40 °C softening point instead of a pourable viscosity.
YLE-170 bisphenol F resin runs at 2000-5000 mPa·s without warming and shares the 160-180 g/eq bracket but builds a less dense network.
YLSE-721 tetrafunctional resin, a glycidylamine at 110-125 g/eq, is the harder-edged route: four epoxides, higher viscosity even at 25 °C, a Gardner allowance of 10.
Color is a selection criterion, not a detail, for visible parts.
Stoichiometric hardener demand follows one line, phr being parts per hundred of resin by weight.
phr = 100 × AHEW ÷ EEW
Table 4 works the equation across the published EEW window.
Table 4. Stoichiometric hardener dosage for YLEP-631 across the published EEW window.
Hardener |
Equivalent weight, g/eq |
phr at EEW 168 |
phr at EEW 174 |
phr at EEW 180 |
DETA (CAS 111-40-0), theoretical AHEW |
20.6 |
12.3 |
11.8 |
11.4 |
MACM (CAS 6864-37-5), published AHEW |
60 |
35.7 |
34.5 |
33.3 |
YLH-9101 (modified amine), published AHEW |
92 |
54.8 |
52.9 |
51.1 |
MHHPA (CAS 25550-51-0), anhydride at ratio 0.85 |
143.0 |
85.1 |
82.2 |
79.4 |
Worked example: 2 kg at 174 g/eq takes 100 × 92 ÷ 174 = 52.9 phr of YLH-9101 modified amine, or 1058 g weighed separately.
Blends move the target: seventy parts at 174 g/eq with thirty at 170 g/eq give a blend EEW of 172.8 g/eq, and a DETA demand of 11.9 phr.
Treat every figure as a starting point: delivered EEW drifts inside its window, and a 10 g error is tolerable in 2 kg but is five percent in a 200 g lab mix.
Post-cure belongs in the decision: heat resistance appears only after an elevated-temperature schedule; the current TDS governs the steps.
Warming the drum is the first operation, and where most batches go wrong.
• Heat indirectly with a water bath or drum heater at 50-60 °C; open flame is out, per the product page.
• A 200 L drum needs hours on the heater before the bulk reaches temperature.
• Log viscosity at 52 °C against 1100-1700 mPa·s before charging the bath or the mixer.
• Weigh resin and hardener by mass, never by volume, and degas 10-15 minutes under vacuum for sections above about 25 mm.
• Ramp the cure: hold near 80 °C before climbing to 150-180 °C so the exotherm does not stack.
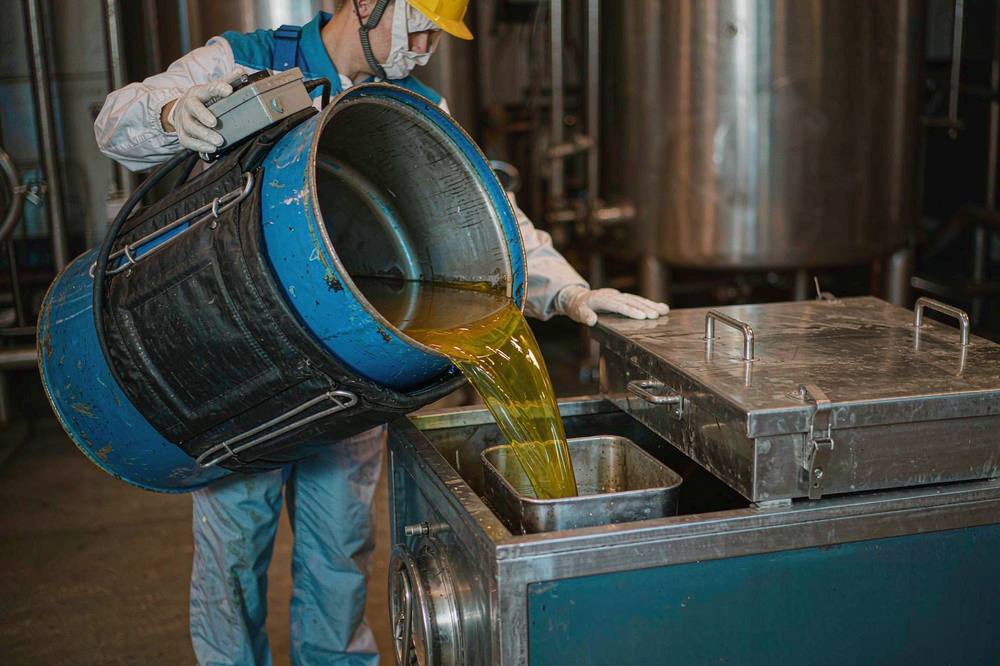
Figure 2. A heater jacket warms the drum for decanting; indirect heat keeps the wall below the reaction point.
Six routes appear on the product page, and each spends a different part of the specification.
Electronic laminates use the dense network and the 500 ppm chlorine ceiling, watching ionic extraction on fine-line boards. Heat-resistant adhesives take hot strength from the tighter mesh but fail as brittle joints under impact. High-temperature coatings gain chemical resistance after post-cure and lose finish to amine blush on cold substrates.
Composites wet out fibre at 1100-1700 mPa·s, but only while the bath holds 55-60 °C. Potting and casting risk exotherm cracking in thick sections; civil engineering grouts and epoxy vinyl inks take chemical resistance from the same network.
None runs neat at room temperature; each starts from a warmed bath, a heated substrate or a blend.
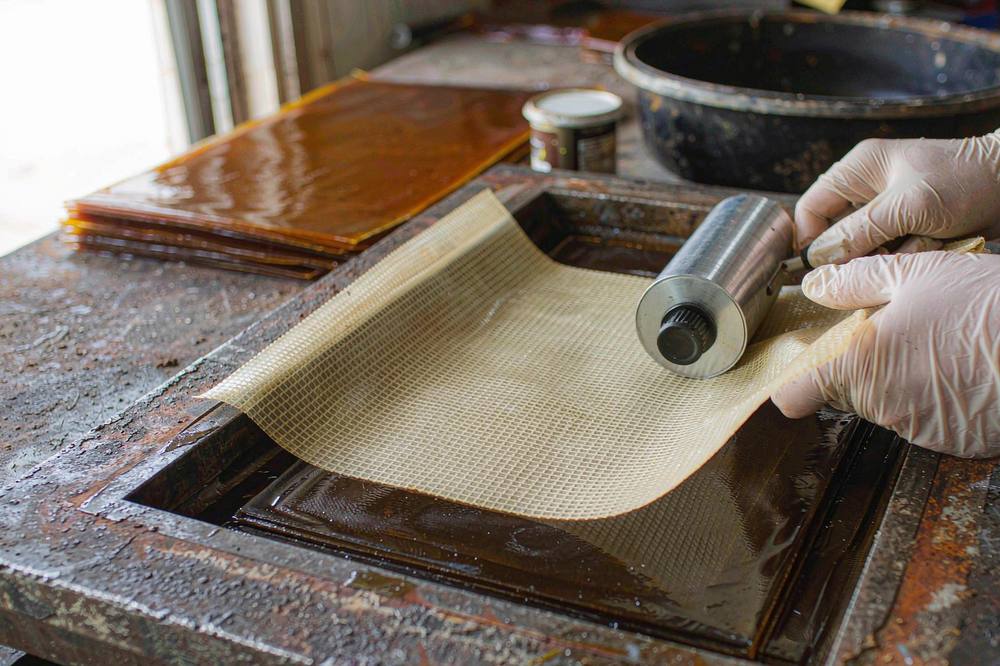
Figure 3. Wet lay-up shows the 52 °C viscosity first: fabric must be wet out while the bath holds temperature.
This is not the resin for room-temperature hand lay-up, for impact-critical parts, or for flame retardance without additives. The molecule carries neither phosphorus nor bromine; a halogen-free flame-retardant laminate needs a co-resin such as YLDP-320 phenolic flame-retardant resin at 3.0% phosphorus.
Viscosity exists only at 52 °C. If your process runs at 25 °C, ask for a measured curve instead of extrapolating.
Clear parts need a color agreement tighter than Gardner 3; two compliant lots can look visibly different side by side.
Incoming inspection should verify EEW by titration against the lot COA, plus color and hydrolyzable chlorine. Reject a lot outside 168-180 g/eq; every dosage moves with it.
Storage is standard: well-ventilated, away from flames and direct sunlight, cap closed after use, oldest stock first. Shelf life is at least 12 months in the original drum.
Safety information lives in the MSDS. Novolac epoxies are skin sensitisers; gloves and eye protection belong in the written procedure.
YLEP-631 is liquid at 52 °C with 1100-1700 mPa·s, but the novolac backbone thickens sharply as temperature falls. Warming to 50-60 °C restores a workable viscosity.
phr = 100 × AHEW ÷ EEW. With MACM cycloaliphatic diamine at AHEW 60 g/eq, 100 g of resin at 174 g/eq takes 34.5 g of hardener. Use the lot COA value, not the catalogue midpoint.
Crosslink density: 2.7 epoxides per molecule build a rigid, low-elongation network, and a thick section adds thermal stress from its own exotherm. Cast in layers, ramp the cure, and consider 20-30 phr of a difunctional liquid.
A ceiling, not a guarantee: a lot at 480 ppm passes specification yet may still run high for a fine-line board. Screen each lot COA and extraction-test the laminate when ionic cleanliness is critical.
Yes, and in practice it usually is. Blending cuts viscosity and cost while the novolac fraction keeps the heat resistance. Recalculate the blend EEW from 100 ÷ (sum of parts ÷ EEW of each) before fixing the hardener weight.
No. The molecule contains neither bromine nor phosphorus; flame retardance must come from a hardener, a co-resin or an additive, with any RoHS or UL 94 claim verified against current certificates.
Liquid phenolic epoxy resin YLEP-631 is specified at 168-180 g/eq, 1100-1700 mPa·s at 52 °C, Gardner 3 maximum and 500 ppm hydrolyzable chlorine, with 2.7 epoxy groups per molecule.
Its failure history is a history of that functionality: exotherm and brittleness in cure, viscosity and moisture in storage, ionic chlorine in electronics.
Used warm, dosed from the lot COA and post-cured on schedule, the grade delivers the heat resistance it is priced for.
1. Product page, PNE type phenolic epoxy resin YLEP-631, Yolatech: https://www.yolatech.com/pne-type-phenolic-epoxy-resin-ylep-631 (accessed 2026-10-20).
2. Product page, PNE type phenolic epoxy resin YLEP-638, Yolatech: https://www.yolatech.com/pne-type-phenolic-epoxy-resin-ylep-638 (accessed 2026-10-20).
3. Product pages, bisphenol A epoxy resin YLE-127/YLE-128 and bisphenol F epoxy resin YLE-170, Yolatech: https://www.yolatech.com/bisphenol-a-epoxy-resin / https://www.yolatech.com/bisphenol-f-epoxy-resin
4. Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for YLEP-631, Yolatech (available on request).
5. ASTM D1652 (epoxy content, EEW) with ISO 3001 (epoxy equivalent), together with ASTM D1544 (Gardner color), ASTM D445 (kinematic viscosity) and ASTM E203 (Karl Fischer water).
 IPv6 network supported